

Top-Lid Household Plastic Trash Bin Injection Mould: Durable, Efficient Tooling for Modern Waste Containers
Admin 2026-10-20Household waste bins may appear simple, but producing a large, durable, attractive, and accurately dimensioned plastic trash bin requires carefully engineered injection moulding tooling. The Top-Lid Household Plastic Trash Bin Injection Mould is developed for manufacturers that need dependable production of practical waste containers for homes, offices, bathrooms, public areas, and other everyday environments. Its design combines a reinforced bin body, an integrated top-lid structure, optimized material flow, and cooling arrangements suited to relatively large plastic products.
This injection mould is intended for the production of household trash bins, office waste containers, and bathroom garbage bins made from commonly used polypropylene or high-density polyethylene. With a hot runner system, one-cavity configuration, P20 or 718 mould steel, and a stated service life of up to 600,000 shots, the tooling is positioned as a long-term production asset rather than a short-term prototype solution.
For manufacturers, the value of a trash bin mould is measured by more than its ability to form a basic container. The mould must support stable cycle operation, consistent wall formation, attractive visible surfaces, reliable lid alignment, efficient maintenance, and repeatable product dimensions. It must also help control common defects such as sink marks, warpage, short shots, weld lines, flash, and uneven cooling. The Top-Lid Household Plastic Trash Bin Injection Mould addresses these requirements through a combination of structural reinforcement, gate optimization, cooling design, suitable material selection, and professional manufacturing management.

Top-Lid Household Plastic Trash Bin Injection Mould
1. Product Overview
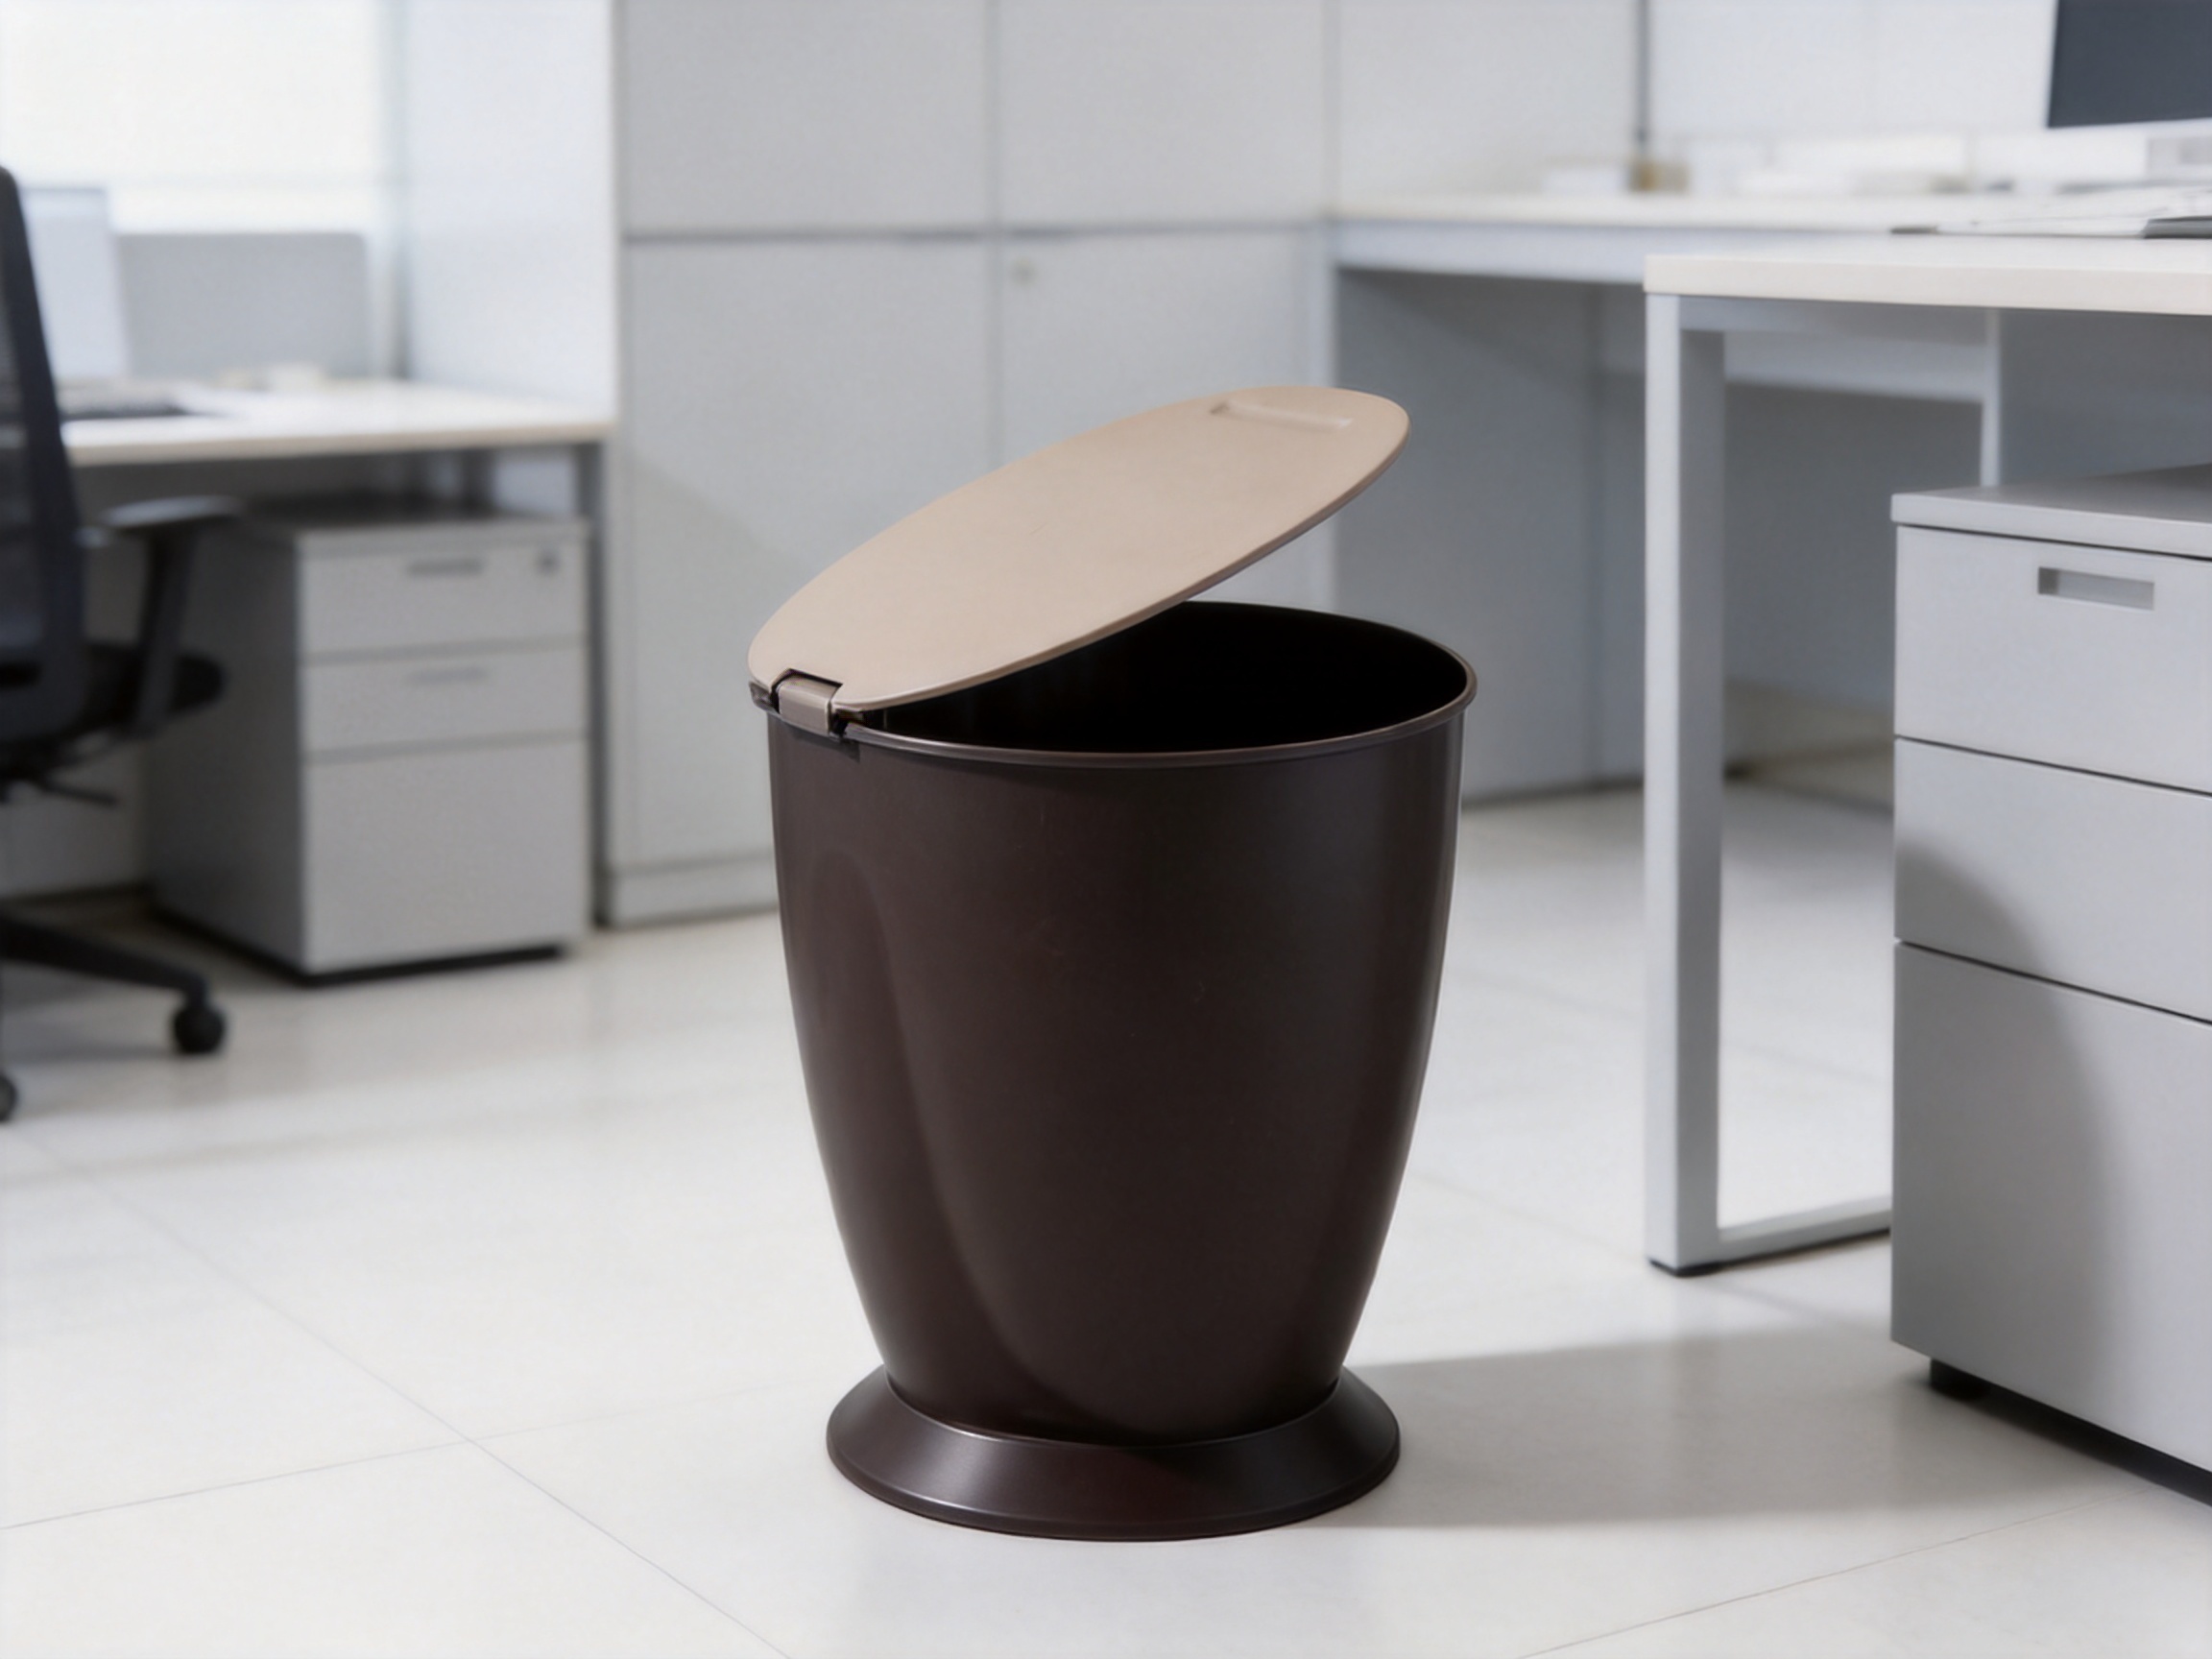
The Top-Lid Household Plastic Trash Bin Injection Mould is designed to form a practical plastic waste bin with a top-lid structure. The product concept is suitable for containers that need to protect waste from view, reduce odors, and provide a cleaner appearance in domestic or commercial settings. Depending on the final product design, the lid can be configured for different opening methods, dimensions, and functional requirements.
A trash bin is normally subjected to repeated opening, closing, handling, loading, and cleaning. Its body must resist deformation when filled, while the rim and lid must maintain sufficient strength for regular use. For this reason, the mould supports an integrated lid structure and a reinforced bucket body. These features help manufacturers develop products that feel stable in the hand and remain serviceable during extended daily use.
The tooling is applicable to PP and HDPE, two materials widely used in household plastic products. Polypropylene can provide a useful balance of low weight, stiffness, chemical resistance, and cost efficiency. HDPE is valued for toughness, impact resistance, and reliable performance in many general-purpose container applications. The selected material, grade, additives, color, and processing conditions can be adjusted according to the intended product specification.
The standard configuration includes a hot runner system and one cavity. A hot runner can reduce cold runner waste and deliver molten plastic more directly to the gate area. A single-cavity layout is suitable for large products where mould size, filling balance, product handling, and dimensional control are more important than maximizing the number of parts produced per cycle. The configuration can also simplify part inspection and process adjustment.
2. Main Technical Specifications
| Item | Specification | Production Significance |
|---|---|---|
| Mould type | Top-lid household plastic trash bin injection mould | Forms a waste container with a practical upper lid structure |
| Typical applications | Household, office, bathroom, and general waste bins | Supports multiple daily-use container markets |
| Compatible product materials | PP / HDPE | Suitable for lightweight and durable plastic products |
| Mould steel | P20 / 718 | Provides a practical base for production tooling and serviceability |
| Runner system | Hot runner | Helps reduce runner waste and improve melt delivery |
| Cavity configuration | 1 cavity | Supports control of large-product filling and dimensions |
| Target mould life | 600,000 shots | Suitable for sustained commercial production |
| Key design features | Integrated lid structure, reinforced body, optimized gate, cooling system | Addresses appearance, strength, and dimensional stability |
The specifications represent the basic configuration described for this product. Final mould dimensions, steel grades, surface finishes, ejection details, cooling circuit arrangements, and compatible injection machine requirements should be confirmed during product development. A complete technical review is especially important when the bin includes a pedal mechanism, soft-close lid, decorative texture, odor-control feature, or specialized internal components.
3. Structural Design of the Bin and Lid
3.1 Reinforced Bucket Body
The bin body is designed with reinforcement in areas that may experience higher loads or handling stress. These areas can include the upper rim, base, corners, side walls, and locations where handles or supporting components are attached. Reinforcement should be carefully balanced because excessive material concentration can increase cycle time and create sink marks, while insufficient support can lead to flexing or deformation.
A well-designed injection mould helps reproduce consistent ribs, bosses, supports, and wall transitions. These details provide structural strength without requiring the entire product to have a thick wall. When the reinforcement is properly integrated into the product design, manufacturers can achieve a stronger bin while controlling material consumption and overall product weight.
The reinforced body also benefits downstream operations. A stable rim can make lid assembly easier, and a more rigid base can help the bin stand evenly on floors. Consistent dimensions reduce the risk of difficult fitting, uneven gaps, and lid misalignment. These benefits are particularly important for retailers and users who expect a household waste container to look neat and function smoothly directly after purchase.
3.2 Integrated Top-Lid Structure
The top-lid structure gives the finished bin a more complete and hygienic appearance than an open container. It can help conceal waste and may support better organization in kitchens, bathrooms, offices, and shared areas. The mould is developed to support integration between the upper body and lid-related geometry, allowing the manufacturer to produce a coordinated product design.
Depending on the customer’s requirements, the lid may be designed around a hinged, lift-up, flip-top, or other opening arrangement. The basic customization scope includes bin capacity and lid structure. Further details, such as hinge position, lid thickness, clearance, opening angle, handle shape, and external texture, should be incorporated during the engineering stage.
Lid fit is a critical quality factor. If the opening is too tight, the lid may bind during use. If the clearance is too large, the product may appear poorly assembled or allow excessive movement. The mould therefore needs accurate machining and careful consideration of shrinkage, draft angles, parting lines, and assembly tolerances. Stable mould construction helps maintain these relationships across repeated production cycles.
3.3 Draft and Ejection Considerations
Large container products require suitable draft angles to release smoothly from the mould. Insufficient draft may cause scuffing, drag marks, deformation, or difficult ejection. Excessive draft can affect the usable internal volume or visual appearance. The correct balance depends on the product geometry, surface texture, material, and release direction.
Ejection must be distributed in a way that supports the product without leaving unacceptable marks on visible surfaces. Large thin-wall products can flex during ejection, so the ejection system must provide sufficient and even force. The design should also minimize stress around corners, ribs, and other concentrated features. These considerations are part of the design review before steel cutting begins.
4. Gate Design and Surface Quality
The visible exterior of a household trash bin is an important selling feature. Consumers often judge product quality by the smoothness, consistency, and cleanliness of the external surface. Sink marks, blush, flow marks, weld lines, and uneven gloss can make a product appear inexpensive even when its structural performance is acceptable.
The Top-Lid Household Plastic Trash Bin Injection Mould uses an optimized gate design intended to help prevent sink marks on visible surfaces. Gate location affects the direction and speed of molten plastic flow, the pressure distribution inside the cavity, the position of weld lines, and the way the product compensates for volumetric shrinkage during packing. A carefully selected gate can therefore improve both appearance and dimensional consistency.
Gate optimization is especially relevant to reinforced products. Ribs and bosses may cool at different rates from the surrounding wall. If the gate is poorly positioned, thicker areas may draw material from nearby surfaces during cooling, leaving visible depressions. A suitable gate and packing strategy can help reduce this effect, although final performance also depends on resin grade, melt temperature, mould temperature, injection speed, holding pressure, and cooling time.
The mould can be prepared for a range of surface finishes according to the intended market. A polished surface may suit smooth, modern household products, while a fine texture can help conceal minor handling marks and provide a more practical appearance. Textured surfaces require appropriate draft and carefully controlled machining or etching. The selected finish should be reviewed together with the product’s branding, cleaning requirements, and color scheme.
5. Cooling Design for Large Plastic Products
Cooling is one of the most important factors in the production of a large plastic bin. After molten resin fills the cavity, the product must release heat evenly so that it can be ejected without excessive deformation. If one area cools faster than another, internal stress and differential shrinkage can lead to warpage, twisting, uneven walls, or a lid that no longer fits correctly.
The mould incorporates cooling arrangements intended to support dimensional stability for large products. Cooling channels should be planned around the geometry of the bin body, rim, base, corners, and lid-related features. The objective is not simply to remove heat, but to remove it in a balanced and controllable way. A uniform temperature profile can improve cycle repeatability and reduce the need for excessive cooling time.
Effective cooling can also improve production economics. If the product requires unnecessarily long cooling, the injection machine remains occupied for more time, reducing output. If cooling is insufficient, the part may be ejected too early and require additional handling or may become distorted. A balanced cooling system therefore contributes to both quality and productivity.
Cooling performance depends on more than channel layout. Water temperature, flow rate, pressure, circuit balance, connector condition, and regular cleaning all influence results. Manufacturers should maintain the cooling system and monitor whether scale, rust, or blockage reduces water flow. The mould’s cooling performance should also be evaluated during initial trials and after extended production.
6. Hot Runner Advantages
The specified hot runner system is an important feature of the mould. In a conventional cold runner system, plastic in the runner solidifies with each cycle and becomes runner waste or requires regrinding. A hot runner keeps the material in a heated state so that it can be delivered to the cavity during the next cycle. This can reduce material waste and simplify post-moulding separation.
For a large trash bin, the quantity of runner material can be significant if a conventional system is used. A hot runner can therefore improve material utilization, particularly in high-volume production. It may also support more direct control of the filling process by placing the gate at a suitable location for the product design.
Hot runner tooling requires precise temperature control and proper maintenance. Heater performance, thermocouple accuracy, nozzle condition, insulation, and controller settings must be managed carefully. When these factors are controlled, the system can provide stable melt delivery and support consistent product quality. The correct hot runner configuration should be selected according to resin type, flow characteristics, color requirements, and the planned production cycle.
Compared with a basic cold-runner mould, this configuration can offer advantages in material savings, reduced runner handling, and cleaner automated production. These advantages are particularly relevant to manufacturers seeking to lower waste, improve production efficiency, and maintain a consistent appearance across large parts.
7. Material Compatibility: PP and HDPE
7.1 Polypropylene
Polypropylene is commonly selected for household containers because it is lightweight, relatively economical, and resistant to many everyday chemicals. It can provide a useful combination of rigidity and flexibility, depending on the selected grade and design. PP is suitable for products that need to be moved frequently, cleaned regularly, or produced in a range of colors.
When PP is used, the processor should consider shrinkage, flow length, melt temperature, mould temperature, and packing pressure. The selected grade may influence impact strength, surface gloss, stiffness, and cycle time. Color masterbatch and additives should be properly dispersed to avoid streaks or inconsistent appearance. Processing conditions should be established through mould trials rather than assumed from one material grade to another.
7.2 High-Density Polyethylene
HDPE is known for toughness, impact resistance, and good performance in many container applications. It may be appropriate when the finished bin must tolerate frequent handling or occasional impact. HDPE also offers useful chemical resistance for general household environments.
As with PP, the exact HDPE grade affects shrinkage and processing behavior. The moulding process should account for the relationship between wall thickness, cooling rate, packing, and product dimensions. A material change from PP to HDPE may require adjustments to injection speed, holding pressure, cooling time, and ejection conditions. The mould can support both materials, but production parameters should be validated separately.
7.3 Material Selection and Sustainability
Material selection should reflect the product’s required strength, weight, appearance, service environment, and target price. Manufacturers may also evaluate recycled content or recyclable grades where appropriate. The use of a hot runner can support a lower level of runner waste, while a durable mould helps reduce the environmental impact associated with frequent tooling replacement.
Any recycled material or additive package should be tested for flow behavior, odor, color consistency, impact performance, and dimensional stability. Product requirements and local regulations may also influence the permitted material composition. A detailed material review at the beginning of the project helps avoid changes after mould completion.
8. Mould Steel and Expected Service Life
The stated mould steel options are P20 and 718. These steels are widely used in injection mould construction and can provide a practical combination of machinability, strength, polishability, and serviceability for many production applications. The final steel selection should reflect the expected production volume, resin characteristics, surface finish, maintenance plan, and customer budget.
P20 is frequently used for mould components that require dependable general-purpose performance and efficient machining. 718 can be selected where improved mechanical performance or surface quality is desired for certain mould components. The appropriate heat treatment, hardness condition, machining method, and surface preparation are important to the actual performance of the finished tooling.
The mould is specified with a target life of 600,000 shots. This indicates suitability for sustained commercial manufacturing rather than limited sampling. Actual mould life depends on operating conditions, material abrasiveness, injection pressure, maintenance quality, cooling-water condition, mould handling, and replacement of wear components. Regular inspection and preventive maintenance are essential to achieve the expected service life.
High-cycle moulding requires attention to the parting surface, guide components, ejector system, hot runner components, seals, cooling circuits, and moving mechanisms. A maintenance schedule can include cleaning, lubrication, inspection for wear, checking water flow, examining the gate area, and verifying that the lid-related features remain dimensionally stable.
9. Advanced Manufacturing Process
The quality of an injection mould depends strongly on the manufacturing process used to create it. A mould may have a strong concept, but inaccurate machining, poor steel preparation, inadequate inspection, or uncontrolled assembly can compromise the final result. A professional manufacturing workflow is therefore necessary from initial product review through final approval.
9.1 Product and Mould Design Review
The process begins with a review of the product concept, three-dimensional data, material, expected production volume, surface requirements, and functional details. Engineers examine wall thickness, ribs, corners, draft angles, parting lines, ejection areas, gates, cooling channels, and potential shrinkage behavior.
For a top-lid trash bin, the review should also consider the relationship between the lid and body. The engineers need to confirm whether the lid is moulded as part of the same product, produced as a separate component, or designed around an additional assembly. The selected approach influences cavity layout, ejection, tooling complexity, and final assembly.
Design review can identify potential manufacturing risks before steel is cut. If a corner is too sharp, a wall is too thick, or a rib is not properly connected, the design team can propose an adjustment. Early correction is more economical than modifying a completed mould or attempting to solve a fundamental design issue through processing alone.
9.2 Flow and Filling Analysis
Large plastic products benefit from engineering analysis before machining. Filling analysis can help evaluate gate position, flow length, filling balance, pressure requirements, weld-line locations, air traps, and potential areas of hesitation. Cooling and warpage analysis can also provide useful guidance for channel placement and expected dimensional behavior.
Analysis does not replace physical trials, but it can reduce uncertainty and guide the design toward a more robust configuration. It is particularly valuable when the product has complex reinforcement, a large visible surface, multiple functional openings, or strict lid-fit requirements. The results can be reviewed with the customer before final tooling construction.
9.3 CNC Machining and EDM
Computer numerical control machining is used to create accurate mould components and cavity surfaces. Milling strategies are selected according to the steel condition, geometry, required surface finish, and tolerance. Large cavity surfaces need stable machining methods to reduce distortion and maintain uniformity across the product area.
Electrical discharge machining can be used for deep, narrow, or complex features that are difficult to produce through conventional cutting. EDM is useful for detailed ribs, corners, slots, and other areas where electrode-based machining provides better access or accuracy. After machining, the affected surfaces may require polishing, texture preparation, or additional finishing work.
9.4 Polishing, Texturing, and Surface Preparation
Visible surfaces are finished according to the approved product appearance. Polishing can create a smooth and reflective surface, while texture preparation can provide a functional or decorative pattern. The finish must be consistent across the cavity and core areas that form the external product.
Surface preparation also affects release. A poorly finished area may increase friction, cause drag marks, or trap the product during ejection. For textured products, the draft angle must be adequate to prevent the texture from locking against the mould. These factors are reviewed together rather than treated as separate cosmetic concerns.
9.5 Assembly and Fitting
After individual components are machined and finished, the mould is assembled and fitted. Engineers check alignment, parting surfaces, guide systems, ejector movement, hot runner installation, cooling connections, and the operation of any moving sections. Proper fitting helps prevent flash and ensures that the mould opens and closes smoothly.
Large moulds require careful handling during assembly. Support, lifting, storage, and transportation procedures help protect precision surfaces and reduce the risk of accidental damage. Clear identification of components can also simplify future maintenance and replacement.
9.6 Trial Moulding and Corrections
Trial moulding is used to verify the actual relationship between the mould, material, machine, and process parameters. Trial parts are examined for filling, appearance, dimensions, ejection, lid fit, warpage, weld lines, sink marks, and other quality characteristics. The results are compared with the approved product requirements.
If adjustments are needed, they may involve process settings, venting, gate balancing, cooling flow, ejection timing, or limited mould modification. A professional trial process records the findings and confirms whether the corrective action has solved the issue. This structured approach is more reliable than making undocumented changes based on visual judgment alone.
10. Company Manufacturing Strengths
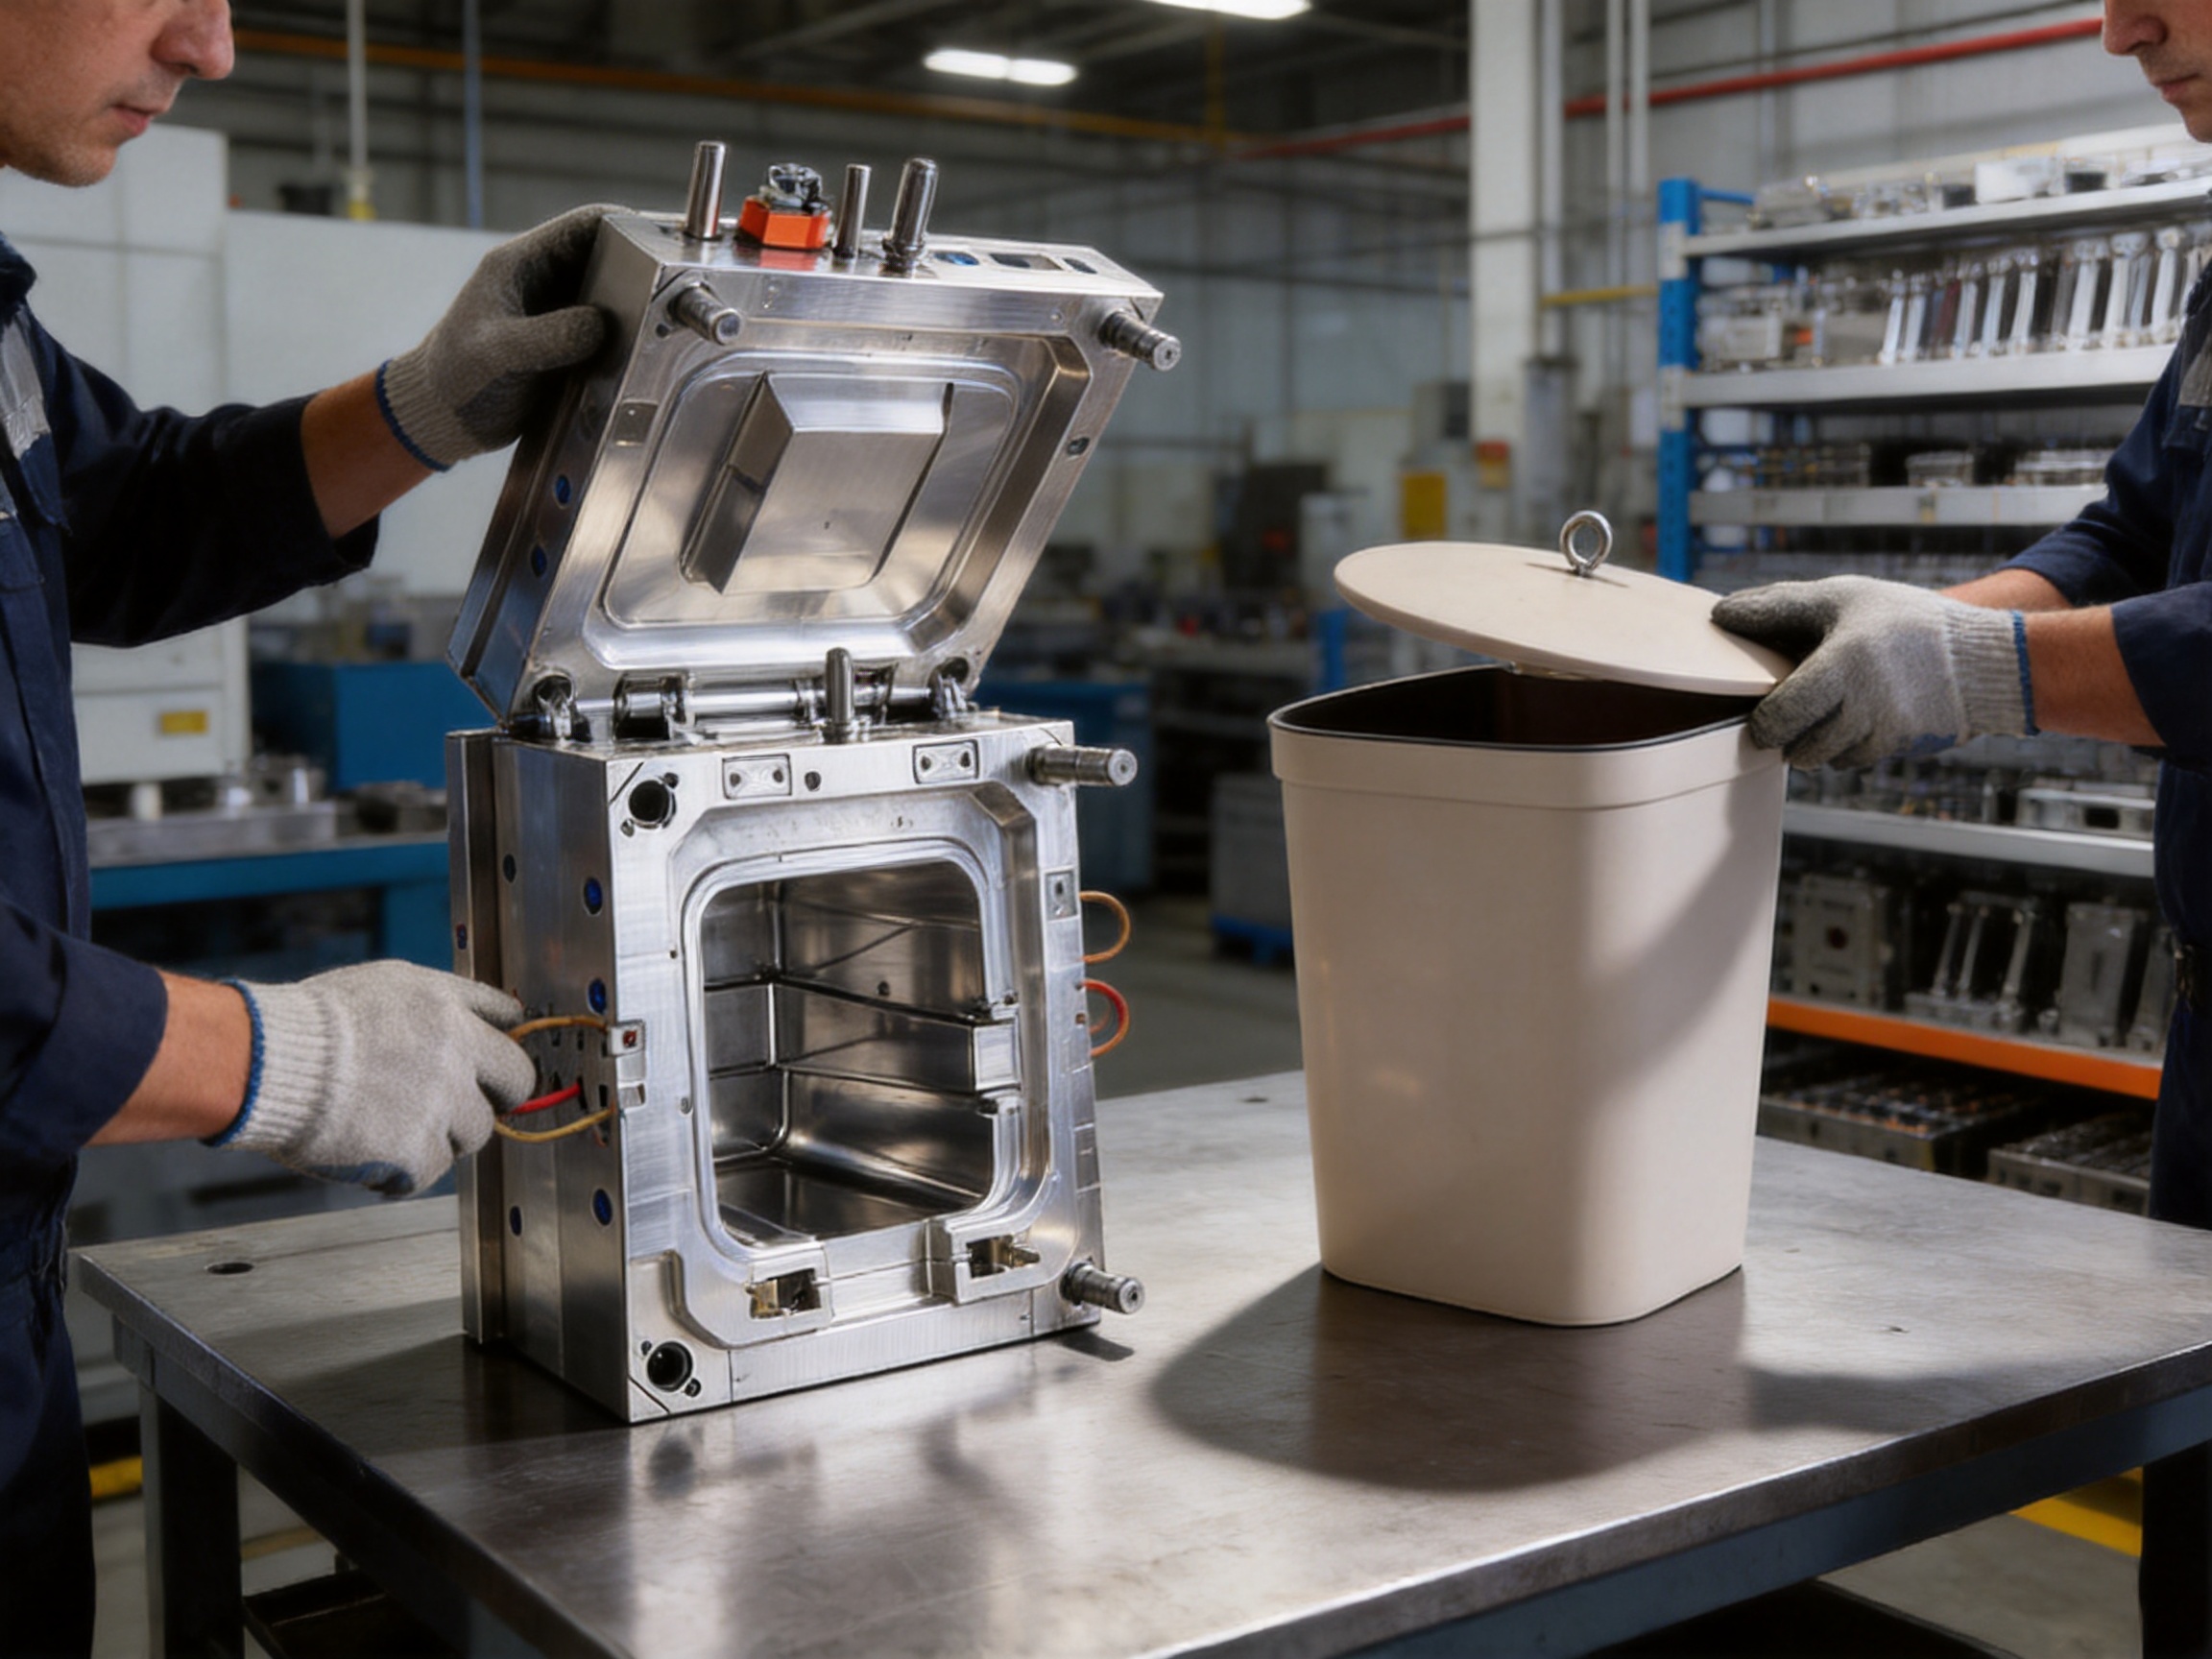
Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. is presented as a high-tech enterprise specializing in the research, development, and manufacturing of precision injection moulds. Its business covers daily necessities, home appliances, automotive parts, and industrial equipment. This sector coverage gives the company experience with a variety of product sizes, functional requirements, materials, and tooling structures.
The company emphasizes a professional design team and a scientific production management system. These capabilities are important for large household moulds because successful delivery depends on coordination between product design, mould engineering, machining, fitting, trial production, inspection, and customer communication. An organized production system helps maintain traceability and reduces the risk of overlooked details.
Haiquan provides integrated services from design and production to after-sales support. For customers purchasing a trash bin mould, integrated service can simplify communication. Instead of dividing responsibility among multiple suppliers, the customer can work with one mould partner for design review, tooling construction, trial support, technical documentation, and maintenance guidance.
The company’s stated philosophy of “Quality First, Sustainable Development” is relevant to long-life production tooling. Quality-first mould manufacturing focuses on repeatability, reliable components, appropriate steel, accurate machining, and stable trial results. Sustainable development can also relate to improving production efficiency, reducing material waste, extending mould life, and supporting customers in different international markets.
With exports to Europe, the Middle East, Southeast Asia, and South America, the company has experience serving customers with different market expectations and product applications. International mould supply requires attention to communication, packaging, documentation, delivery coordination, machine compatibility, and after-sales response. These factors can be as important to the customer’s success as the mould’s cavity geometry.
11. Advantages Over Basic or Conventional Competitor Tooling
11.1 Better Control of Large Product Dimensions
Some basic trash bin moulds focus mainly on forming the outside shape and may not provide sufficient attention to cooling balance, reinforcement, or lid alignment. The Top-Lid Household Plastic Trash Bin Injection Mould is designed with dimensional stability for large products as a stated objective. Its cooling arrangements and reinforced structure are intended to help control deformation during production.
Better dimensional control can reduce downstream problems such as unstable bases, uneven rims, excessive lid gaps, or parts that require manual correction. This advantage is especially useful for manufacturers supplying retail products, where consistent appearance across batches affects customer satisfaction and brand reputation.
11.2 Reduced Visible Sink-Mark Risk
Reinforced containers often have thicker sections around ribs and structural features. Without suitable gate and packing design, these areas can create sink marks on visible surfaces. The optimized gate design is intended to reduce this risk, giving the mould an advantage over less carefully engineered tooling.
Reduced sink-mark risk does not mean that defects are impossible. Material grade, processing settings, cooling, and product design remain important. However, placing and sizing the gate with the product’s visible areas in mind provides a stronger foundation for consistent appearance than simply selecting a gate for convenience.
11.3 Lower Runner Waste
The hot runner system can reduce the amount of solidified runner material produced per cycle. In a high-volume operation, the reduction in runner waste may contribute to lower material costs and less handling. It can also support a cleaner automated production process because operators do not need to separate a large cold runner from every moulded part.
Compared with a basic cold-runner mould, the hot runner configuration may offer improved material efficiency. The customer should nevertheless consider the additional requirements for temperature control, start-up, shutdown, cleaning, and maintenance when evaluating total ownership cost.
11.4 Longer Production Planning Horizon
A stated life of 600,000 shots gives manufacturers a useful basis for production planning. When a mould is designed for sustained use, the customer can estimate output, schedule maintenance, and organize replacement components more effectively. A longer-life tool can also reduce the disruption and expense associated with early mould replacement.
Service life should always be understood as a target under suitable operating and maintenance conditions. Even a well-made mould can experience premature wear if abrasive materials, excessive pressure, contaminated cooling water, poor lubrication, or incorrect handling are involved. The advantage comes from combining sound construction with disciplined maintenance.
11.5 Flexible Household Product Applications
The mould concept can support several related waste-bin markets, including household, office, and bathroom products. Basic customization of capacity and lid structure gives the customer an opportunity to adapt the product to different sales channels without abandoning the fundamental tooling concept.
This flexibility can be valuable for manufacturers that serve private-label customers or multiple regional markets. Variations in capacity, color, surface texture, and lid configuration can help create product families while retaining common design principles. The exact extent of modification depends on whether the change can be achieved through replaceable inserts or requires new mould components.
12. Production Workflow for Customers
A successful mould project should begin with a clear product brief. The customer should provide the desired bin capacity, external dimensions, wall thickness, lid style, material, color, surface finish, annual volume, target cycle time, and injection machine information. Photographs or reference samples can help clarify appearance expectations, but complete three-dimensional product data is preferred.
The next stage is design evaluation. Engineers review the product for mouldability and identify potential issues involving draft, wall thickness, ribs, undercuts, parting lines, gates, cooling, and ejection. Any recommended changes should be documented and approved before tooling construction.
After design approval, the mould is manufactured using the agreed steel, runner system, cavity configuration, and surface finish. During this stage, the customer may receive progress information related to steel preparation, rough machining, fine machining, assembly, and trial scheduling. Clear communication helps align expectations regarding delivery and technical approval.
Trial production follows mould assembly. The trial should use the intended or a technically comparable material and an injection machine with suitable capacity. The resulting parts are assessed against the approved drawings and samples. If changes are required, the correction process should be recorded and verified through another trial or inspection.
Before shipment, the mould should be cleaned, protected, and packed for international transportation where applicable. Relevant documentation may include mould drawings, spare-part information, material recommendations, trial records, inspection results, and operating guidance. These documents can help the customer install and maintain the tool more efficiently at its own facility.
13. Quality Control and Inspection
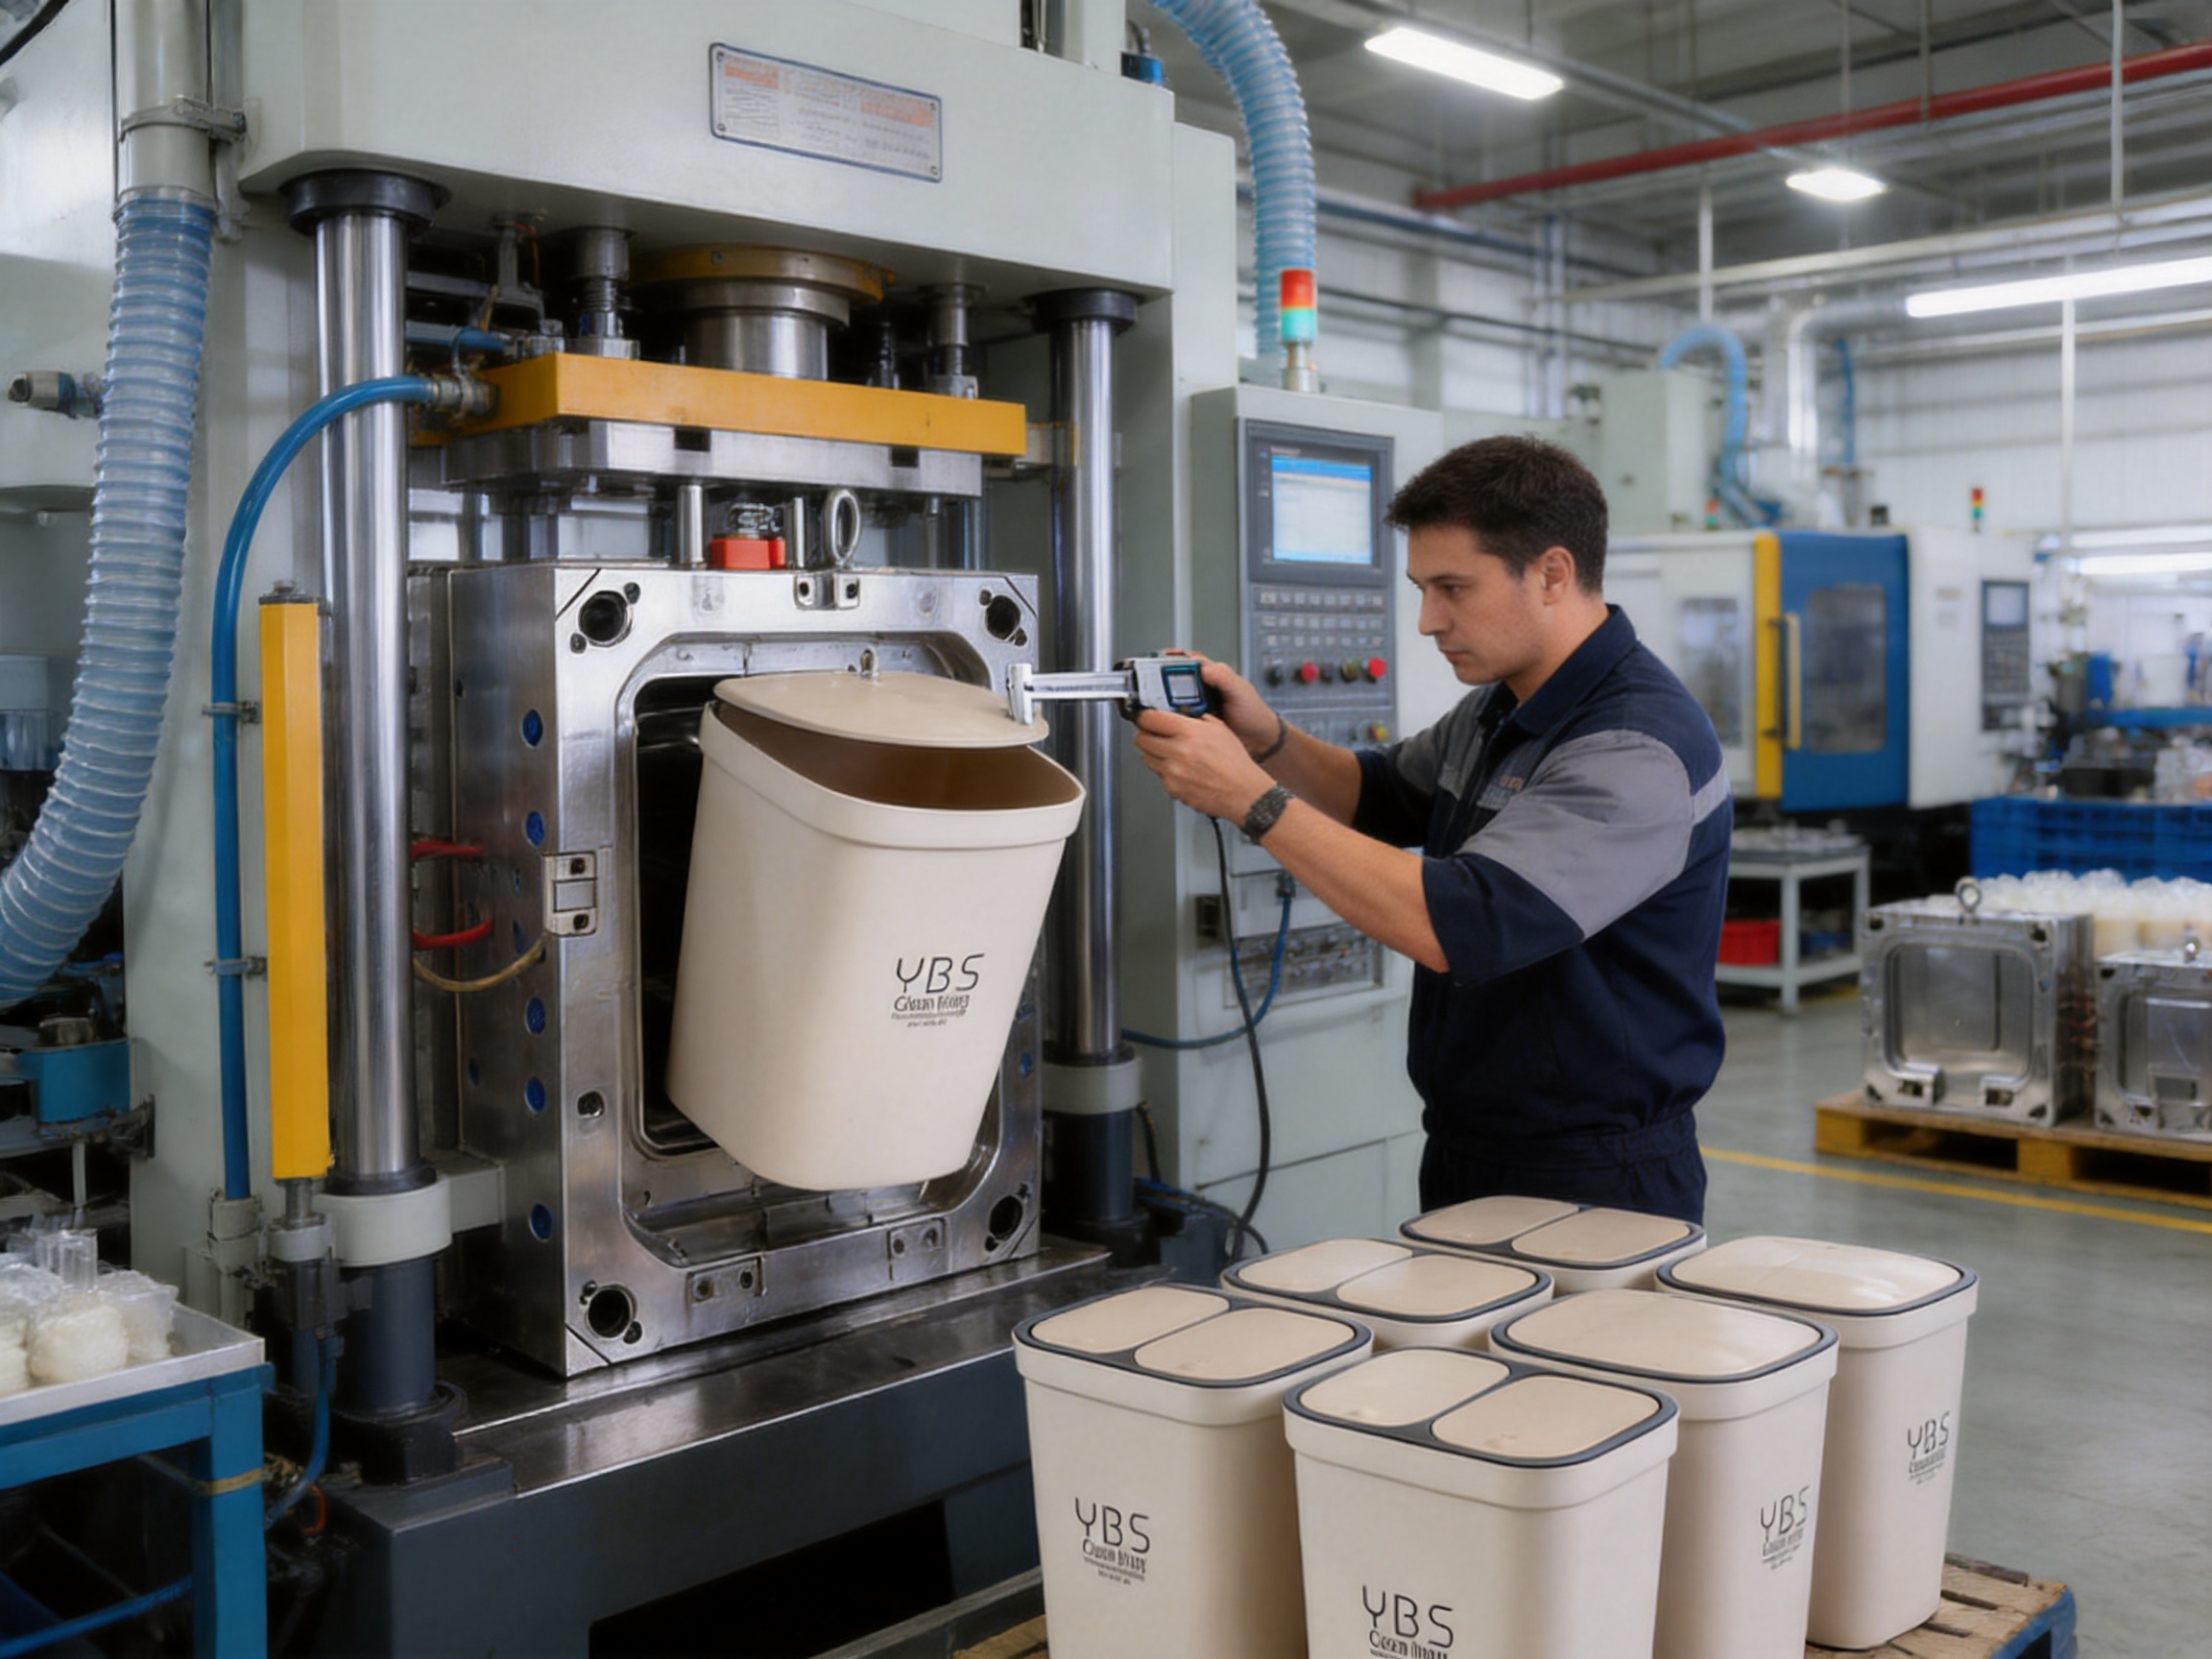
Quality control should cover both the mould and the moulded product. Mould inspection can include checks of cavity dimensions, parting-line fit, ejector movement, guide alignment, cooling-circuit pressure, hot runner function, and surface finish. Product inspection can include weight, overall dimensions, wall thickness, lid fit, appearance, base stability, and functional opening and closing.
For a large trash bin, dimensional inspection should not be limited to a few points. The body may shrink or distort differently at the base, side walls, rim, and corners. Measuring multiple locations provides a clearer understanding of stability. The lid and body should also be inspected as a matched set when their fit is a key product requirement.
Appearance standards should be established before production. The customer should define acceptable limits for flow marks, weld lines, color variation, gate vestige, polishing variation, texture consistency, and minor surface imperfections. Clear standards help prevent disagreement during final approval.
Process control is equally important after mould delivery. Operators should record injection pressure, filling time, holding pressure, cooling time, melt temperature, mould temperature, and cycle time. Monitoring these values helps identify gradual changes that may indicate material variation, cooling blockage, hot runner instability, or mould wear.
14. Maintenance Recommendations
Regular maintenance helps preserve mould accuracy and extend service life. After production, the mould should be cleaned of resin residue, dust, and moisture. Parting surfaces should be protected from corrosion, and moving components should receive suitable lubrication according to the mould manufacturer’s guidance.
The hot runner should be checked for temperature stability and signs of leakage or blockage. Sudden changes in heating behavior can indicate a damaged heater, thermocouple, controller, or nozzle. Problems should be addressed before they affect a large production batch.
Cooling circuits should be monitored for flow reduction, scale, rust, and leakage. Periodic flushing or water-treatment procedures may be necessary depending on local water quality. Poor cooling performance can gradually increase cycle time and cause dimensional variation even when the mould cavity itself remains in good condition.
Ejector pins, guide pillars, bushings, slides, and other moving parts should be inspected for wear. Uneven wear may indicate insufficient lubrication, misalignment, excessive load, or contamination. Replacing a low-cost wear component at the correct time can prevent more expensive damage to the mould base or cavity.
Maintenance records should include production shots, inspection dates, replaced parts, observed defects, and corrective actions. A shot-count record is particularly useful for a mould with a target life of 600,000 shots. It allows the customer to plan inspections before problems become visible in the product.
15. Application Areas
15.1 Household Waste Bins
In homes, the product can be used in kitchens, bedrooms, living areas, utility rooms, and other spaces. A top lid can provide a cleaner appearance and help conceal daily waste. Different capacities can be selected for compact rooms, family kitchens, or larger general-purpose applications.
15.2 Office Waste Containers
Offices often require bins that look organized and professional. The product can be adapted for deskside or shared-area use depending on its capacity and opening structure. A robust body and consistent surface finish support repeated handling by cleaning staff and office users.
15.3 Bathroom Garbage Bins
Bathroom bins generally benefit from compact dimensions, easy cleaning, and a lid structure that helps keep waste concealed. PP or HDPE can provide suitable resistance for everyday household environments. Surface design and lid operation should be selected to make cleaning and emptying convenient.
15.4 Public and Commercial Environments
Although the basic product is oriented toward household and office use, related designs may be considered for shops, clinics, hotels, educational facilities, and other commercial locations. Such applications may require increased capacity, stronger handles, heavier walls, or specialized lid and liner arrangements.
16. Customization Options
Basic customization includes bin capacity and lid structure. Capacity changes may affect the overall height, width, wall thickness, base geometry, cavity dimensions, cooling layout, and ejection method. The customer should therefore treat capacity changes as an engineering modification rather than a simple visual adjustment.
Lid customization can involve the opening direction, hinge position, lid profile, handle, clearance, thickness, and operating force. If the lid includes additional mechanisms, those components must be reviewed together with the mould design. A simple lid may be produced with straightforward tooling, while a soft-close, pedal-operated, or multi-part lid may require additional moulds and assembly processes.
Additional options may include color, surface texture, logo areas, label recesses, anti-slip details, handles, internal supports, and stackability features. Each feature should be assessed for its impact on flow, cooling, ejection, draft, tooling cost, and production cycle time.
Manufacturers should also consider packaging and logistics at the design stage. A bin that nests efficiently can reduce storage and transportation costs, while a lid that remains attached or fits securely can simplify retail handling. These practical considerations can influence the moulded geometry and should be included in the initial product brief.
17. Frequently Asked Questions
Q1: What products can this mould manufacture?
The mould is designed for top-lid household plastic trash bins. Typical applications include household trash bins, office waste containers, and bathroom garbage bins. Related commercial applications may also be possible after engineering review.
Q2: Which plastics are compatible with the mould?
The listed product materials are polypropylene and high-density polyethylene. The exact grade should be selected according to the required strength, appearance, shrinkage, impact performance, and processing conditions. PP and HDPE should be validated separately because their processing behavior is not identical.
Q3: Why is a hot runner used?
A hot runner delivers molten plastic through heated channels and can reduce cold runner waste. It may also support efficient filling of a large product. The system requires proper temperature control and maintenance for reliable operation.
Q4: Why is the mould configured with one cavity?
A one-cavity configuration can be suitable for a relatively large product where filling balance, mould size, dimensional control, and manageable tooling cost are priorities. It also simplifies product inspection and process adjustment. The final cavity count should reflect the customer’s required output.
Q5: How long can the mould last?
The stated target mould life is 600,000 shots. Actual life depends on steel condition, material, injection pressure, cooling-water quality, maintenance, lubrication, and operating practices. Preventive maintenance is essential to achieve the expected service life.
Q6: Can the bin capacity be customized?
Yes. Basic customization includes bin capacity. A capacity change may affect the mould dimensions, cooling arrangement, ejection system, and product shrinkage, so it should be reviewed during the design stage.
Q7: Can the lid structure be changed?
Yes. The lid structure can be customized within the agreed tooling concept. The customer should specify the desired opening method, hinge or handle arrangement, clearance, thickness, and operating requirements before mould design is finalized.
Q8: How does the mould help reduce sink marks?
The mould uses an optimized gate design intended to reduce sink marks on visible surfaces. Final results also depend on wall thickness, rib design, material grade, packing pressure, mould temperature, and cooling conditions.
Q9: What should be considered when changing from PP to HDPE?
A material change may require new injection, holding, and cooling parameters because PP and HDPE have different flow and shrinkage characteristics. The customer should conduct a dedicated trial and verify dimensions, appearance, lid fit, and product strength.
Q10: What information should a customer provide before ordering?
The customer should provide product drawings or three-dimensional data, capacity, material, color, surface finish, lid structure, expected annual volume, injection machine information, packaging requirements, and any applicable quality standards. Reference samples can also help clarify the intended appearance.
Q11: Is the mould suitable for automated production?
The hot runner and one-cavity configuration can support an efficient production workflow, and automation may be considered depending on the machine, product geometry, ejection method, and handling requirements. Automation details should be reviewed during the tooling design stage.
Q12: What is the company’s service scope?
Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. provides services covering mould design, production, trial support, and after-sales assistance. The company specializes in precision injection moulds for daily necessities, home appliances, automotive parts, and industrial equipment.
18. Conclusion
The Top-Lid Household Plastic Trash Bin Injection Mould is a practical tooling solution for manufacturers producing durable and attractive waste containers. Its key features include a reinforced bucket body, integrated top-lid structure, optimized gate design, cooling suited to large products, hot runner technology, PP and HDPE compatibility, one-cavity construction, P20 or 718 mould steel, and a target life of 600,000 shots.
Compared with basic tooling, the mould is designed to provide better attention to large-product dimensional stability, visible-surface quality, material efficiency, and sustained production. Its advantages depend on correct product design, suitable material selection, disciplined injection parameters, and regular maintenance, but the tooling structure provides a solid foundation for consistent manufacturing.
The manufacturing strengths of Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. support this product concept. The company combines precision injection mould development, professional design capability, scientific production management, international customer experience, and integrated service from design through after-sales support. These strengths can help customers reduce development risks and establish a more reliable production process.
For manufacturers seeking a dependable mould for household, office, bathroom, or related waste-bin applications, this tooling offers a balanced combination of durability, customization potential, production efficiency, and long-term serviceability. A detailed engineering review before construction will ensure that the final mould matches the required capacity, lid arrangement, material, surface finish, production volume, and injection machine.
References
1. Product technical information for the Top-Lid Household Plastic Trash Bin Injection Mould, including material, steel, runner, cavity, and service-life specifications.
2. General injection mould design principles for large polypropylene and high-density polyethylene containers.
3. General guidelines for hot runner system selection, temperature control, and maintenance.
4. General mould engineering practices for gate design, cooling-channel planning, ejection, draft, and dimensional stability.
5. General quality-control practices for plastic injection moulds and large household injection-moulded products.
6. Company information concerning Taizhou Huangyan Haiquan Plastic Mold Co., Ltd., its product sectors, design capabilities, manufacturing management, export markets, and integrated customer services.
Product: Top-Lid Household Plastic Trash Bin Injection Mould

For exclusive deals and latest offers, sign up by entering your email address below.











 +86-18657672567
 sales@tzhqmould.com
celin@tzhqmould.com
 No. 17 Houshi Road, Beicheng Industrial Zone, Huangyan District, Taizhou City, Zhejiang Province, China
Copyright © Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. All Rights Reserved
Injection Plastic Mould Maker

