

Household Plastic Basin and Bucket Injection Mould: Durable Tooling for High-Performance Daily Necessities
Admin 2026-10-12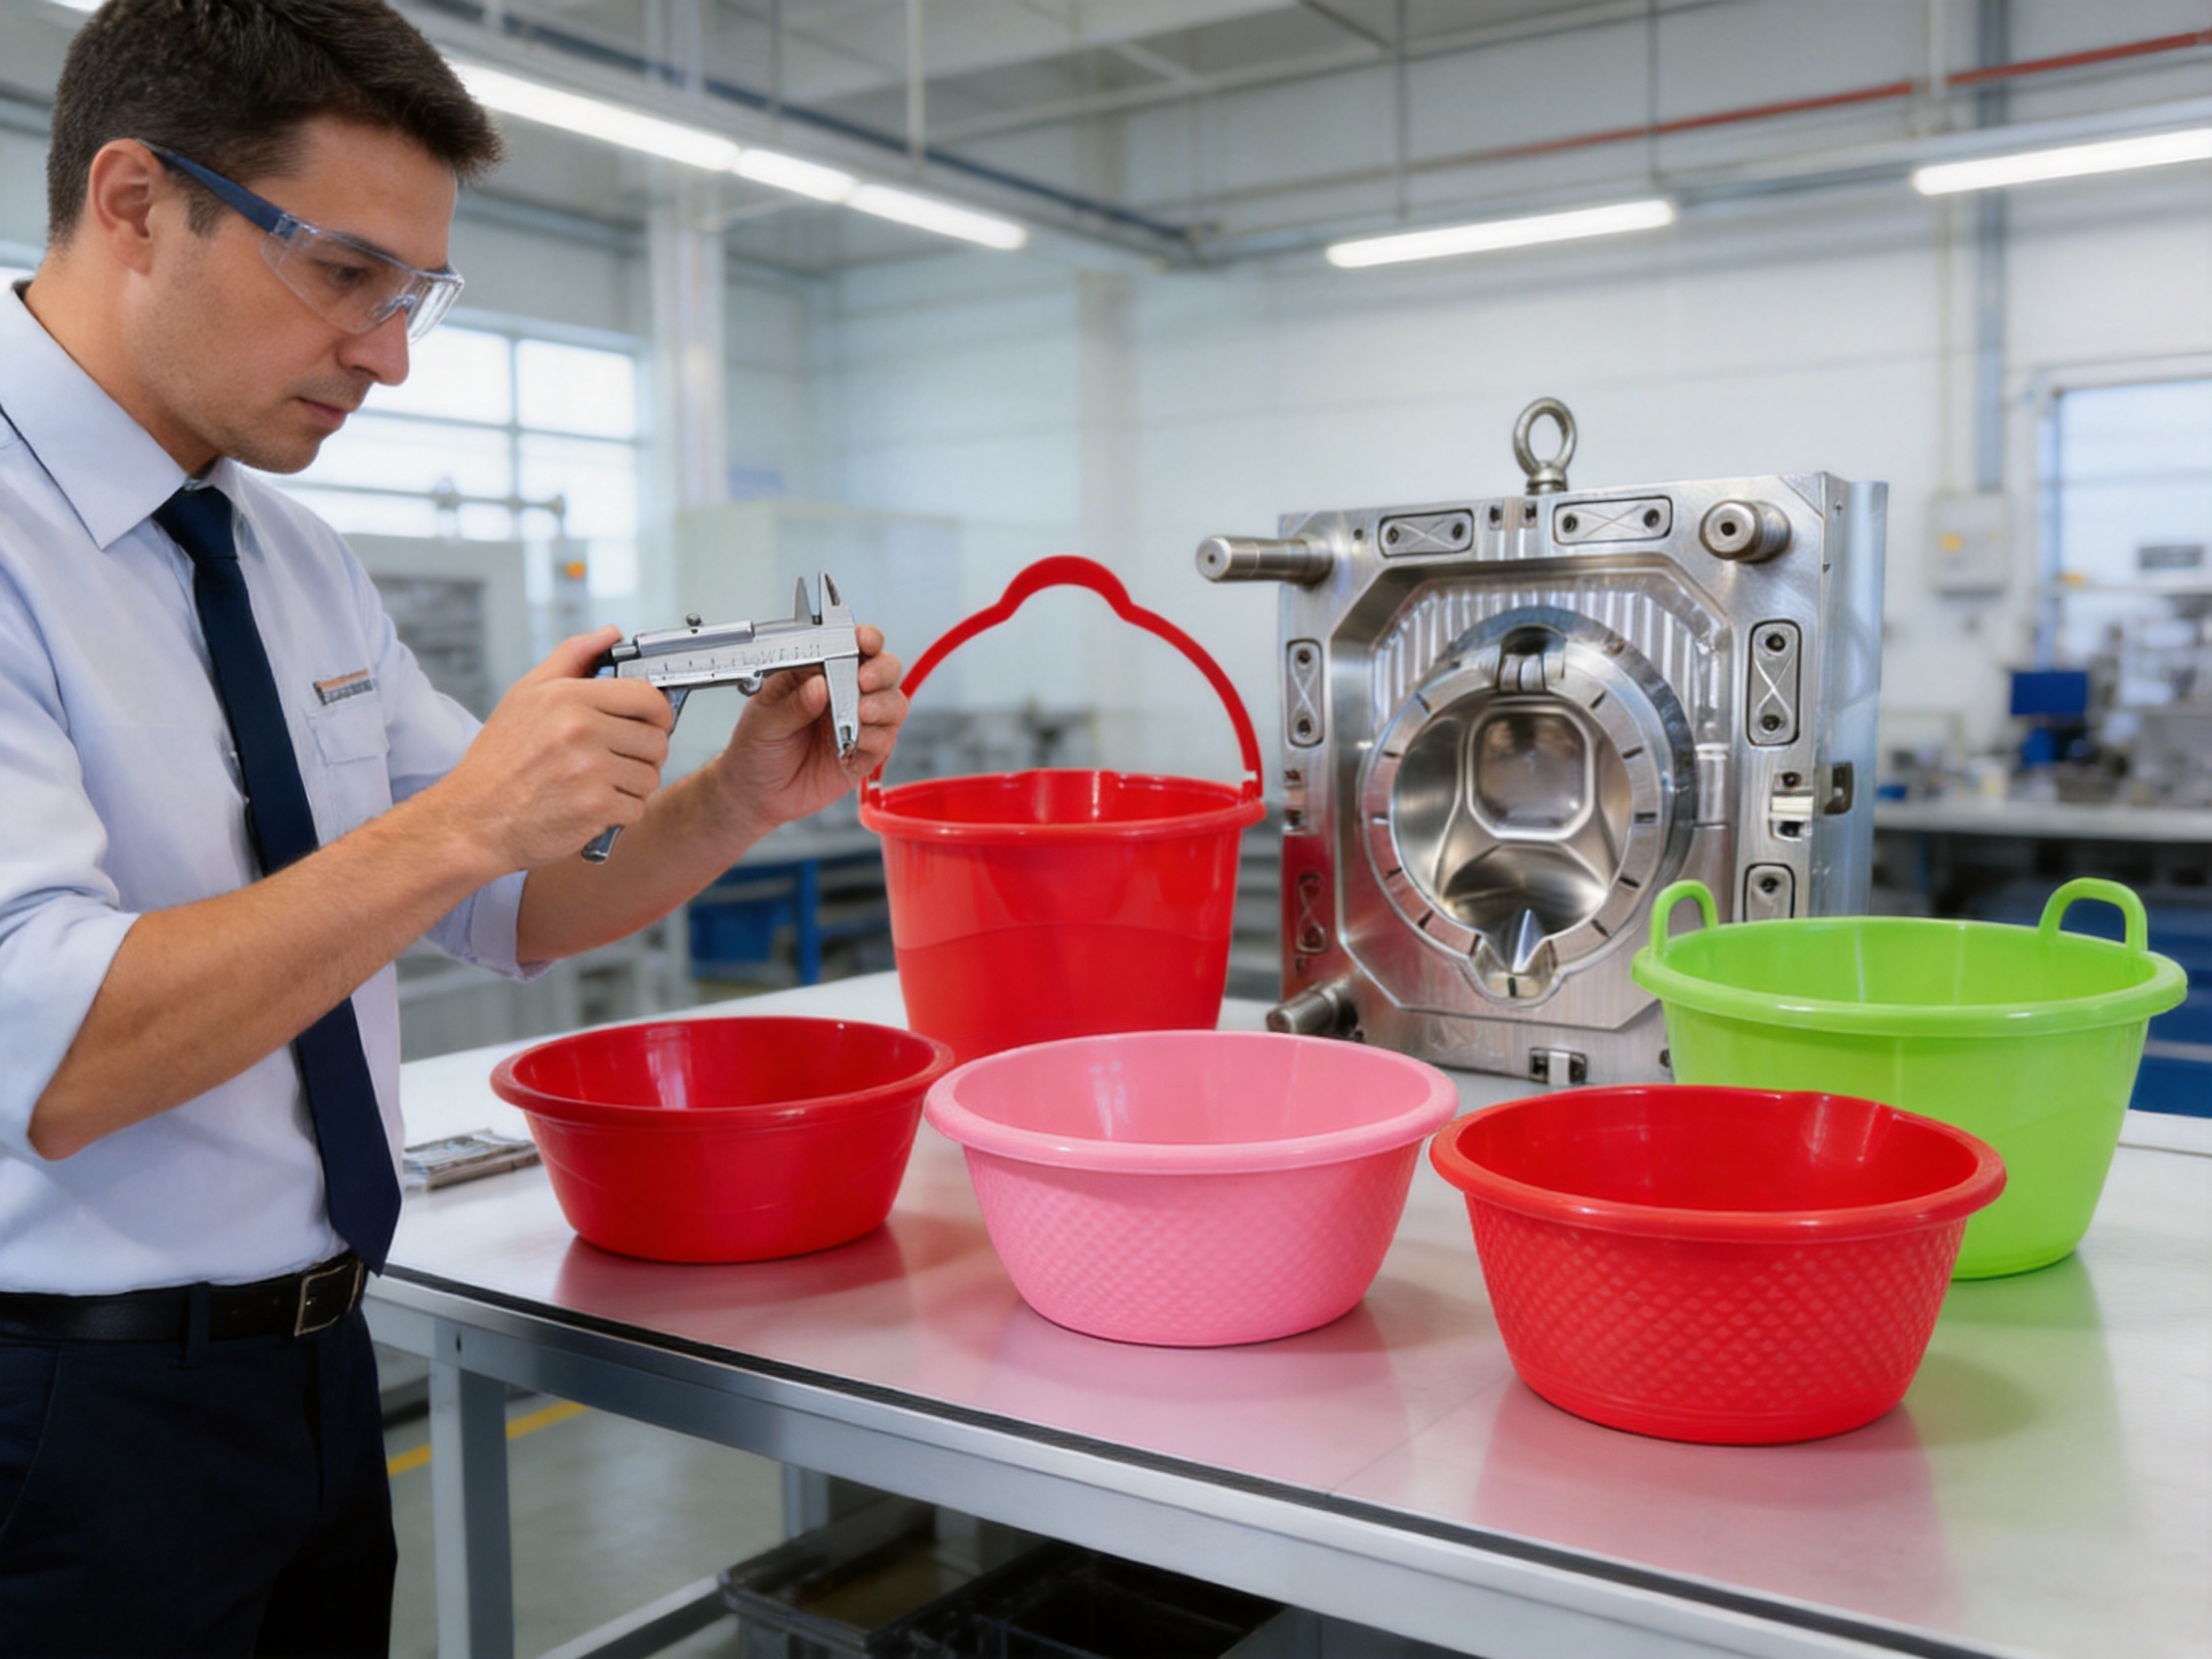
Household basins and buckets are among the most frequently used plastic products in modern homes, commercial facilities, cleaning operations, bathrooms, and utility areas. Although these products appear simple, producing them consistently requires carefully engineered injection moulding tooling. Large open containers must maintain a stable shape, resist impact, support repeated handling, and remain attractive after many production cycles. The mould must also control wall thickness, manage cooling, form strong rims, and create practical handles without introducing weak points or visible defects.
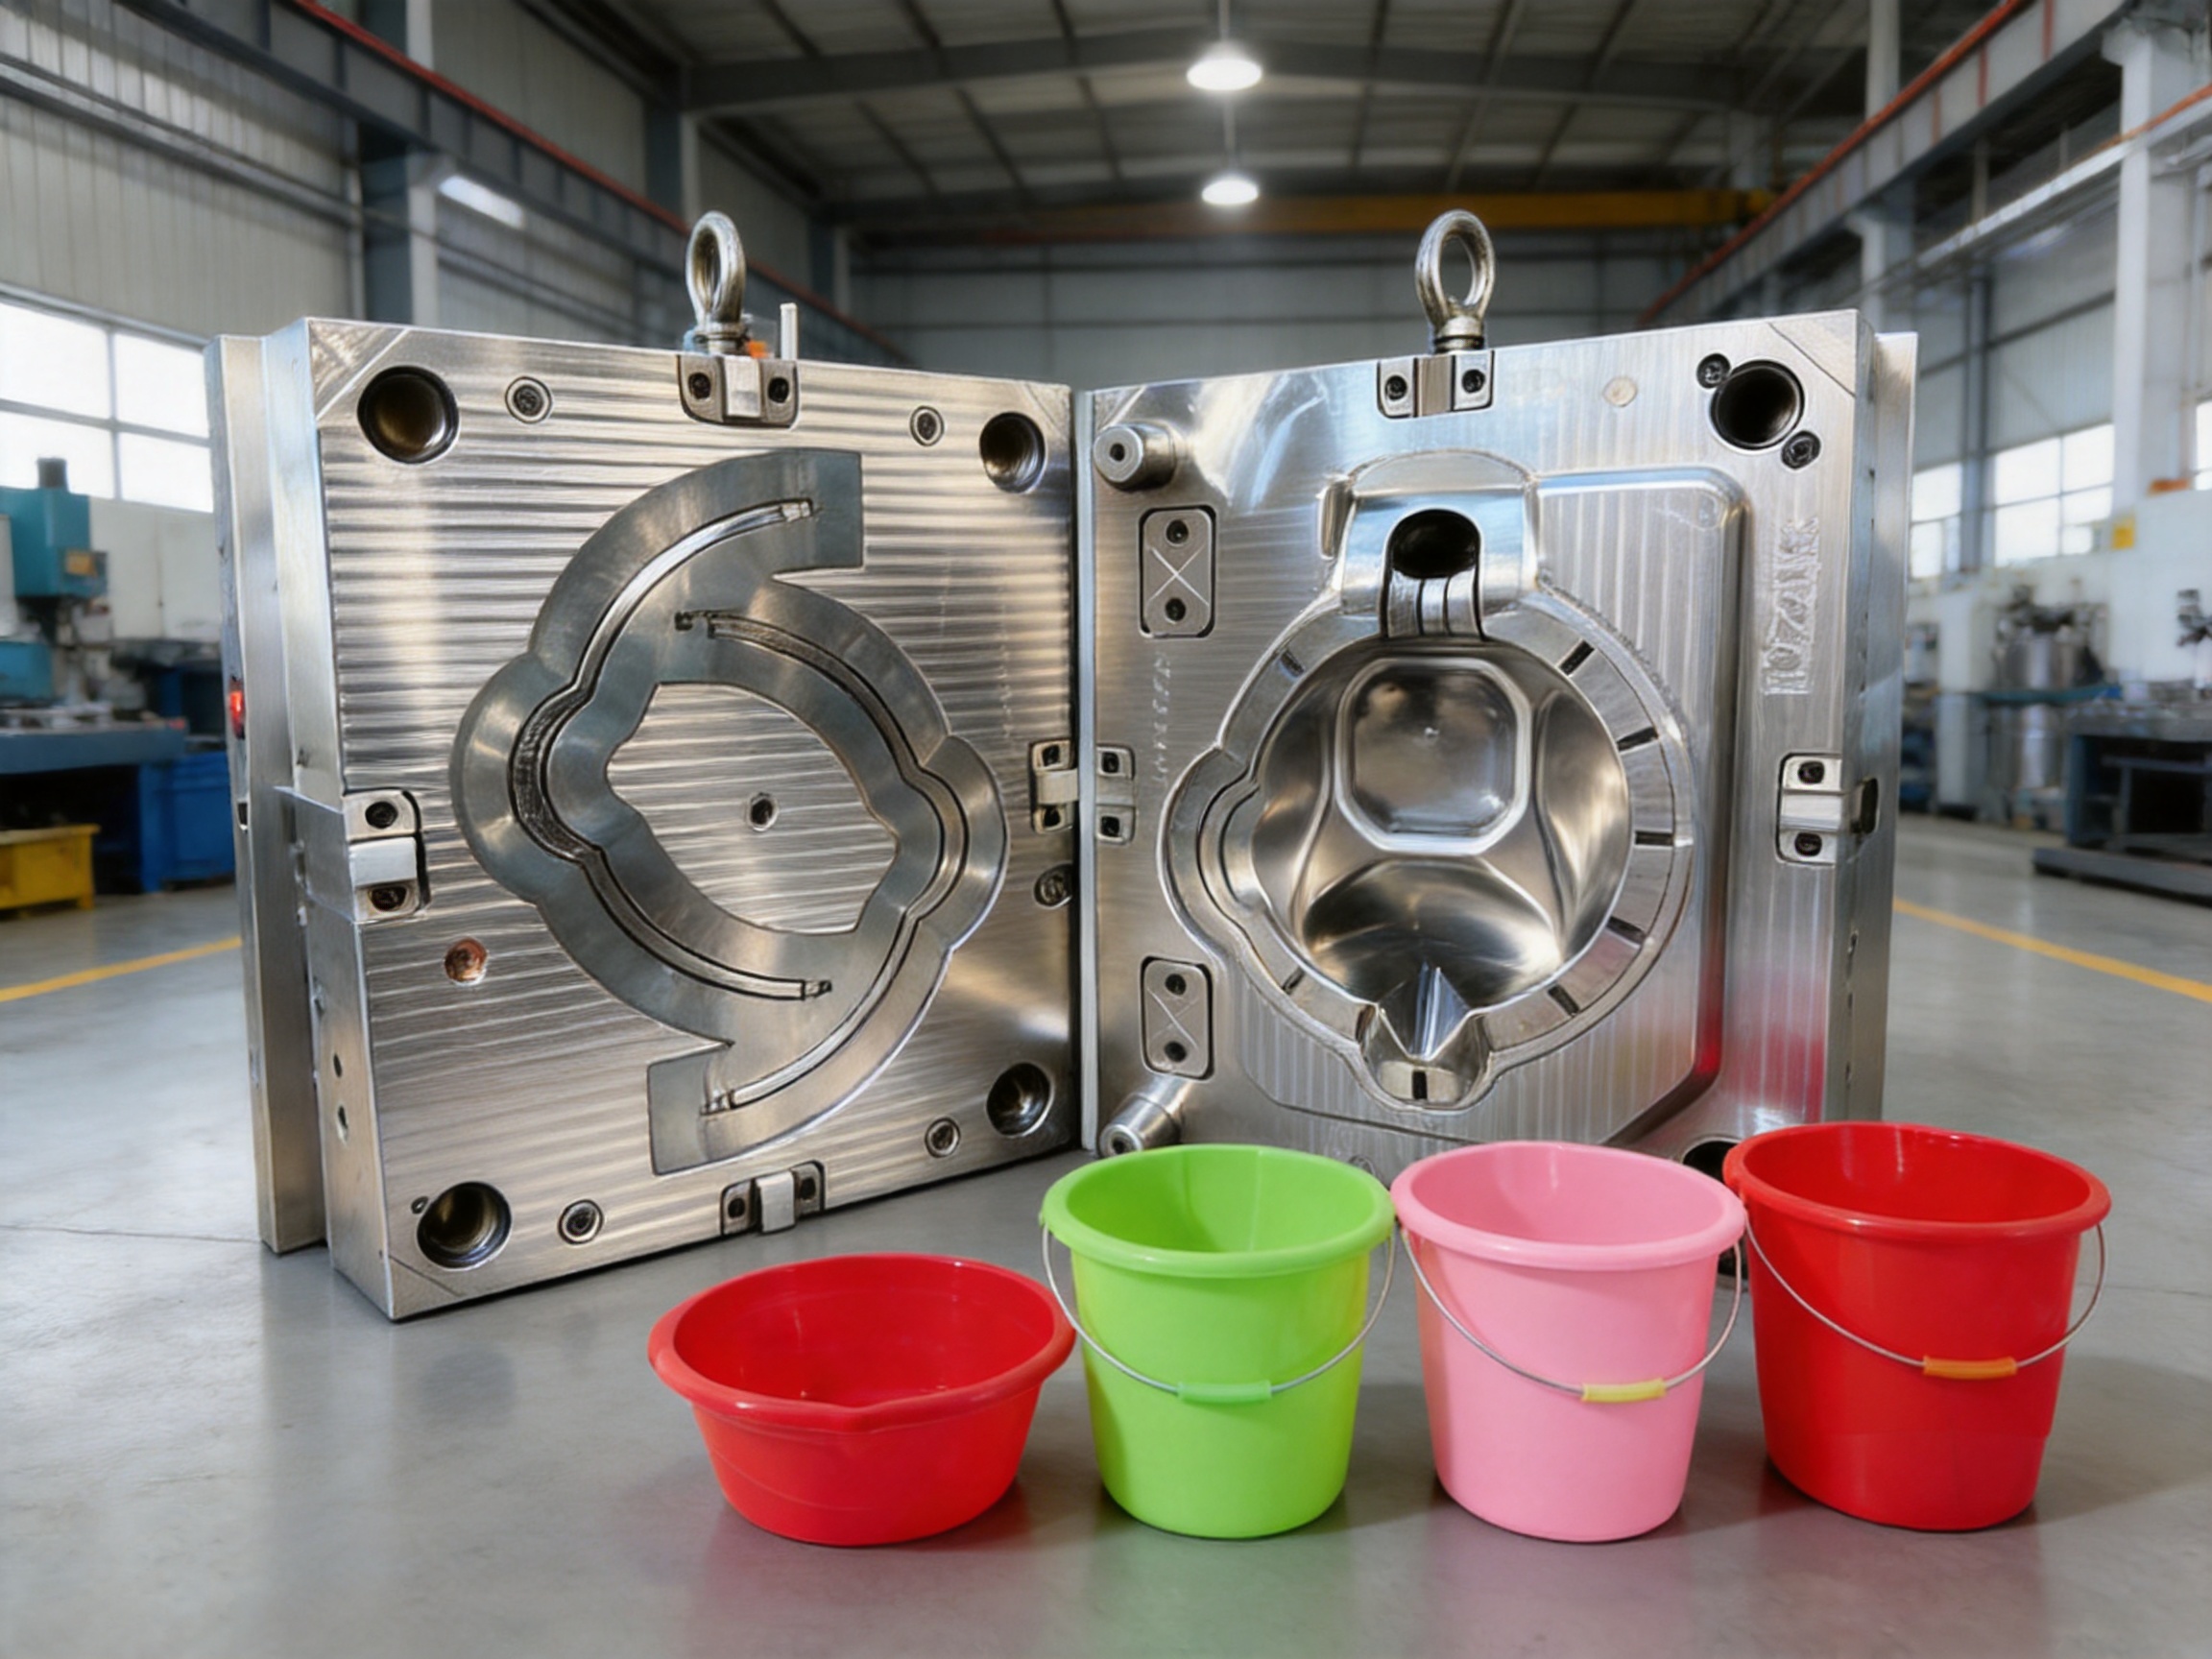
The Household Plastic Basin and Bucket Injection Mould is developed specifically for these requirements. It is a production-focused solution for manufacturers that need dependable tooling for washing basins, cleaning buckets, bathroom water containers, and utility storage buckets. Its design combines structural strength, balanced moulding performance, practical customization, and compatibility with commonly used polypropylene and polyethylene materials.
Manufactured by Taizhou Huangyan Haiquan Plastic Mold Co., Ltd., this injection mould reflects the company’s experience in daily necessities moulds and precision plastic tooling. Haiquan provides integrated support covering product development, mould design, manufacturing, testing, delivery, and after-sales service. Its capabilities are supported by a professional design team, scientific production management, and an export-oriented quality system serving customers in Europe, the Middle East, Southeast Asia, and South America.
Why Basin and Bucket Mould Quality Matters
A plastic basin or bucket must perform reliably under everyday conditions. Users may fill it with water, cleaning solutions, laundry, tools, or other household items. The product can be carried by its rim or handle, placed on uneven floors, stacked with similar products, and exposed to repeated washing. If the mould is poorly designed, the finished article may warp, crack, leak, or become difficult to use.
The mould therefore needs to do more than reproduce the basic outline of a container. It must distribute molten plastic evenly throughout the cavity, maintain a stable wall profile, form smooth surfaces, support efficient demoulding, and remove heat at a controlled rate. These technical factors directly influence production cost, product reliability, appearance, and customer satisfaction.
For manufacturers, mould consistency is equally important. A basin or bucket mould may be used for hundreds of thousands of cycles. Small dimensional changes can create major production problems when multiplied across a long manufacturing run. Unstable moulding may lead to short shots, sink marks, deformation, flash, uneven handles, or excessive scrap. A carefully engineered mould helps reduce these risks while supporting a more predictable production schedule.
The Household Plastic Basin and Bucket Injection Mould addresses these challenges through a structure designed for large daily-use plastic parts. The design emphasizes strong rim construction, balanced wall thickness, integrated handle options, smooth product surfaces, and an optimized cooling layout. These features work together to produce containers that are practical, durable, and suitable for high-volume production.

Household Plastic Basin and Bucket Injection Mould
Product Design for Everyday Strength
Strong Rim Structure
The rim is one of the most important areas of a basin or bucket. It defines the opening, provides a gripping edge, affects stacking, and contributes to the overall rigidity of the container. A weak or poorly supported rim can deform when the product is lifted, filled, stacked, or exposed to heat.
This mould is designed to form a strong and stable rim structure. The rim can be engineered with suitable reinforcement according to the product size, material, and intended application. By supporting the upper edge of the container, the mould helps the finished product maintain its shape during repeated daily use.
A stable rim also improves the user experience. It makes the basin or bucket easier to hold, pour, clean, and store. For commercial or institutional users, such as cleaning companies, hotels, workshops, and facility management teams, rim strength is particularly valuable because products may be handled many times each day.
Balanced Wall Thickness
Large plastic containers are vulnerable to uneven cooling and differential shrinkage. If one area is significantly thicker than another, the product may cool at different speeds and become distorted. Uneven wall thickness can also create weak sections, visible sink marks, unnecessary material consumption, and dimensional inconsistency.
The mould design focuses on balanced wall thickness to help prevent deformation. During the design phase, the cavity geometry, core structure, gate position, filling path, and cooling arrangement can be evaluated together. This coordinated approach helps the molten PP or PE reach the required areas with a more controlled flow pattern.
Balanced walls are beneficial in several ways. They can improve product stiffness, support more uniform shrinkage, reduce weight variation, and help the finished basin or bucket retain its intended geometry. They may also allow manufacturers to use material more efficiently without sacrificing practical strength.
Handle Integration
Handles are an important functional feature for many bucket designs. A handle must be comfortable enough for carrying while remaining firmly connected to the container body. The connection area must tolerate the weight of the contents and repeated lifting forces.
Handle integration can be included directly in the mould design. Depending on the customer’s product concept, the tooling can accommodate different handle positions, shapes, connection details, and reinforcement requirements. This makes it possible to develop a bucket that matches a specific market, brand range, capacity, or user group.
Direct consideration of the handle during mould development helps avoid last-minute modifications that may compromise the mould structure. It also allows the design team to evaluate the relationship between handle geometry, wall thickness, demoulding direction, filling behavior, and cooling performance.
Smooth and Easy-to-Clean Surfaces
Basins and buckets are commonly used with water, detergents, soaps, food-related materials, garden products, and cleaning chemicals. Their surfaces should therefore be easy to wash and resistant to retaining dirt. A well-finished cavity surface helps create a smooth product surface with fewer areas where residue can accumulate.
The mould can be supplied with a polished or matte surface finish. A polished finish may be selected where a smooth, bright, and easy-to-clean appearance is preferred. A matte finish may be more appropriate where a softer visual effect, reduced glare, or a particular tactile quality is desired.
Surface treatment is not only an aesthetic decision. It can influence demoulding, product maintenance, visible mould marks, and the perceived quality of the finished article. Haiquan’s mould manufacturing process allows the surface finish to be considered as part of the complete tooling specification rather than as an isolated final step.
Applications of the Injection Mould
The mould is suitable for a broad range of daily necessities. Its flexible design allows manufacturers to produce products for household, commercial, and utility applications.
Household Washing Basins
Washing basins are used for laundry, hand washing, soaking, cleaning, and general household tasks. They may need a wide opening, stable base, comfortable rim, and sufficient depth. The mould can be adapted to different diameters, heights, capacities, and shapes to suit regional consumer preferences.
Cleaning Buckets
Cleaning buckets are commonly used with mops, brushes, detergents, and water. They require good carrying strength and practical handling. A reinforced rim and optional integrated handle design support daily cleaning operations in homes, offices, hotels, restaurants, and public facilities.
Bathroom Water Containers
Bathroom containers must remain stable in wet environments and should be easy to rinse. Smooth surfaces and controlled wall thickness are valuable for this application. The mould can be configured to produce compact containers for limited spaces or larger vessels for homes and commercial facilities where water storage is required.
Utility Storage Buckets
Utility buckets may be used to store tools, gardening materials, workshop components, or household supplies. These products often require greater impact resistance and a stronger body. Material selection, wall design, bottom geometry, and handle construction can be adjusted according to the expected load and service conditions.
Advantages Over Basic or Poorly Engineered Tooling
Not every basin and bucket mould provides the same production value. A low-cost mould may appear attractive initially but can create higher operating expenses through short service life, unstable cycles, excessive maintenance, inconsistent products, and frequent production interruptions.
More Reliable Long-Term Performance
The specified mould life is up to 700,000 shots when suitable materials, processing conditions, maintenance practices, and operating procedures are used. This service-life target gives manufacturers a strong foundation for long-term production planning. It can reduce the need for frequent replacement and help distribute tooling investment across a larger number of finished products.
The use of P20 or H13 mould steel allows the tooling specification to be matched to the customer’s performance requirements. P20 is widely used for dependable general-purpose mould construction and provides a practical balance between machinability, strength, and cost. H13 offers enhanced performance for demanding applications where higher thermal resistance and durability are required.
Better Control of Deformation
Large, thin-walled products can easily lose their shape if the mould filling and cooling processes are not properly coordinated. The emphasis on balanced wall thickness and optimized cooling helps control these risks. A more stable product geometry can improve stacking, packaging, handling, and customer acceptance.
Flexible Runner System Options
The mould can be configured with either a hot runner or cold runner system. A cold runner may offer a straightforward and economical solution for certain production conditions. A hot runner can reduce runner waste and support more efficient material use in appropriate high-volume applications.
The best choice depends on factors such as product size, resin type, expected output, injection machine capability, cycle time, color changes, maintenance preferences, and budget. Offering both options allows the tooling design to be aligned with the customer’s actual production environment rather than forcing every project into one standard configuration.
One- or Two-Cavity Production
The mould is available with one or two cavities. A single-cavity mould may be suitable for larger products, specialized designs, lower-volume programs, or customers prioritizing simpler tooling. A two-cavity configuration can increase output when the injection machine and product requirements support it.
Cavity selection must consider more than production quantity. The mould base, filling balance, cooling layout, ejection system, machine capacity, and product dimensions all influence the final decision. Haiquan’s design team can evaluate these factors to create a practical cavity configuration for the intended application.
Customization Without Losing Production Discipline
Manufacturers may require different basin sizes, handle designs, capacities, colors, surface textures, or cavity arrangements. The mould can be customized to accommodate these requirements while maintaining a clear focus on manufacturability and service life.
Customization is particularly valuable for distributors and product brands that want to differentiate their household products. A unique shape or handle profile can help a product stand out in a crowded market. At the same time, professional tooling design ensures that customization does not create unnecessary difficulty in filling, cooling, demoulding, or maintenance.
Material Compatibility: PP and PE
The mould is designed for use with polypropylene and polyethylene, two widely adopted materials for household plastic products.
Polypropylene
Polypropylene is frequently used for basins and buckets because it offers a useful combination of low density, chemical resistance, stiffness, and practical processability. It can produce lightweight containers that are suitable for repeated washing and handling. PP is also available in many colors and grades, giving product manufacturers flexibility in appearance and performance.
When PP is selected, the moulding process must account for its shrinkage behavior, flow characteristics, cooling rate, and required impact performance. Gate location and cooling balance are especially important for large parts because uneven thermal conditions can influence final dimensions.
Polyethylene
Polyethylene can provide good toughness, impact resistance, and chemical resistance. Depending on the selected grade, PE may be suitable for products that require a more flexible or resilient body. It is useful for certain utility buckets, water containers, and cleaning products exposed to repeated handling.
PE grades can behave differently during injection moulding, so the final moulding parameters should be established through testing. The mould structure provides a stable platform, while processing conditions can be adjusted according to resin grade, product thickness, color, and machine performance.
Material Selection and Product Requirements
Material selection should be based on the product’s intended use rather than on price alone. A household basin used for light washing may have different requirements from a utility bucket used in a workshop. Load, impact, chemical exposure, flexibility, appearance, temperature, and target service life should all be considered.
Haiquan can support customers in relating the selected PP or PE material to the mould design. This coordination helps reduce the risk of developing a cavity that performs well in theory but does not match the actual resin and production process.
Advanced Mould Manufacturing Process
A high-quality injection mould is the result of multiple controlled stages. Each stage affects the accuracy, reliability, and final performance of the tooling.
Product and Requirement Review
The process begins with a review of the product concept and production objectives. The design team considers the product dimensions, capacity, wall thickness, handle arrangement, surface finish, material, injection machine, annual output, and expected mould life.
This review is important because a mould cannot be designed effectively without understanding how the final basin or bucket will be used. A product intended for household consumers may have different priorities from one intended for industrial cleaning. Early communication also helps identify possible problems with parting lines, draft angles, ejection, undercuts, and assembly.
Three-Dimensional Tooling Design
Three-dimensional design provides a detailed view of the cavity, core, mould base, runner system, cooling channels, ejector components, guide elements, and related mechanisms. The design team can assess the relationship between the product and each mould component before steel is cut.
For a large open container, the three-dimensional design process must pay particular attention to deep cavity areas, rim details, bottom structure, handle interfaces, and demoulding direction. Proper draft design helps the product release smoothly and reduces the risk of scuffing or sticking.
Flow and Filling Considerations
The filling behavior of PP or PE affects product quality. The mould must guide molten plastic through the cavity while limiting excessive pressure variation, weld-line weakness, air entrapment, and incomplete filling. Gate selection and location are evaluated according to the product geometry and desired appearance.
For large parts, a poorly placed gate can produce uneven filling or cause visible marks in a prominent area. A professional mould design considers how the plastic flows around the basin or bucket and how the filling pattern interacts with the handle region, rim, base, and wall transitions.
Cooling System Optimization
Cooling is one of the most important factors in the production of large plastic parts. After injection, the molten material must solidify sufficiently before ejection. If cooling is too slow, cycle times increase. If cooling is uneven, the part may warp or shrink inconsistently.
The cooling system is optimized for large plastic products. Channels are arranged to remove heat from important areas of the core and cavity while supporting a stable temperature distribution. The exact layout depends on product size, wall thickness, mould steel, resin, cycle requirements, and machine conditions.
Effective cooling can improve cycle consistency and help manufacturers achieve more predictable dimensions. It may also reduce production downtime caused by repeated adjustments. Cooling performance should be verified during mould trials and refined when necessary.
CNC Machining and Precision Manufacturing
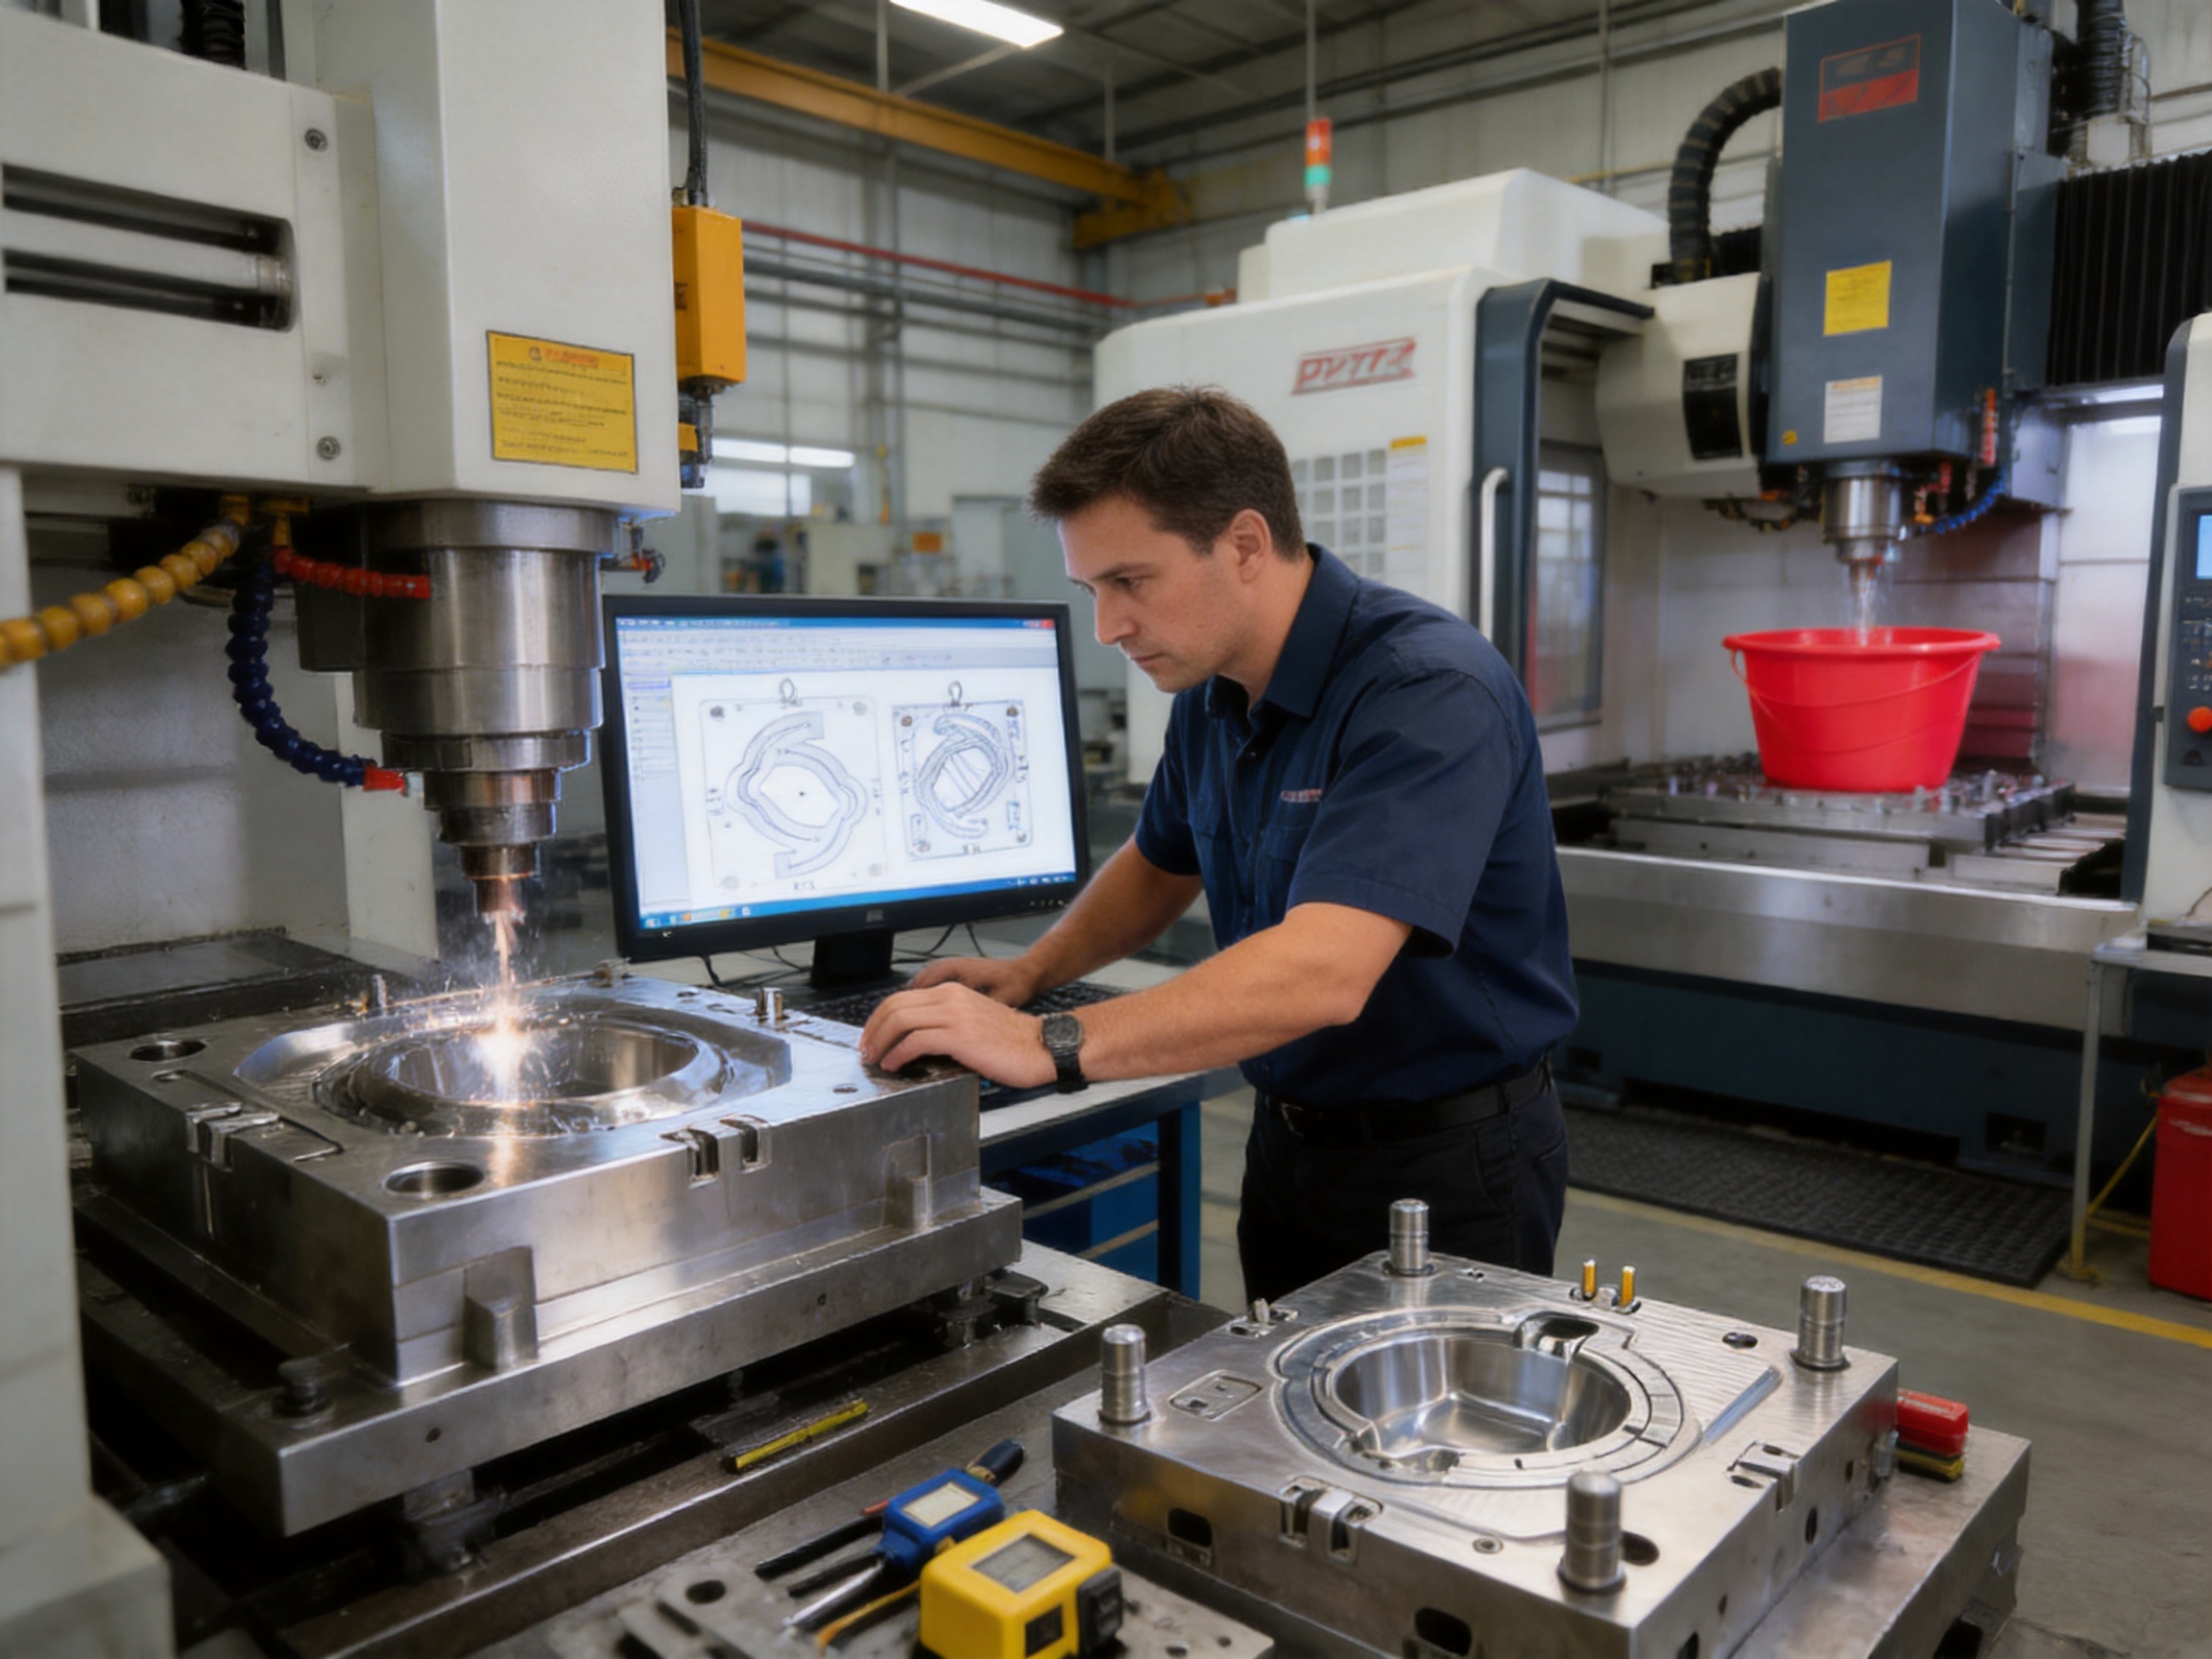
Modern mould production relies on accurate machining to reproduce the designed geometry. CNC machining is used for the cavity, core, mould plates, and other precision components. The machining strategy is selected according to the complexity of the product, material hardness, surface requirements, and dimensional tolerances.
Large household products may look uncomplicated, but their broad surfaces and long edges can reveal machining inconsistencies. Controlled machining helps maintain smooth transitions, stable wall geometry, accurate parting lines, and reliable assembly between mould components.
EDM and Detail Processing
Electrical discharge machining can be used for details that are difficult to produce through conventional cutting. Fine grooves, sharp internal features, handle connections, and other specialized areas may benefit from EDM processing.
Detail processing is completed with consideration for product release and surface quality. Every feature must be functional and manufacturable. Unnecessary sharp corners or poorly positioned details can increase wear and create ejection problems, so professional design judgment remains essential.
Polishing and Surface Treatment
After machining, mould surfaces can be polished or textured according to the selected product finish. Polishing requires patience and process control, particularly across large visible surfaces. An inconsistent finish may create differences in gloss, reflection, or texture on the final basin or bucket.
For matte surfaces, texturing must be carefully matched across connected areas. For polished surfaces, the mould maker must remove machining marks while preserving the intended geometry. These steps contribute directly to product appearance and ease of cleaning.
Mould Assembly and Inspection
After individual components are manufactured, they are assembled into a complete mould system. Fit, movement, alignment, cooling connections, ejector operation, and runner components are inspected. The mould must open and close smoothly while maintaining accurate alignment during repeated cycles.
Inspection may include dimensional checks, visual examination, component verification, and functional testing. Careful assembly reduces the risk of flash, uneven wear, leakage, misalignment, or premature damage during production.
Trial Moulding and Correction
Trial moulding provides an opportunity to evaluate the mould under real or representative production conditions. Test parts are examined for dimensions, wall thickness, appearance, warpage, sink marks, flash, handle strength, filling balance, and ejection performance.
If adjustments are required, the team can refine processing parameters or modify specific mould features. Trial feedback is especially valuable for large products because small changes in cooling, pressure, holding time, or ejection can influence the final result.
Manufacturing Strengths of the Supplier
Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. specializes in precision injection moulds for daily necessities, home appliances, automotive parts, and industrial equipment. This sector experience gives the company a broader technical foundation than a supplier focused only on simple household tooling.
The company operates as a high-tech enterprise with an emphasis on research and development, mould manufacturing, and integrated customer service. Its professional design team supports product development from the earliest concept stage. This can help customers identify design improvements before manufacturing begins, potentially reducing later modification costs.
Scientific production management is another important strength. Injection mould manufacturing involves many linked operations, including design, steel preparation, machining, heat treatment, polishing, assembly, testing, and delivery. A structured management system helps coordinate these activities and maintain visibility across the project.
Quality First and Sustainable Development are central operating principles. In practical terms, this means focusing on stable tooling performance, responsible manufacturing, useful service life, and long-term customer relationships. The objective is not merely to deliver a mould, but to provide tooling that supports reliable production after installation at the customer’s facility.
International experience also contributes to project communication and delivery. Customers in Europe, the Middle East, Southeast Asia, and South America may have different product preferences, machine conditions, documentation practices, and quality expectations. Experience serving diverse markets helps the company adapt its communication and technical coordination to each project.
Technical Specifications
The following specifications provide a general reference for the Household Plastic Basin and Bucket Injection Mould. Final values may be adjusted according to product design, material grade, production volume, and customer requirements.
| Specification | Available Option or Standard | Production Consideration |
| Mould Steel | P20 / H13 | Selected according to durability, thermal demand, budget, and expected production conditions |
| Product Material | PP / PE | Material grade should match impact, stiffness, chemical, and appearance requirements |
| Runner System | Hot Runner or Cold Runner | Chosen according to output, waste reduction, maintenance, and machine conditions |
| Cavity Configuration | 1–2 Cavities | Determined by product size, machine capacity, output target, and filling balance |
| Target Mould Life | Up to 700,000 Shots | Dependent on steel, processing, maintenance, operating conditions, and product design |
| Surface Finish | Polished or Matte | Selected according to appearance, tactile quality, cleaning needs, and market positioning |
| Customization | Basin Size, Handle Design, Cavity Layout | Adapted to the customer’s product portfolio and production plan |
Production Efficiency and Cost Control
Tooling cost should be evaluated over the complete production life rather than only by the initial purchase price. A mould that produces stable parts, runs predictable cycles, and requires limited corrective maintenance can offer a lower total cost of ownership.
The optimized cooling system supports cycle stability for large parts. Efficient cooling may reduce unnecessary waiting time between injection and ejection, although the final cycle depends on the machine, resin, wall thickness, part design, and processing parameters.
Runner selection also affects material use. A cold runner system may be suitable for many applications, but it creates runner material that must be managed. A hot runner can reduce or eliminate certain runner waste conditions and may support higher production efficiency. The correct choice should be made based on the complete production plan rather than on one isolated benefit.
One- or two-cavity configurations provide additional flexibility. A customer launching a new product may prefer one cavity to limit initial tooling investment and simplify validation. A high-volume producer may select two cavities to increase output. By offering both options, the mould can be aligned with the customer’s commercial stage and equipment capacity.
Durability also affects cost. With a target service life of up to 700,000 shots, the mould can support substantial production before replacement becomes necessary when properly operated and maintained. Longer service life helps manufacturers plan production with greater confidence and reduces the disruption associated with frequent tooling changes.
Quality Control Considerations
Quality control begins with the product design and continues throughout manufacturing. Important control points include steel verification, component dimensions, cavity and core alignment, cooling channel integrity, runner performance, ejection movement, surface finish, and trial part inspection.
The mould should be examined for potential flash areas, particularly around the rim, handle interfaces, parting line, and other joining surfaces. Flash can affect product appearance, user comfort, stacking, and safety. Accurate fitting and consistent mould clamping help reduce this risk.
Product dimensions should be checked after the mould has reached stable operating conditions. Plastic shrinkage is influenced by material grade, mould temperature, injection pressure, holding pressure, cooling time, and ambient conditions. Multiple samples may be required to confirm repeatability.
Handle areas deserve special attention. The connection must be free from cracks, incomplete filling, or excessive weld-line weakness. If the handle is integrated into the main moulded body, its geometry and cooling must be evaluated together with the container wall.
Surface quality should be reviewed under suitable lighting. Polished products should have a consistent appearance, while matte products should show a uniform texture without unexpected gloss variation. The final acceptance criteria can be agreed upon before production begins.
Maintenance and Service Life
Even a well-designed mould requires regular care. Maintenance practices should include cleaning product residue, checking cooling channels, inspecting the runner system, lubricating moving components where appropriate, and monitoring ejector and guide systems.
Operators should avoid using unsuitable tools that could scratch polished surfaces or damage parting edges. When the mould is removed from the machine, it should be cleaned, protected against corrosion where necessary, and stored in a controlled environment.
Cooling performance should be monitored over time. Deposits or restricted flow can reduce heat transfer and lead to longer cycles or inconsistent products. Regular inspection of water connections and channels helps preserve the intended thermal performance.
Wear should be identified before it becomes a major production problem. Early signs may include increasing flash, difficult ejection, dimensional changes, unusual noise, or visible damage on the product. Prompt corrective action can extend mould life and reduce the risk of unplanned downtime.
The stated service life of up to 700,000 shots is influenced by many factors. Mould steel, resin additives, processing pressure, cycle frequency, maintenance, clamping accuracy, and operator practices all affect actual performance. Proper maintenance is therefore an essential part of achieving the expected return from the tooling investment.
Customization Process for New Basin and Bucket Designs
Customers can begin customization by providing a product drawing, three-dimensional file, sample, sketch, or detailed functional description. Useful information includes overall dimensions, capacity, wall thickness, handle style, material preference, surface finish, annual quantity, and target injection machine.
The design team then reviews the concept for mouldability. This review may identify areas that require draft angles, stronger transitions, modified wall thickness, revised parting lines, or improved ejection access. Such recommendations are intended to make the product easier to manufacture and more reliable in service.
Basin size can be modified for different applications. A compact basin may be designed for bathrooms or apartments, while a larger model may be intended for laundry or commercial cleaning. Bucket height, opening diameter, bottom shape, and carrying capacity can be adjusted according to market demand.
Handle design can also be customized. Options may include a simple reinforced grip, a curved carrying handle, a broader ergonomic profile, or a design adapted for stacking and storage. The handle must be reviewed for both user comfort and moulding feasibility.
Cavity configuration can be selected according to output requirements. A single-cavity tool may be preferred for a large or complex basin. Two cavities may be suitable where product dimensions and machine capacity permit balanced filling and cooling.
Before final approval, the customer and mould maker should confirm the product design, steel grade, runner system, surface finish, cavity count, mould life target, delivery schedule, and acceptance criteria. Clear confirmation at this stage helps prevent misunderstandings during manufacturing.
Why Choose a Specialized Plastic Mould Maker
A specialized plastic mould maker understands that the mould and the injection-moulded product must be developed together. The tool cannot be separated from the selected resin, machine, production volume, and user requirements.
Experienced moulding manufacturers can anticipate issues such as shrinkage, cooling imbalance, trapped air, handle weakness, difficult demoulding, and surface inconsistency. Addressing these issues during design is generally more efficient than correcting them after mass production has started.
A specialized supplier can also provide better coordination between design and manufacturing. The same technical understanding is carried through from the initial product review to mould assembly and trial production. This continuity supports faster decisions and more practical solutions.
For international customers, a supplier that provides integrated services can simplify communication. Design clarification, tooling progress, testing feedback, shipping preparation, and after-sales support can be coordinated through one experienced partner.
Environmental and Sustainable Production Considerations
Sustainable production begins with efficient use of materials and long-lasting tooling. Balanced wall thickness can help avoid unnecessary plastic consumption while maintaining suitable product strength. Stable moulding can also reduce scrap caused by deformation, incomplete filling, or surface defects.
Runner selection may influence material efficiency. In suitable high-volume applications, a hot runner can reduce runner waste. However, the best solution depends on the specific product and production plan. A carefully selected cold runner may remain practical where simplicity and maintenance convenience are priorities.
Long mould life supports a more sustainable tooling strategy by reducing the frequency of mould replacement and the resources used for manufacturing new tools. Proper maintenance extends this benefit and helps maintain production consistency over time.
PP and PE products can be selected according to application requirements, and manufacturers should consider responsible material sourcing, production scrap management, and end-of-life handling as part of their broader sustainability planning.
Recommended Project Workflow
A successful project can follow a structured workflow. First, the customer defines the product function, market, dimensions, material, output, and appearance. Second, the mould maker reviews the design and recommends improvements for filling, cooling, ejection, and durability.
Third, three-dimensional mould design is prepared for customer confirmation. Fourth, steel and production components are selected according to the agreed specifications. Fifth, machining, polishing, assembly, and inspection are completed under controlled production management.
Sixth, the mould undergoes trial moulding. Test parts are evaluated for appearance, dimensions, handle integrity, wall balance, and demoulding. Seventh, any required corrections are completed. Finally, the mould is prepared for delivery together with the relevant technical information and after-sales support.
This workflow creates clear decision points and helps ensure that the final tooling reflects the customer’s actual production needs. It also reduces the likelihood of expensive changes after the mould has been completed.
Q&A
What products can be made with this mould?
The mould is suitable for household washing basins, cleaning buckets, bathroom water containers, and utility storage buckets. The design can be customized for other similar open plastic containers when the product geometry and moulding requirements are compatible.
Which materials are compatible with the mould?
The standard material options are polypropylene and polyethylene. The final resin grade should be selected according to the required stiffness, impact resistance, chemical resistance, appearance, flexibility, and operating environment.
Can the bucket handle be integrated into the mould?
Yes. Handle integration can be included directly in the mould design. The handle shape, connection structure, position, and reinforcement can be reviewed according to the product concept and expected load.
What steel options are available?
P20 and H13 are available. P20 is a practical choice for many general-purpose moulds, while H13 may be selected for more demanding thermal and durability requirements. The appropriate grade depends on production conditions and the expected service life.
How many cavities can the mould have?
The mould can be configured with one or two cavities. The correct configuration depends on product dimensions, machine capacity, annual output, filling balance, cooling requirements, and project budget.
Is a hot runner or cold runner system better?
Neither system is universally better. A hot runner may reduce runner waste and support efficient high-volume production, while a cold runner may provide a simpler and economical solution for other projects. The choice should be based on the complete production plan.
What surface finishes are available?
The mould can provide polished or matte product surfaces. The preferred finish depends on the desired appearance, tactile effect, cleaning requirements, product positioning, and customer specifications.
What mould life can be expected?
The specified mould life is up to 700,000 shots under suitable operating and maintenance conditions. Actual performance depends on steel selection, resin, processing parameters, cycle frequency, mould care, and product design.
How does the mould help prevent basin or bucket deformation?
The design supports balanced wall thickness and an optimized cooling system. These features help reduce uneven shrinkage and thermal imbalance. Final results also depend on the selected material, injection parameters, mould temperature, holding pressure, and cooling time.
Can the mould be made for a special basin size?
Yes. Basin size, bucket capacity, wall dimensions, handle design, cavity configuration, and surface finish can be customized according to the customer’s product requirements.
What information should a customer provide before requesting a quotation?
Useful information includes product drawings or samples, three-dimensional files if available, dimensions, material, capacity, handle requirements, surface finish, expected annual quantity, injection machine details, cavity preference, and target delivery schedule.
Does the supplier provide support after mould delivery?
Haiquan provides integrated services from design and production to after-sales support. The exact scope of technical assistance can be confirmed during the project quotation and order process.
Conclusion
The Household Plastic Basin and Bucket Injection Mould is a practical tooling solution for manufacturers producing reliable daily necessities. Its design addresses the main challenges associated with large open plastic containers, including rim strength, wall balance, handle integration, surface quality, cooling stability, and repeated production use.
Compatibility with PP and PE, P20 or H13 steel options, hot or cold runner systems, one- or two-cavity configurations, and polished or matte finishes gives customers the flexibility to create products for different markets and applications. The target mould life of up to 700,000 shots further supports long-term production planning when the tool is properly operated and maintained.
The product’s principal advantage is the combination of functional design and manufacturing discipline. Rather than treating the mould as a simple cavity, the development process considers product use, material behavior, filling, cooling, ejection, surface finish, maintenance, and production efficiency as connected factors.
With expertise in daily necessities moulds and other precision injection tooling, Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. provides design, manufacturing, testing, delivery, and after-sales support for customers seeking dependable plastic moulding solutions. For basin and bucket manufacturers, this integrated approach can help improve product consistency, reduce production risk, and build a stronger foundation for long-term market supply.
References
1. Injection Moulding Handbook, general principles of thermoplastic injection mould design and processing.
2. Plastics Engineering Fundamentals, guidance on polypropylene, polyethylene, shrinkage, cooling, and part design.
3. Mould Steel Selection Principles, comparative considerations for P20 and H13 tooling steels.
4. Industrial Cooling System Design, practices for thermal control in large injection moulds.
5. Product Design for Injection Moulding, recommendations for wall thickness, draft, ejection, ribs, rims, and handles.
6. General Quality Management Practices for Precision Tooling Manufacturing.
Product: Household Plastic Basin and Bucket Injection Mould

For exclusive deals and latest offers, sign up by entering your email address below.











 +86-18657672567
 sales@tzhqmould.com
celin@tzhqmould.com
 No. 17 Houshi Road, Beicheng Industrial Zone, Huangyan District, Taizhou City, Zhejiang Province, China
Copyright © Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. All Rights Reserved
Injection Plastic Mould Maker

