

Household Plastic Basin and Bucket Injection Mould: Design, Manufacturing, and Performance Guide
Admin 2026-09-04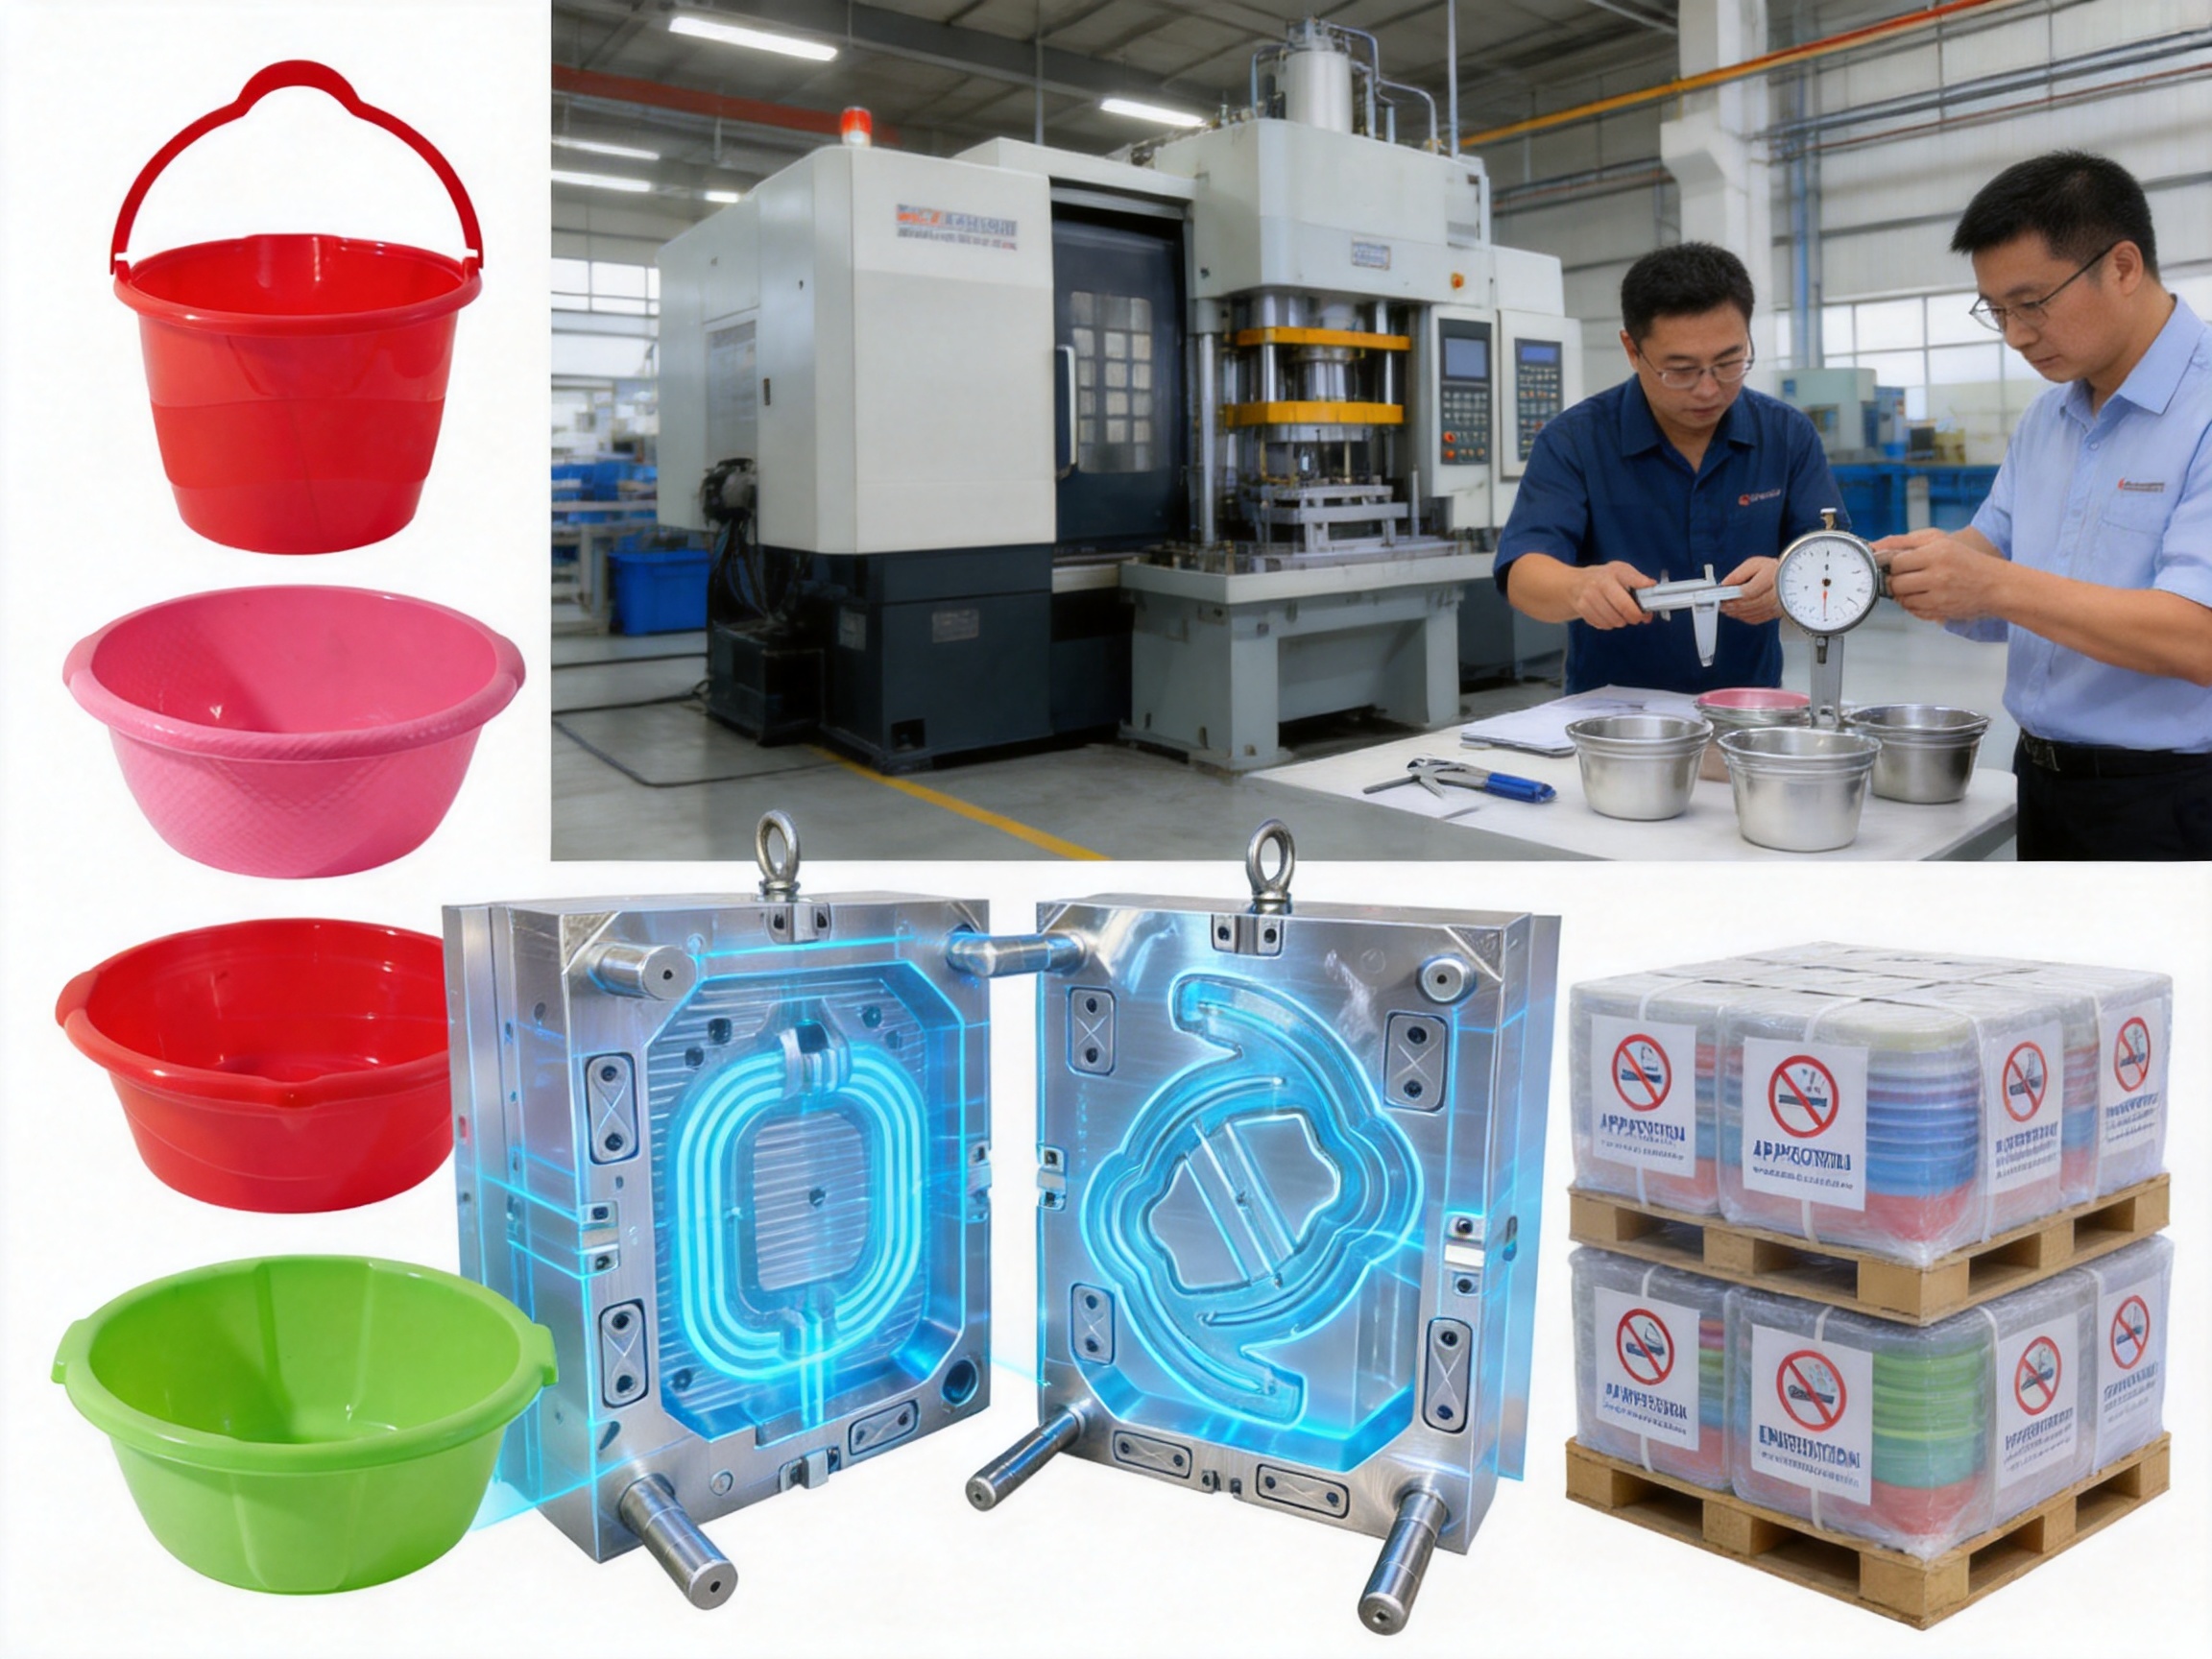
Household basins and buckets are among the most frequently used plastic products in homes, commercial cleaning environments, bathrooms, laundries, hotels, and utility areas. Although these products may appear simple, producing them consistently requires a carefully engineered injection mould. A basin or bucket must combine a low material weight with sufficient rigidity, a smooth and attractive surface, reliable dimensional accuracy, and enough impact resistance for repeated daily use. The mould must also support stable production cycles, efficient cooling, dependable ejection, and practical maintenance.
The Household Plastic Basin and Bucket Injection Mould developed by Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. is designed specifically for these requirements. It supports the production of washing basins, cleaning buckets, bathroom water containers, and utility storage buckets made from commonly used materials such as polypropylene and polyethylene. Its structure emphasizes strong rim design, balanced wall thickness, integrated handle options, smooth product surfaces, and optimized cooling for large plastic parts.
As a professional plastic mould manufacturing company, Haiquan combines product design analysis, mould engineering, precision machining, assembly, testing, and after-sales support. This integrated approach enables the manufacturer to control quality throughout the complete production process rather than treating mould construction as a series of disconnected operations. The result is tooling intended to deliver stable output, attractive finished products, and long service life in demanding production environments.

Household Plastic Basin and Bucket Injection Mould
Understanding the Household Basin and Bucket Mould
A plastic basin and bucket injection mould is a precision tool used to form molten thermoplastic material into a defined household product shape. During the injection process, plastic is heated until it reaches a suitable flow condition and is then forced into the mould cavity under pressure. The cavity creates the external and internal geometry of the basin or bucket, while the core forms the inner surface and maintains the required product thickness.
Unlike small injection-moulded components, basins and buckets generally have relatively large projected areas and broad surfaces. These characteristics create special engineering challenges. The mould must allow plastic to flow evenly across the entire part, prevent excessive shrinkage variation, remove heat efficiently, and eject the finished item without distortion. If any of these functions is poorly designed, the final product may show warpage, sink marks, uneven walls, weld lines, short shots, flash, or difficulty during demoulding.
The mould described in this article is intended for household products that require a balance between practical performance and economical mass production. It can be configured for one or two cavities, depending on product size, machine capacity, cycle-time objectives, and customer output requirements. The available runner options include hot runner and cold runner systems, allowing the tooling configuration to be matched to the production strategy.
Product Forms Supported by the Mould
The mould can be customized for different basin and bucket geometries. A shallow washing basin may require a wide opening, reinforced rim, and comfortable carrying edges. A cleaning bucket may require a deeper body, a stronger handle connection, and greater resistance to impact when filled with water. Bathroom water containers may prioritize smooth internal surfaces and compact dimensions, while utility storage buckets may require additional capacity and reinforced structural areas.
Although these products share a similar manufacturing principle, each design must be evaluated individually. The sidewall angle, base structure, rim profile, handle position, draft angle, corner radius, and material distribution all affect mould performance. Haiquan’s design team can modify basin size, handle design, and cavity configuration according to customer requirements.
Key Design Advantages
The value of an injection mould is determined not only by the appearance of the tooling but also by its ability to produce consistent parts over a long period. The Household Plastic Basin and Bucket Injection Mould focuses on several design advantages that directly influence product quality, manufacturing efficiency, and operating cost.
Strong Rim Structures
The rim is one of the most important structural features of a basin or bucket. It defines the opening, affects the product’s resistance to deformation, and influences how the user grips or carries the item. A weak or uneven rim can bend easily, lose its shape, or create an uncomfortable edge. It may also make the product appear low quality even when the main body is correctly formed.
The mould design supports a strong and stable rim structure. Appropriate rim thickness and transitions help distribute mechanical loads around the opening. Reinforced rim geometry can improve resistance to bending when a bucket is lifted while full or when a basin is moved with water and cleaning materials inside. It also contributes to dimensional stability during cooling.
From a moulding perspective, the rim must be designed with suitable filling and cooling conditions. Excessive thickness can cause sink marks or extended cooling time, while insufficient thickness can reduce strength. A balanced structure allows the product to maintain a practical weight while still providing a firm edge. This balance is particularly valuable for manufacturers that need to control resin consumption without sacrificing durability.
Balanced Wall Thickness
Large household plastic products are sensitive to uneven wall thickness. When one region cools and shrinks more quickly than another, internal stresses can develop. These stresses may cause warpage, twisting, deformation, or dimensional inconsistency. A basin that does not sit flat or a bucket with a distorted opening may be rejected by customers and retailers.
The mould is designed to support balanced wall distribution across the main product body. This design objective helps reduce localized shrinkage and encourages more uniform cooling. It also improves the visual quality of broad surfaces, where uneven thickness can create visible depressions or gloss differences.
Balanced thickness does not mean that every section must have exactly the same dimension. Practical products often need thicker reinforcement at the base, rim, handle attachment, or corner areas. The goal is to apply material where it contributes to strength while avoiding unnecessary mass in areas that do not need reinforcement. This approach helps maintain a useful relationship between product weight, stiffness, cycle time, and material cost.
Integrated Handle Options
Many buckets require a handle for carrying water, cleaning solutions, laundry, or other household materials. A handle can be installed after moulding, but direct integration into the product design often creates a cleaner appearance and can improve assembly efficiency. The mould can be adapted to support handle-related features, including reinforced attachment areas and suitable connection geometry.
Handle integration requires careful consideration of load transfer. The attachment region must resist repeated pulling forces, impact, and twisting. If the handle connection is too thin or the surrounding wall is poorly supported, the product may crack or deform during use. By incorporating the handle requirements into the mould design, the manufacturer can coordinate the attachment structure with the bucket wall, rim, and overall product shape.
Customers may request different handle styles, attachment positions, grip shapes, or handle-related reinforcement. The customization capability of the mould allows the tooling to be adjusted for various market preferences and product applications.
Smooth and Cleanable Product Surfaces
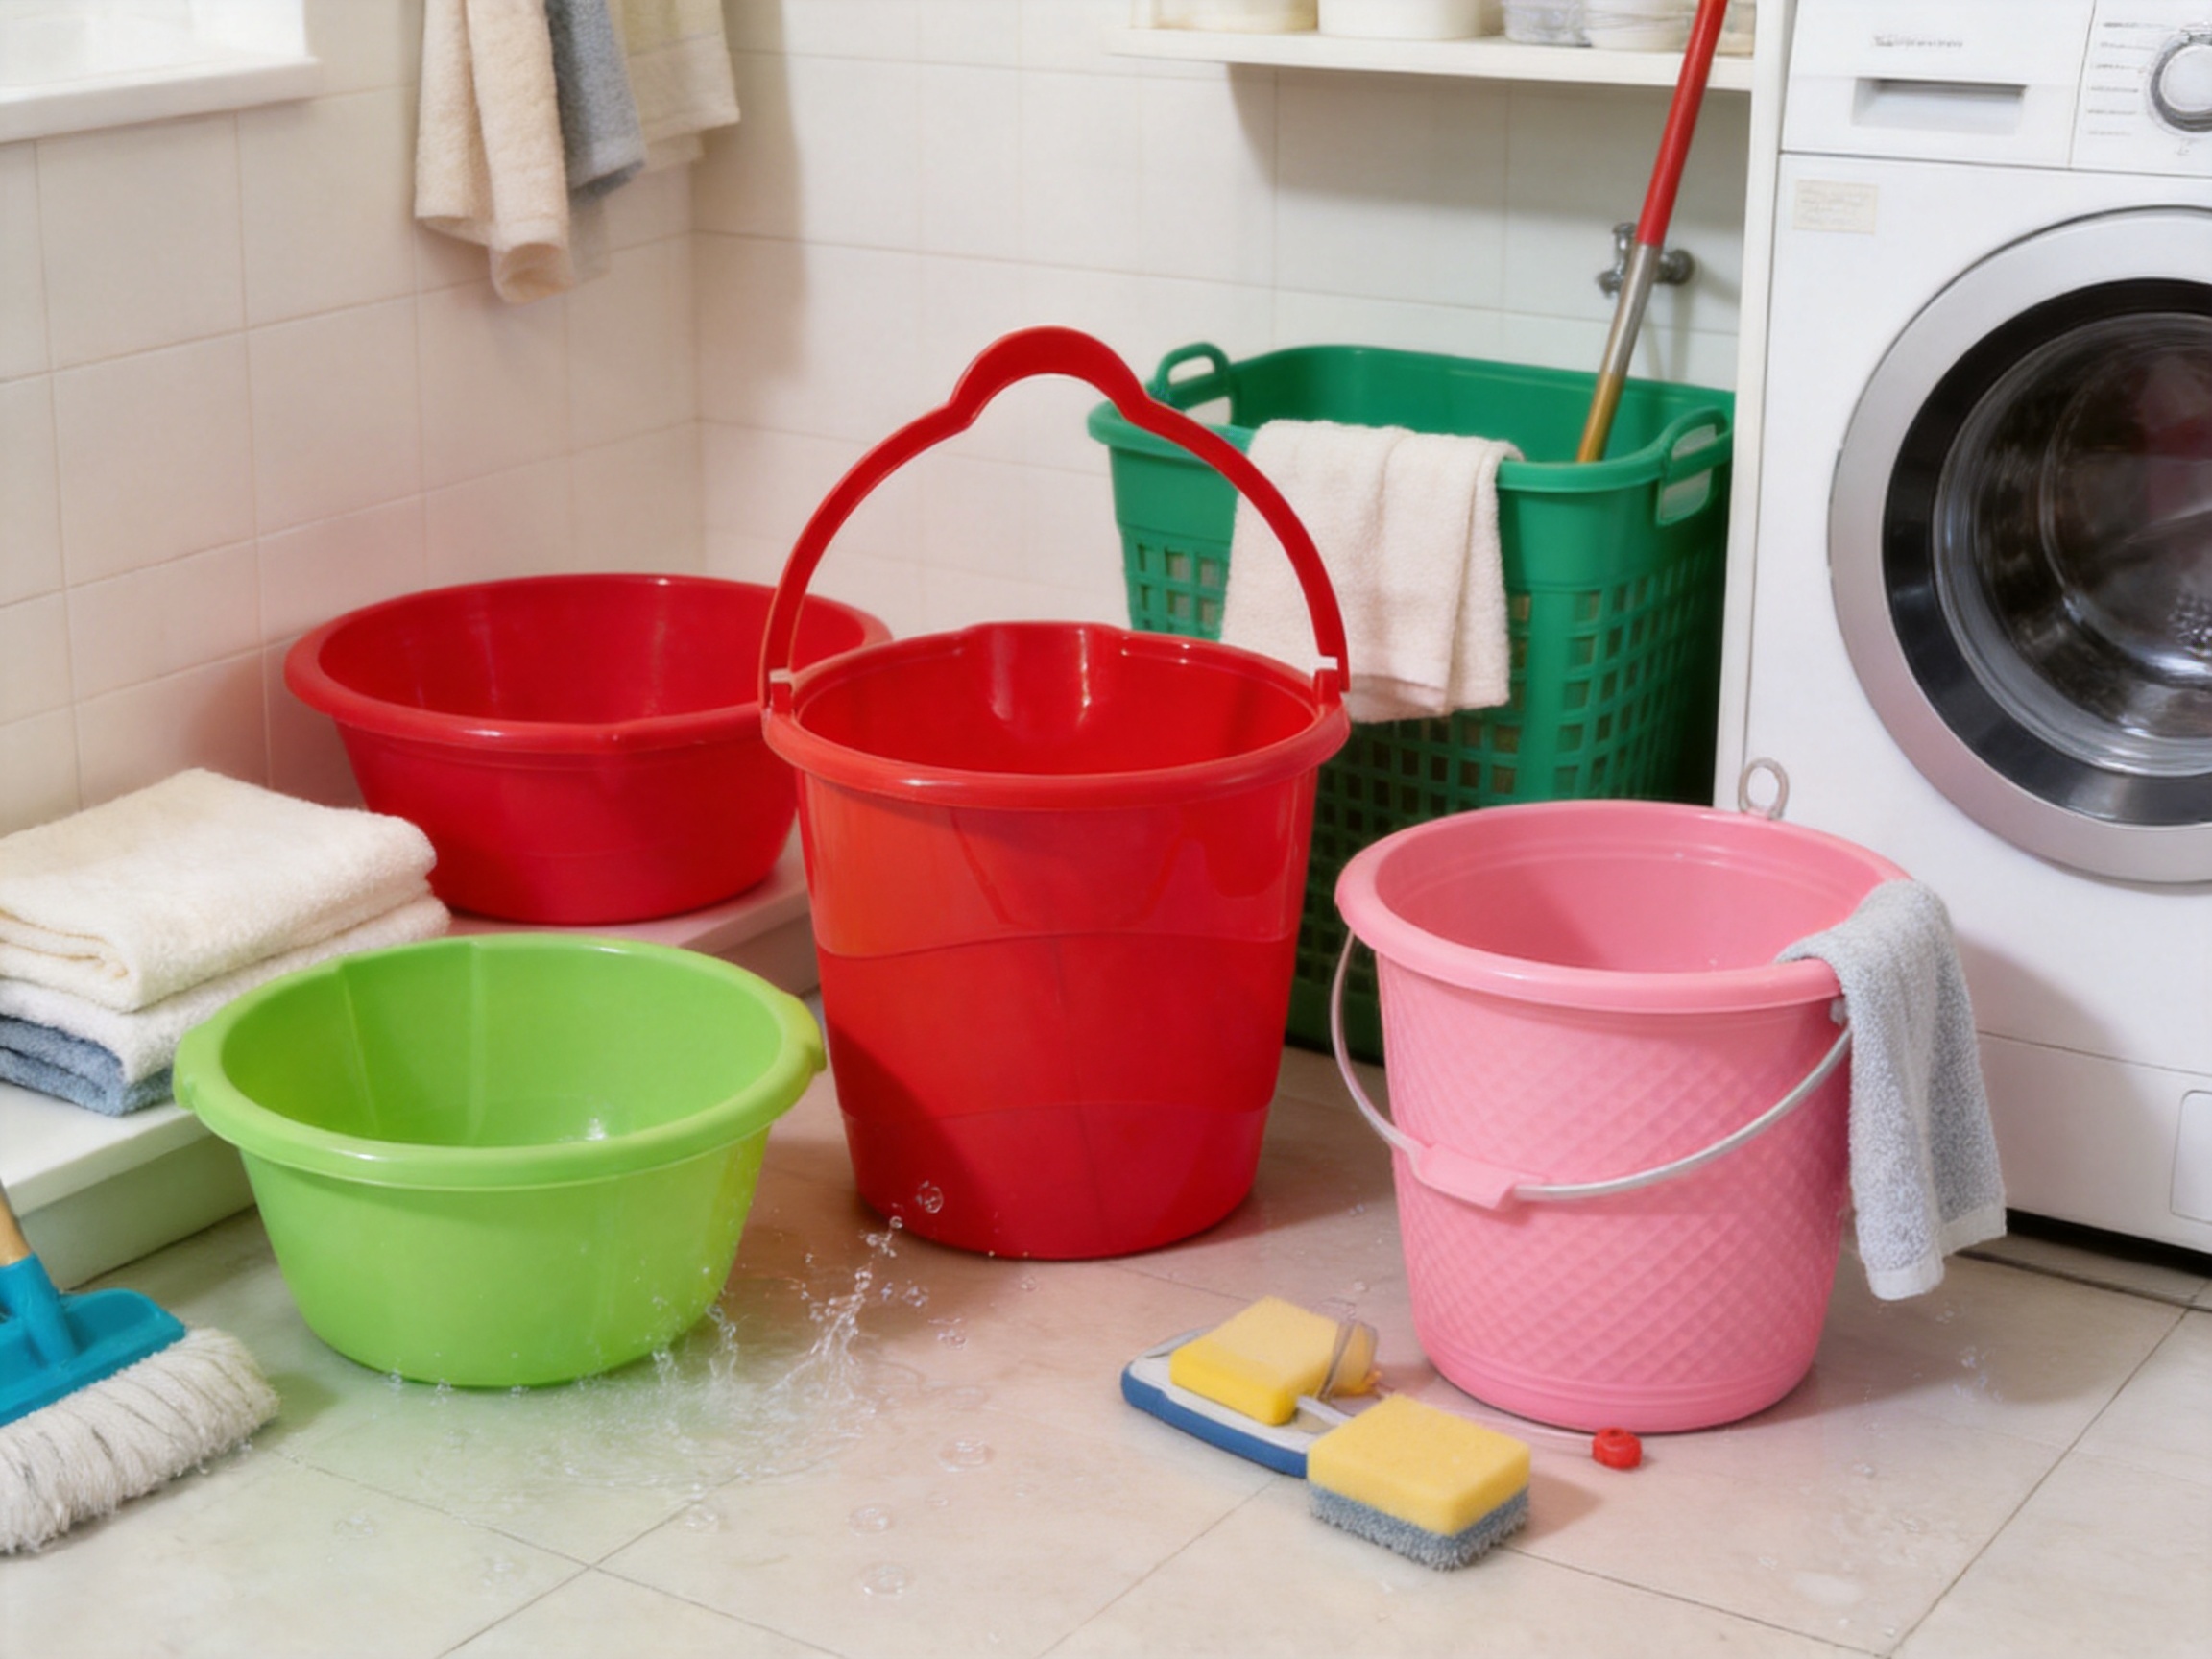
Household basins and buckets are exposed to water, detergents, soap, dirt, and a wide range of cleaning products. Smooth surfaces are therefore highly desirable. They are easier to wash, less likely to retain residue, and more resistant to the visible accumulation of stains. A high-quality mould surface also contributes to a more attractive finished product.
The mould can be supplied with a polished or matte surface finish. A polished finish may be selected for products that require a smooth, reflective, or premium appearance. A matte finish can provide a softer visual effect, reduce the visibility of minor handling marks, and support a practical non-gloss appearance. The appropriate finish depends on the product design, brand positioning, resin behavior, and customer expectations.
Surface finishing is not merely a cosmetic step. It influences release behavior, product cleaning performance, visual uniformity, and the way light reflects from large surfaces. For this reason, mould finishing must be carried out with attention to the product’s intended use and the selected plastic material.
Material Compatibility and Product Performance
The mould is designed for common household product materials including polypropylene and polyethylene. Both materials are widely used in injection moulding, but they have different processing characteristics and product performance profiles.
Polypropylene
Polypropylene, commonly known as PP, is widely selected for basins and buckets because it offers a useful combination of low density, chemical resistance, rigidity, and affordability. It can provide a lightweight product that remains sufficiently strong for routine household use. PP is also available in a broad range of colors and can be modified with additives or impact-enhancing formulations depending on the application.
When moulding polypropylene, the filling pattern, cooling balance, shrinkage behavior, and ejection conditions must be considered. A well-designed mould helps manage these factors by supporting stable material flow and uniform heat removal. The final product can be designed with a crisp rim, stable base, smooth sidewalls, and practical handle reinforcement.
Polyethylene
Polyethylene, or PE, is valued for toughness, flexibility, and resistance to many household chemicals. Depending on the specific grade, it can be suitable for products that require impact resistance and a degree of flexibility. PE may be selected for buckets or containers that are expected to withstand rough handling, repeated movement, or occasional impact.
Because PE grades can display different shrinkage and flow characteristics, the moulding process must be adjusted to the selected resin. Gate location, cooling design, draft angles, and ejection force all influence the quality of the finished item. The mould can be engineered around the customer’s material grade and processing conditions to support reliable production.
Material Selection and Mould Design
Material selection should be completed before finalizing mould details. The resin affects shrinkage allowances, cooling time, surface appearance, product flexibility, and dimensional stability. A mould intended for a rigid PP basin may require different considerations from a mould intended for a more flexible PE bucket.
Haiquan’s engineering process takes the intended product, material, cavity arrangement, and production requirements into account. This allows the mould to be designed as a complete system rather than simply as a negative shape of the product. The objective is to create tooling that works effectively with the selected machine, resin, and production method.
Runner System Options
The Household Plastic Basin and Bucket Injection Mould can be configured with either a hot runner or cold runner system. The choice depends on project volume, product design, machine configuration, resin usage, maintenance preferences, and investment considerations.
Hot Runner System
A hot runner system keeps the material in a heated flow path until it reaches the gates. This can reduce runner waste and support a more automated production process. For high-volume production, the reduction of discarded runner material may contribute to lower material consumption and improved cycle efficiency.
Hot runner systems can also provide greater control over gate placement and filling for large products. When properly balanced, they may support more uniform filling across a broad basin or bucket surface. However, hot runner tooling requires careful temperature control, reliable components, and appropriate maintenance procedures.
Cold Runner System
A cold runner system uses solidified runners that are removed with the moulded product or separated during subsequent handling. It is often simpler to operate and may be suitable for manufacturers that prioritize straightforward maintenance and lower initial tooling complexity.
Cold runner systems can be an economical choice for certain production volumes, product sizes, and material grades. They may also provide flexibility during early product development or for businesses that already have established cold runner injection equipment. The final selection should consider the complete operating cost rather than only the initial mould price.
Matching the Runner to Production Requirements
There is no single runner configuration that is ideal for every basin and bucket project. A high-volume program with a stable product design may benefit from hot runner efficiency. A lower-volume or highly flexible production program may prefer the simplicity of a cold runner. Haiquan can evaluate the customer’s product and production objectives before recommending a suitable configuration.
Cavity Configuration and Productivity
The mould is available with one or two cavities. Cavity selection affects output, mould size, injection machine requirements, cooling balance, and overall investment. A single-cavity mould may be appropriate for a large product, a specialized design, or a production program with moderate volume. It can also simplify initial development and allow focused control over one product format.
A two-cavity mould can increase output by producing two parts in each injection cycle. This may improve productivity when the machine has sufficient injection capacity and clamping force. However, the two cavities must be balanced carefully so that both products fill, cool, and eject consistently. An unbalanced multi-cavity system can create variation between parts and reduce the expected productivity benefit.
For basins and buckets, cavity configuration must also account for the product’s projected area and the available factory equipment. Large products require considerable clamping force, and the mould must be compatible with the customer’s injection machine. Proper cavity planning helps avoid excessive machine loading and supports predictable production cycles.
Cooling System for Large Plastic Parts
Cooling is one of the most critical functions of a large injection mould. After molten plastic enters the cavity, it must release heat and solidify sufficiently before the product can be ejected. If cooling is too slow, cycle time increases. If cooling is uneven, the product may warp, shrink unevenly, or lose its intended shape.
The mould’s cooling system is optimized for large plastic parts. Cooling channels are planned to remove heat from important regions such as the base, sidewalls, rim, corners, and handle attachment areas. The design objective is not simply to maximize water flow but to achieve a balanced temperature distribution throughout the mould.
Good cooling design supports several advantages:
- More stable product dimensions.
- Reduced risk of warpage and deformation.
- Shorter and more predictable moulding cycles.
- Improved surface quality.
- More consistent production between different operating shifts.
- Lower risk of premature mould stress caused by thermal imbalance.
Large household products often have broad surfaces that are difficult to cool uniformly. The cooling system must therefore be considered together with wall thickness, gate location, material selection, and mould structure. A production-oriented design can help manufacturers achieve a better balance between cycle time and product quality.
Precision Manufacturing Process
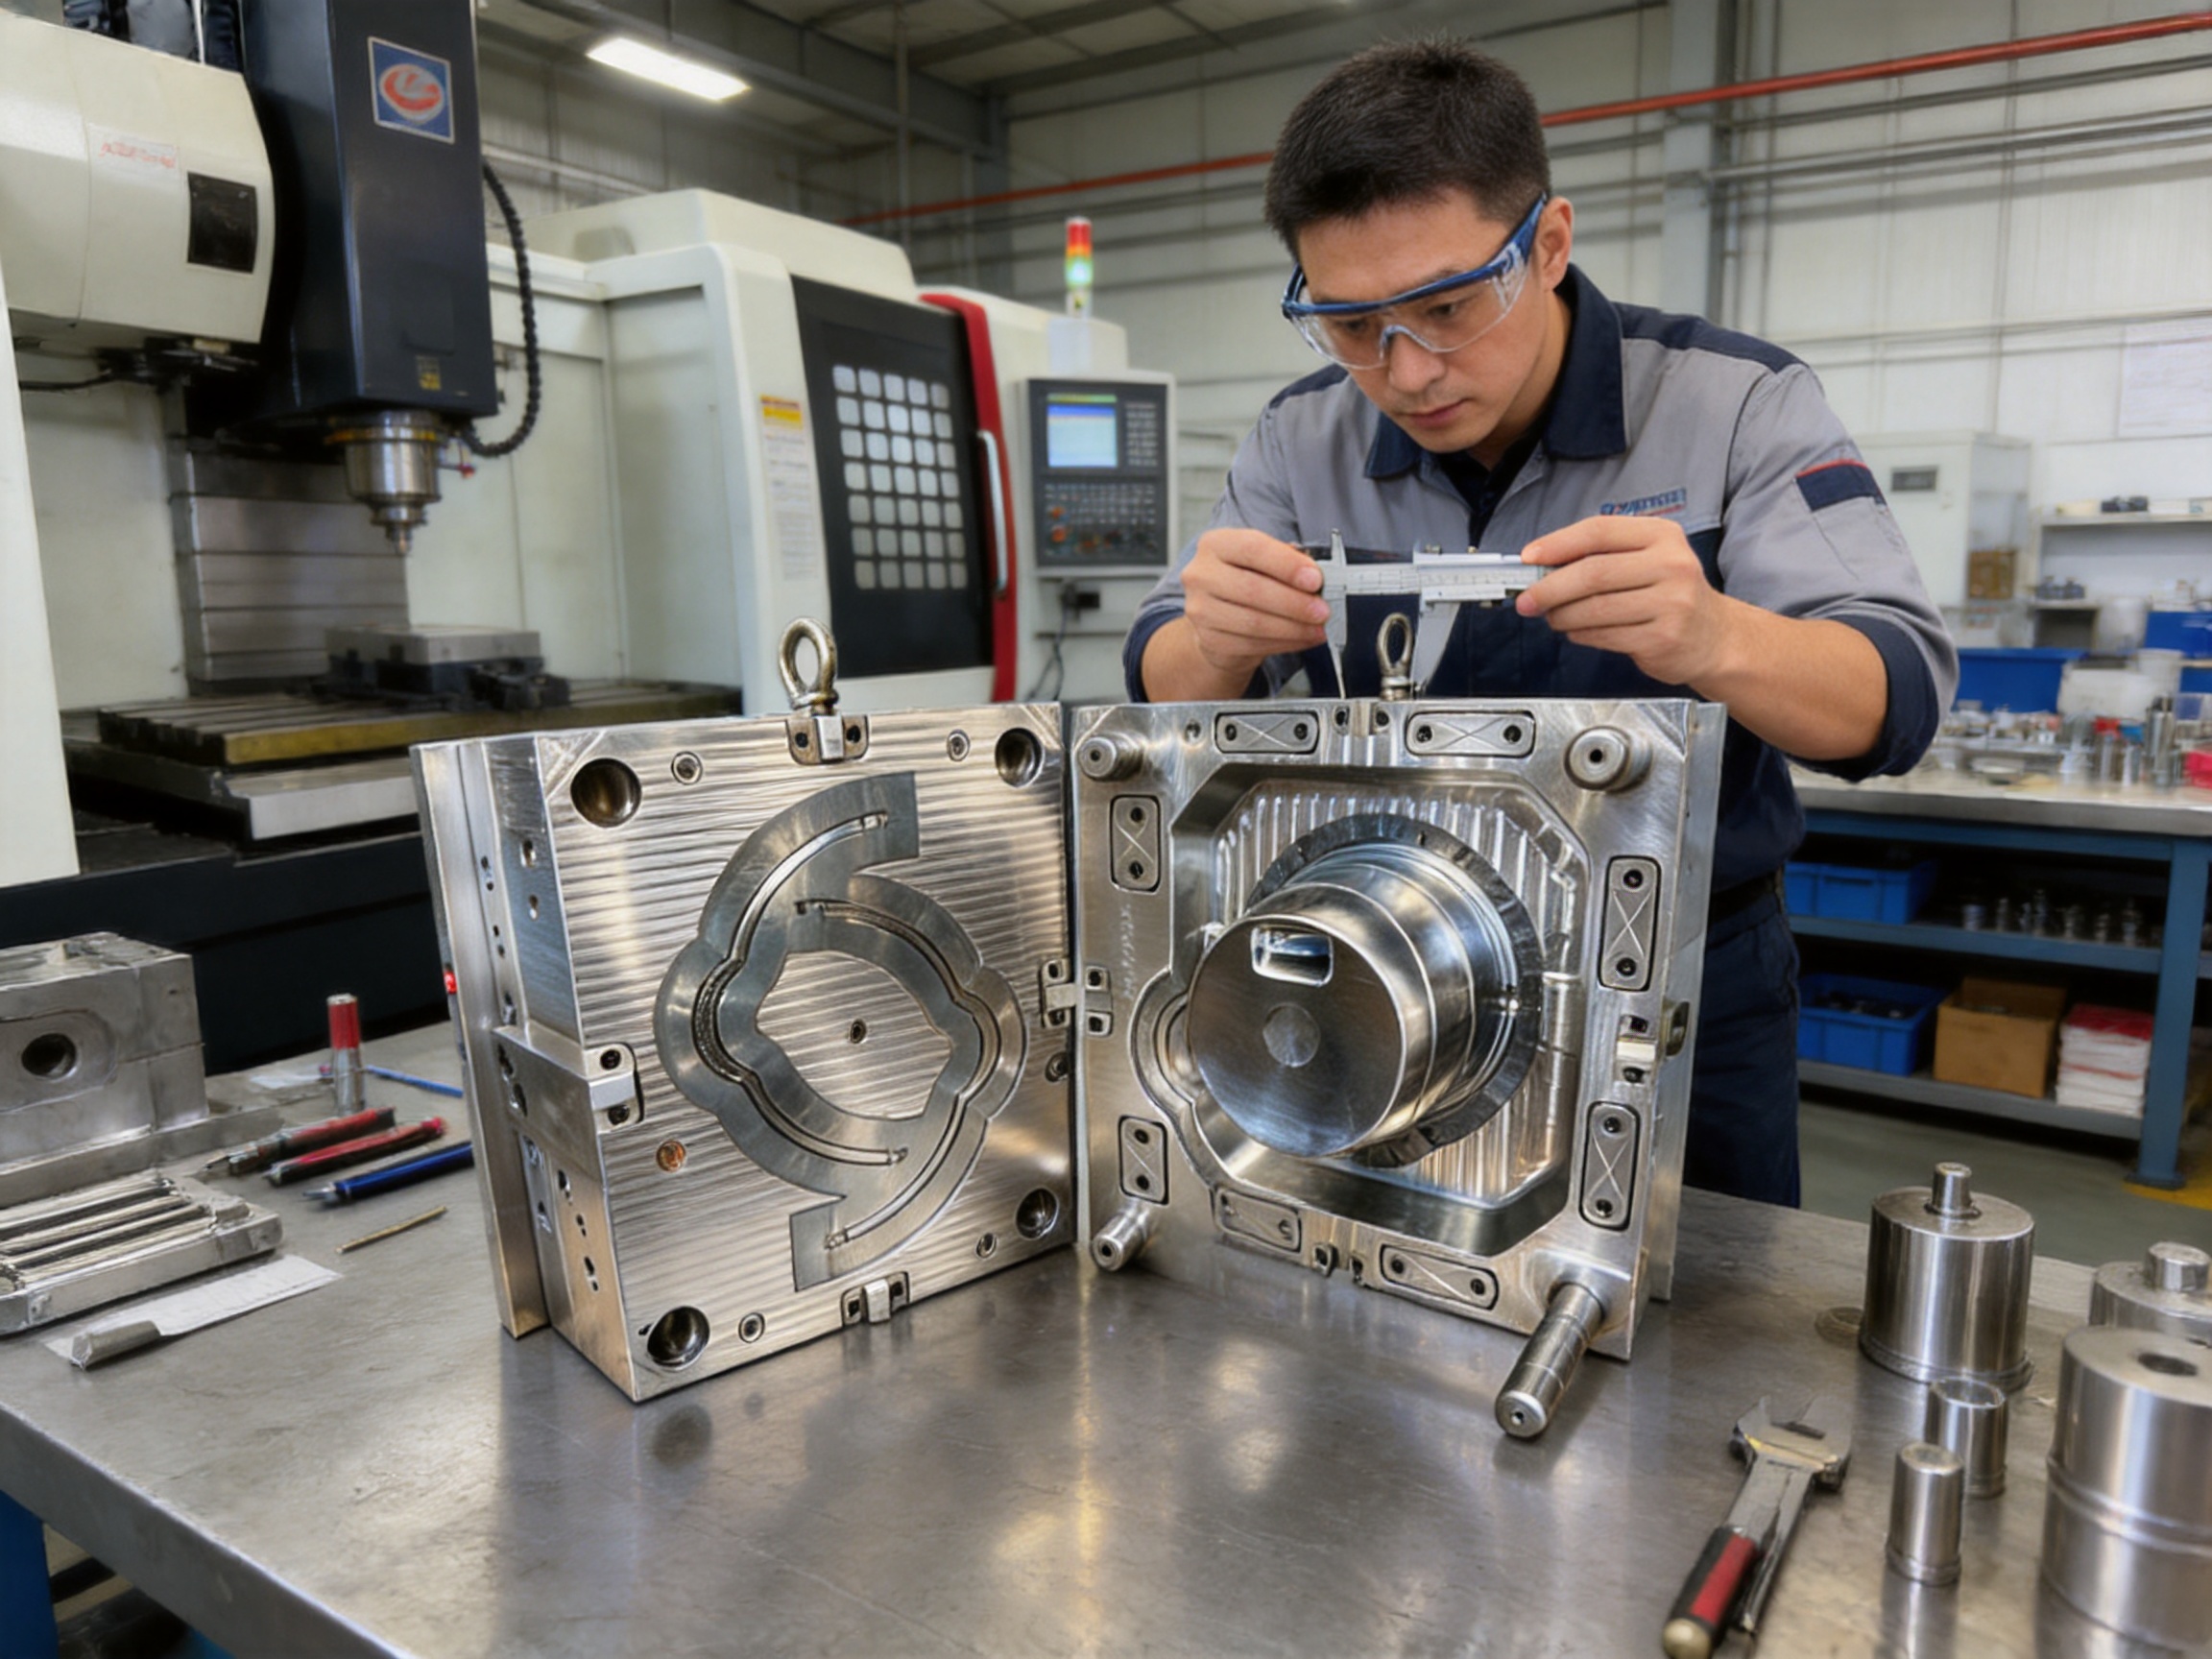
The performance of a basin and bucket mould depends heavily on how it is manufactured. Accurate design information must be transferred into steel with tight control over dimensions, surface condition, alignment, and moving components. Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. uses an integrated manufacturing process covering engineering preparation, steel selection, machining, fitting, assembly, testing, and delivery.
Product and Mould Design Analysis
The process begins with an evaluation of the customer’s product requirements. Product geometry, material, dimensions, handle structure, surface finish, expected production volume, and injection machine conditions are reviewed. The design team considers draft angles, wall thickness, corner transitions, parting lines, gate position, ejection method, and cooling requirements.
Design analysis is particularly important for large household products because small geometry problems can become visible across a broad surface. The engineering team must identify areas that may trap air, create weld lines, generate excessive stress, or make demoulding difficult. Early attention to these details reduces the risk of expensive modifications after machining has begun.
Steel Selection
The standard material options for the mould include P20 and H13 steel. P20 is commonly used for injection mould components because it offers a practical combination of machinability, strength, and cost. It can be suitable for many general-purpose household product applications when the required production conditions are properly defined.
H13 is a hot-work tool steel known for high strength and good resistance to thermal fatigue. It may be selected for applications requiring enhanced durability or more demanding operating conditions. The appropriate steel grade depends on projected production volume, resin characteristics, moulding temperature, surface requirements, and customer expectations.
Steel selection is a long-term investment decision. A mould with a projected life of approximately 700,000 shots must be designed and built with sufficient structural integrity, wear resistance, and maintenance accessibility. Selecting a suitable steel grade helps protect product consistency over the expected service period.
CNC Machining and Precision Cutting
After design approval and material preparation, the mould components are machined according to the engineering data. CNC machining is used to produce accurate cavity and core surfaces, parting areas, mounting structures, cooling features, and mechanical interfaces. Precision cutting and controlled machining reduce dimensional variation between components.
For a basin or bucket mould, machining accuracy is important on both visible product surfaces and internal mould interfaces. The cavity and core must align correctly to maintain wall thickness and prevent flash. The parting surface must close properly, while the ejector and guide systems must move smoothly without damaging the mould or product.
Electrodischarge Machining and Detail Work
Some mould features may require additional precision processes for complex details, sharp transitions, deep areas, or difficult-to-machine geometry. Electrodischarge machining and related finishing operations can be used where conventional cutting tools cannot achieve the required result efficiently.
Detail work may include handle attachment structures, reinforcement patterns, narrow corners, gate areas, or specialized surface features. Every detail must be checked for proper release and suitable draft. The purpose is to create a mould that reproduces the intended product design without introducing unnecessary manufacturing difficulty.
Polishing and Surface Treatment
Polishing is carried out according to the requested product appearance. A polished cavity requires consistent treatment across broad surfaces to prevent visible differences in gloss. Matte finishes require controlled texturing or surface treatment so that the final product has a uniform appearance.
Surface treatment must also consider release performance. Excessively rough or inconsistent regions can increase ejection resistance and leave unwanted marks on the plastic product. A properly finished mould surface supports a cleaner appearance and improves the repeatability of the production process.
Assembly and Fitting
After individual components are machined and finished, the mould is assembled and fitted. This stage includes the installation of guide pillars, guide bushes, ejector components, inserts, cooling connections, runner components, and other mould elements. Careful fitting ensures that the mould opens and closes accurately and that moving parts operate without abnormal friction.
Assembly quality is especially important for large moulds because their size and weight increase the forces acting on guide systems, parting surfaces, and ejector components. Proper alignment helps prevent uneven wear and protects the cavity and core from damage during repeated cycles.
Trial Moulding and Corrections
A trial moulding process is used to verify filling, cooling, ejection, product dimensions, surface quality, and overall mould operation. Sample products are inspected for short shots, flash, sink marks, weld lines, warpage, uneven color, and other potential defects.
If adjustments are required, the mould can be corrected through controlled modifications to gates, vents, cooling channels, ejection details, or surface areas. Trial production is an essential quality-control stage because it tests the mould under practical operating conditions rather than relying only on design calculations.
Manufacturing Strengths of the Supplier
Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. is a high-tech enterprise specializing in the research, development, and manufacturing of precision injection moulds. Its product coverage includes daily necessities, home appliances, automotive parts, and industrial equipment. This cross-sector experience gives the company exposure to a wide range of material behaviors, structural requirements, dimensional standards, and moulding challenges.
The company operates with a professional design team and a scientific production management system. These strengths support coordinated control from initial product design through mould production and after-sales service. Customers benefit from having design communication, technical evaluation, manufacturing, testing, and support handled within an integrated organization.
Experience Across Multiple Product Sectors
Daily necessity moulds often require efficient production and attractive surfaces, while automotive and industrial moulds may demand more complex structural analysis and tighter dimensional control. Experience across these categories helps the manufacturer apply disciplined engineering methods to household mould projects.
For a basin or bucket mould, this experience can be applied to areas such as structural reinforcement, cooling balance, moving component durability, parting-line control, and production stability. The result is a tooling approach that goes beyond basic shape replication.
Professional Design Capability
A strong design team can identify potential moulding risks before they become manufacturing problems. Product analysis may reveal that a handle attachment needs reinforcement, that the base requires a different cooling arrangement, or that a proposed parting line could create an unwanted mark. Early design review can reduce rework and help customers make informed decisions about product performance and cost.
The design team can also support customization. Basin dimensions, bucket depth, handle form, cavity number, surface finish, and runner system can be adapted to match different customer requirements. This flexibility is valuable for manufacturers serving multiple markets or developing several product sizes.
Scientific Production Management
Production management contributes directly to delivery reliability and mould quality. Organized scheduling, process control, component inspection, assembly records, and testing procedures help maintain consistency from one project to the next. A scientific management system also makes it easier to identify problems and implement corrective action.
Reliable delivery is particularly important for product manufacturers that plan launches, seasonal promotions, or capacity expansion around a specific mould completion date. Clear communication and structured production control can reduce uncertainty during the tooling project.
International Customer Service
Haiquan exports moulds to Europe, the Middle East, Southeast Asia, South America, and other international markets. This export experience means the company is familiar with communicating across different technical expectations, product standards, shipping arrangements, and production environments.
International customers may require specific mould base standards, machine compatibility, spare parts, documentation, packaging, or testing procedures. A supplier with export experience is better positioned to discuss these requirements during the quotation and design stages.
Advantages Over Basic or Low-Cost Competitor Tooling
When comparing mould suppliers, the lowest initial price does not always represent the lowest total cost. A low-cost mould may appear attractive at the quotation stage but create higher expenses through unstable cycles, excessive scrap, frequent maintenance, difficult part removal, and premature wear. The Household Plastic Basin and Bucket Injection Mould is intended to compete through engineering quality and production reliability rather than only through initial purchase price.
More Consistent Product Quality
Balanced wall thickness, controlled cooling, suitable draft, and accurate cavity alignment help produce parts with more stable dimensions. Consistency is important when products are packed, stacked, displayed, or used together in a product range. A basin with an uneven rim or bucket with a distorted base can cause customer complaints and reduce confidence in the product line.
Better Structural Durability
Reinforced rim structures and carefully designed handle areas contribute to better resistance against routine household loads. Competitor moulds that focus only on visual shape may fail to address the forces applied during lifting, carrying, stacking, and cleaning. A production mould should support the product’s actual use conditions, not simply its appearance.
Improved Material Efficiency
Balanced product thickness can reduce unnecessary material use while maintaining useful stiffness. When the mould is designed properly, manufacturers may avoid excessive wall thickness that adds weight and extends cooling time. Material savings can become significant over hundreds of thousands of production cycles.
Reduced Production Instability
Large plastic parts are vulnerable to variations in filling and cooling. An optimized runner and cooling design helps reduce the need for constant machine adjustments. More stable processing can improve production planning, reduce rejected parts, and simplify operator training.
Longer Service Life
With appropriate steel selection, accurate machining, careful fitting, and scheduled maintenance, the mould is designed for an expected life of approximately 700,000 shots. This service-life target supports long-term production planning and can reduce the need for frequent tooling replacement.
Customization Instead of a One-Design Solution
Some mould suppliers offer standard tooling with limited modification options. Haiquan can customize basin size, handle design, and cavity configuration. This allows customers to develop products for specific markets, capacities, user groups, and packaging requirements.
Application Areas
The mould supports a broad range of household and utility products. Its main application areas include washing basins, cleaning buckets, bathroom water containers, and utility storage buckets.
Household Washing Basins
Washing basins are used for laundry, hand washing, cleaning, soaking, and general household tasks. They require a stable base, a comfortable rim, sufficient sidewall stiffness, and a surface that is easy to clean. The mould can be adapted to create different widths, depths, shapes, and color options.
Cleaning Buckets
Cleaning buckets are used with mops, brushes, detergents, and water. They often need a durable handle structure and sufficient capacity for routine cleaning work. A strong rim and balanced body can help the bucket remain stable when filled and carried.
Bathroom Water Containers
Bathroom containers must be easy to rinse and resistant to the effects of frequent water exposure and household cleaning products. Smooth internal surfaces and practical proportions support convenient daily use. Depending on the product concept, the mould can be configured for compact containers or larger water-holding designs.
Utility Storage Buckets
Utility buckets may be used to store tools, garden materials, toys, accessories, dry goods, or cleaning supplies. They may require increased stiffness, stackability, reinforced edges, or a particular lid and handle arrangement. These features can be considered during customization and mould design.
Quality Control Considerations
Quality control should be applied throughout the entire mould project. Inspection begins with the design and material review and continues through steel preparation, machining, fitting, assembly, trial moulding, and final acceptance.
Dimensional inspection verifies that cavity and core components meet the approved design. Surface inspection checks polishing, texture, transitions, and visible product areas. Functional testing evaluates mould opening, closing, ejection, cooling connections, runner operation, and insert stability.
Trial parts should be reviewed for both appearance and practical performance. Important checks may include the overall dimensions, rim roundness, base flatness, handle attachment strength, wall uniformity, product weight, surface condition, and ease of demoulding. The exact inspection plan can be adapted to customer requirements and product specifications.
Maintenance and Service Life
Even a high-quality mould requires correct maintenance. Regular cleaning helps prevent residue from accumulating on the parting surface, cavity, core, vents, and cooling connections. Lubrication of suitable moving components helps reduce friction and wear. Operators should also inspect guide systems, ejector pins, screws, inserts, and water fittings according to an established schedule.
Cooling performance should be monitored during production. Deposits or restricted channels can reduce water flow and create thermal imbalance. If cycle time increases or product warpage changes over time, the cooling system should be inspected. Early maintenance can prevent more serious mould damage.
At the end of a production run, the mould should be cleaned, dried, protected against corrosion where appropriate, and stored in a safe position. Correct storage is particularly important for large moulds because improper support can place stress on the mould base or moving components.
A documented maintenance plan helps the customer approach the expected 700,000-shot service life. Actual life depends on steel grade, resin, processing conditions, production frequency, maintenance quality, and the amount of abrasive or chemically aggressive additives in the material.
Technical Specification Overview
| Product Type | Household plastic basin and bucket injection mould |
| Primary Category | Daily necessities mould |
| Compatible Product Materials | PP / PE |
| Mould Steel Options | P20 / H13 |
| Runner System | Hot runner or cold runner |
| Cavity Configuration | 1–2 cavities |
| Expected Mould Life | Approximately 700,000 shots |
| Surface Finish Options | Polished or matte |
| Customization Scope | Basin size, handle design, and cavity configuration |
| Main Applications | Washing basins, cleaning buckets, bathroom containers, and utility buckets |
How to Select the Correct Mould Configuration
Customers should define the product’s intended use before confirming the mould design. Important questions include the required capacity, product dimensions, resin grade, expected annual output, available injection machine, desired surface finish, handle requirements, and target product weight.
The basin or bucket size affects mould dimensions, machine requirements, cooling layout, and cavity count. The selected material affects shrinkage allowance and processing conditions. The output target influences whether one or two cavities are more appropriate. The surface finish affects cavity preparation and inspection requirements.
Customers should also consider how the finished products will be packed and transported. Stackability, nesting depth, rim strength, handle position, and product flexibility all influence logistics costs. A mould designed with these practical issues in mind can provide value beyond the injection machine itself.
Questions for the Design Review
- What are the final product length, width, height, and capacity?
- Will the product be made from PP, PE, or another resin?
- Does the product require an integrated or attached handle?
- What level of impact resistance is expected?
- Is a polished or matte surface preferred?
- What is the target production volume?
- What injection machine and clamping force are available?
- Would a hot runner or cold runner better suit the production plan?
- Are multiple sizes or interchangeable inserts required?
- What inspection and acceptance standards should be applied?
Providing complete information at the beginning of the project helps the manufacturer prepare a more accurate design and quotation. It also reduces the risk of later changes that could affect tooling cost, delivery time, or product performance.
Why Integrated Mould Manufacturing Matters
An integrated mould manufacturing company can coordinate the many technical decisions that influence final performance. Product design, mould flow, steel selection, machining, cooling, ejection, finishing, and trial production are closely connected. A change in one area may affect all the others.
For example, changing the product material may require an adjustment to shrinkage allowance, cooling conditions, and ejection design. Changing the handle shape may affect cavity layout, parting line location, and local reinforcement. Increasing production volume may justify a different runner system or cavity arrangement. Integrated engineering allows these relationships to be evaluated systematically.
Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. provides services from design and production to after-sales support. This complete service model can simplify communication for international customers and provide a clear technical contact throughout the mould project.
Environmental and Economic Considerations
Plastic household products must be manufactured economically while maintaining suitable service performance. Mould design has a direct influence on material use, cycle time, energy consumption, scrap rate, and tooling replacement frequency.
Balanced wall thickness can reduce unnecessary resin consumption. Efficient cooling can shorten cycles and reduce the energy required to maintain stable production. A reliable mould can reduce rejected parts and minimize material waste. A longer mould service life can also reduce the environmental and financial cost associated with making replacement tooling.
PP and PE are widely used thermoplastics with established recycling pathways in many markets. Manufacturers should follow local requirements for material selection, additives, product labeling, and recycling. The mould itself can support efficient production, but responsible environmental performance also depends on resin management, machine settings, product design, and end-of-life handling.
Customer Support and Global Supply
Haiquan serves customers in Europe, the Middle East, Southeast Asia, South America, and other international regions. Global supply requires attention to technical communication, packaging protection, shipping preparation, documentation, and installation support.
Before shipment, customers may require mould drawings, spare parts lists, operating instructions, trial samples, or inspection records. Clear documentation helps the receiving factory install and operate the mould correctly. It can also assist maintenance personnel when replacement parts or future technical support are needed.
After-sales support is an important part of mould value. A supplier that remains available after delivery can help address questions about mould installation, processing conditions, cooling connections, ejection, and maintenance. This support can reduce downtime and help customers achieve a faster production start.
Q&A: Household Plastic Basin and Bucket Injection Mould
Q1: What products can this mould produce?
The mould is intended for household washing basins, cleaning buckets, bathroom water containers, and utility storage buckets. The exact product shape, size, capacity, rim, base, and handle design can be customized.
Q2: Which plastic materials are supported?
The standard material options are polypropylene and polyethylene. The final resin grade should be confirmed during the design stage because different grades may have different shrinkage, flow, impact, and cooling behavior.
Q3: Can the bucket handle be integrated into the moulded product?
Yes. Handle integration can be included in the mould design. The handle attachment structure, grip shape, position, and reinforcement can be modified according to the customer’s product requirements.
Q4: Is the mould available with more than one cavity?
Yes. The standard configuration supports one or two cavities. The correct choice depends on product size, desired output, injection machine capacity, tooling budget, and production balance requirements.
Q5: What is the difference between the hot runner and cold runner options?
A hot runner keeps the plastic flow path heated and can reduce runner waste in high-volume production. A cold runner is generally simpler and may offer easier maintenance or lower initial complexity. The best option depends on the product, material, production volume, and customer equipment.
Q6: How does the mould help prevent basin or bucket deformation?
The mould focuses on balanced wall thickness, strong rim structures, and optimized cooling. These features help reduce uneven shrinkage and thermal stress, supporting better dimensional stability during and after moulding.
Q7: What surface finishes are available?
The mould can be supplied with a polished or matte surface finish. The preferred option should be selected according to the desired product appearance, cleaning requirements, and market positioning.
Q8: What steel can be used for the mould?
P20 and H13 are the listed steel options. P20 provides a practical solution for many general household applications, while H13 may be selected when greater resistance to demanding operating conditions is required.
Q9: What is the expected service life?
The stated mould life is approximately 700,000 shots. Actual service life depends on steel selection, resin, processing conditions, mould maintenance, production frequency, and the use of additives or abrasive materials.
Q10: Can the mould be made for a customer’s existing injection machine?
The mould should be designed around the customer’s machine specifications. Important information includes clamping force, injection volume, platen dimensions, tie-bar spacing, ejector arrangement, nozzle details, and available cooling connections.
Q11: What information should be supplied for a quotation?
Customers should provide product drawings or samples, dimensions, material, expected output, handle requirements, surface finish, cavity preference, machine specifications, and any special packaging or inspection requirements.
Q12: Does the supplier provide after-sales support?
Haiquan provides integrated services covering design, production, and after-sales support. Customers can discuss installation, operation, maintenance, spare parts, and technical questions with the supplier after delivery.
Conclusion
The Household Plastic Basin and Bucket Injection Mould is engineered for a product category that demands both simplicity in use and precision in manufacture. Strong rim structures, balanced wall thickness, customizable handle integration, smooth surfaces, and optimized cooling help address the principal challenges associated with large household plastic parts.
With P20 or H13 steel options, hot or cold runner configurations, one- or two-cavity layouts, and polished or matte surface finishes, the mould can be adapted to different production strategies. Its compatibility with PP and PE supports a wide range of household applications, from washing basins and cleaning buckets to bathroom containers and utility storage products.
Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. strengthens this product through professional design capability, precision manufacturing, scientific production management, international export experience, and after-sales service. By managing the process from design analysis through trial moulding and delivery, the company provides more than a basic cavity-and-core tool. It provides a production system intended to improve product consistency, reduce manufacturing risk, support long-term output, and create better value for household plastic product manufacturers.
References
1. Injection Moulding Design Principles for Thermoplastic Household Products.
2. General Guidelines for Plastic Part Wall Thickness, Draft Angles, Ribs, and Reinforcement.
3. Engineering Data and Processing Recommendations for Polypropylene and Polyethylene.
4. Tool Steel Selection Guide for Plastic Injection Mould Applications.
5. Industrial Practices for Injection Mould Cooling, Ejection, and Preventive Maintenance.
6. Product and technical information supplied for the Household Plastic Basin and Bucket Injection Mould.
Product: Household Plastic Basin and Bucket Injection Mould

For exclusive deals and latest offers, sign up by entering your email address below.











 +86-18657672567
 sales@tzhqmould.com
celin@tzhqmould.com
 No. 17 Houshi Road, Beicheng Industrial Zone, Huangyan District, Taizhou City, Zhejiang Province, China
Copyright © Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. All Rights Reserved
Injection Plastic Mould Maker

