

Plastic Flower Pot Injection Mould with Various Designs for Efficient Pot Manufacturing
Admin 2026-09-20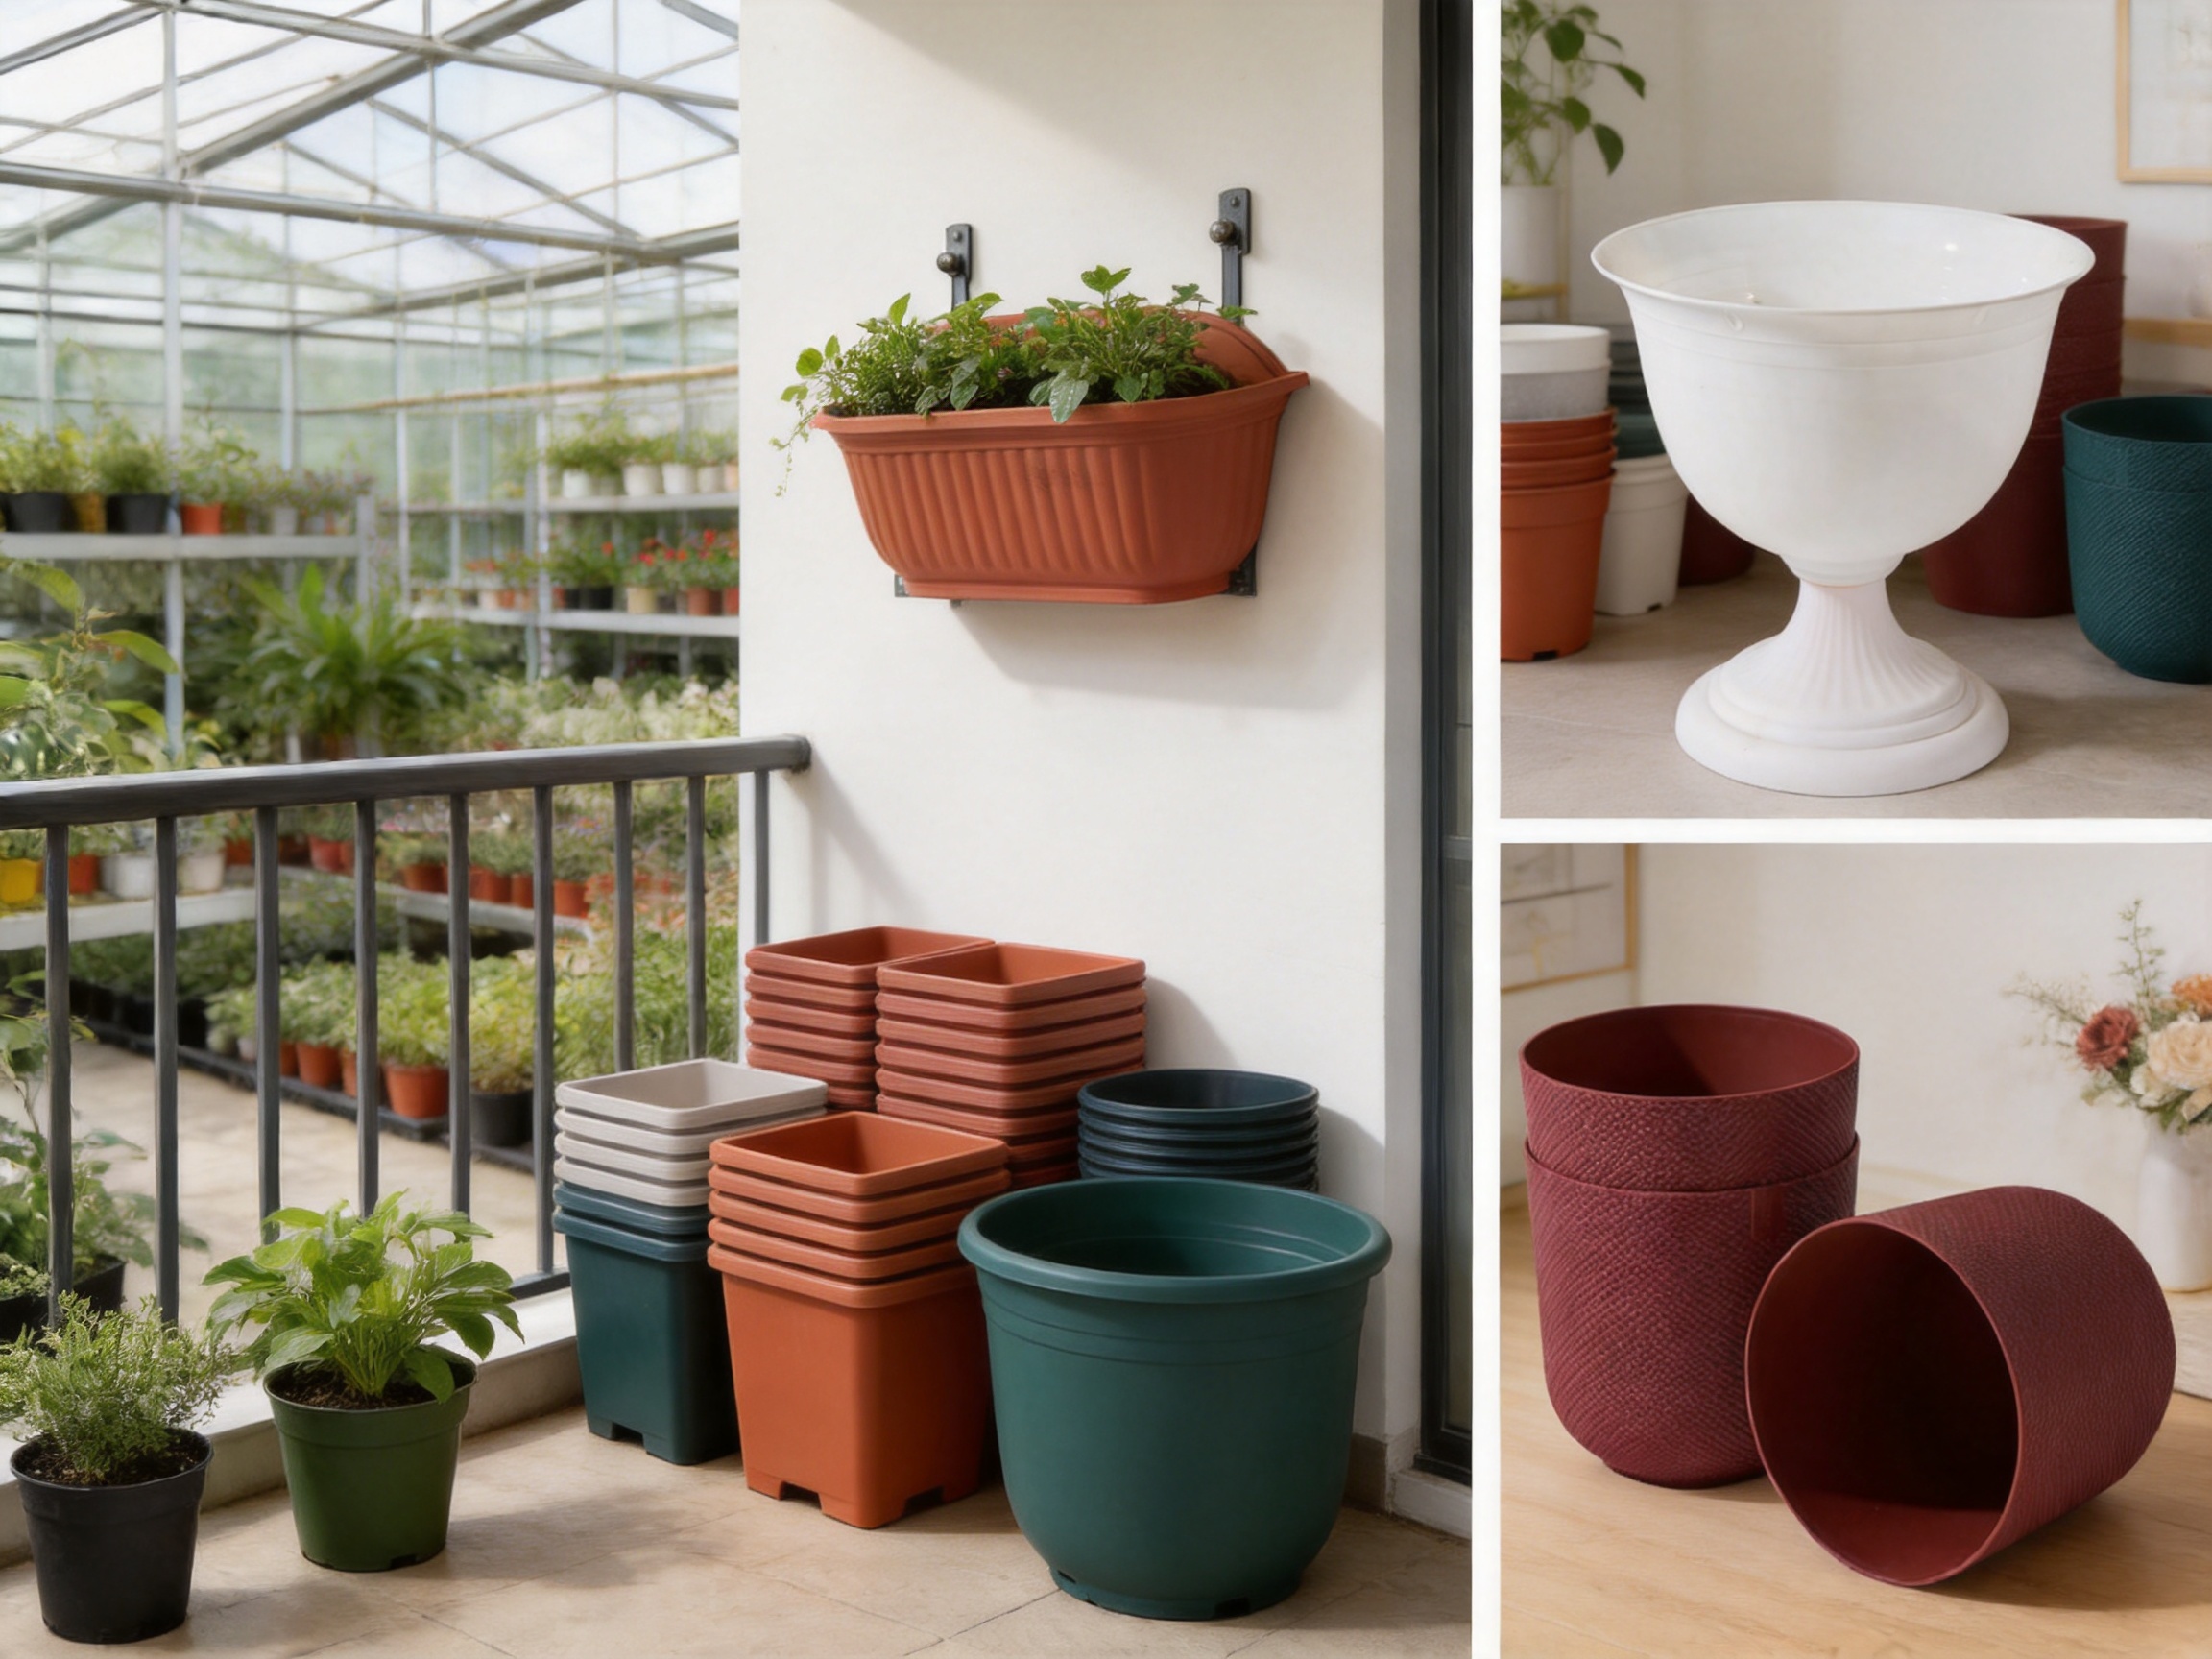
Plastic flower pots are essential products in gardening, landscaping, nursery production, home decoration, and commercial plant cultivation. Although they may appear simple, manufacturing high-quality pots requires carefully engineered tooling that can deliver attractive shapes, consistent wall thickness, reliable drainage, smooth surfaces, and stable production performance. The Plastic Flower Pot Injection Mould with Various Designs is developed to meet these requirements while supporting different pot styles, sizes, surface finishes, and production volumes.
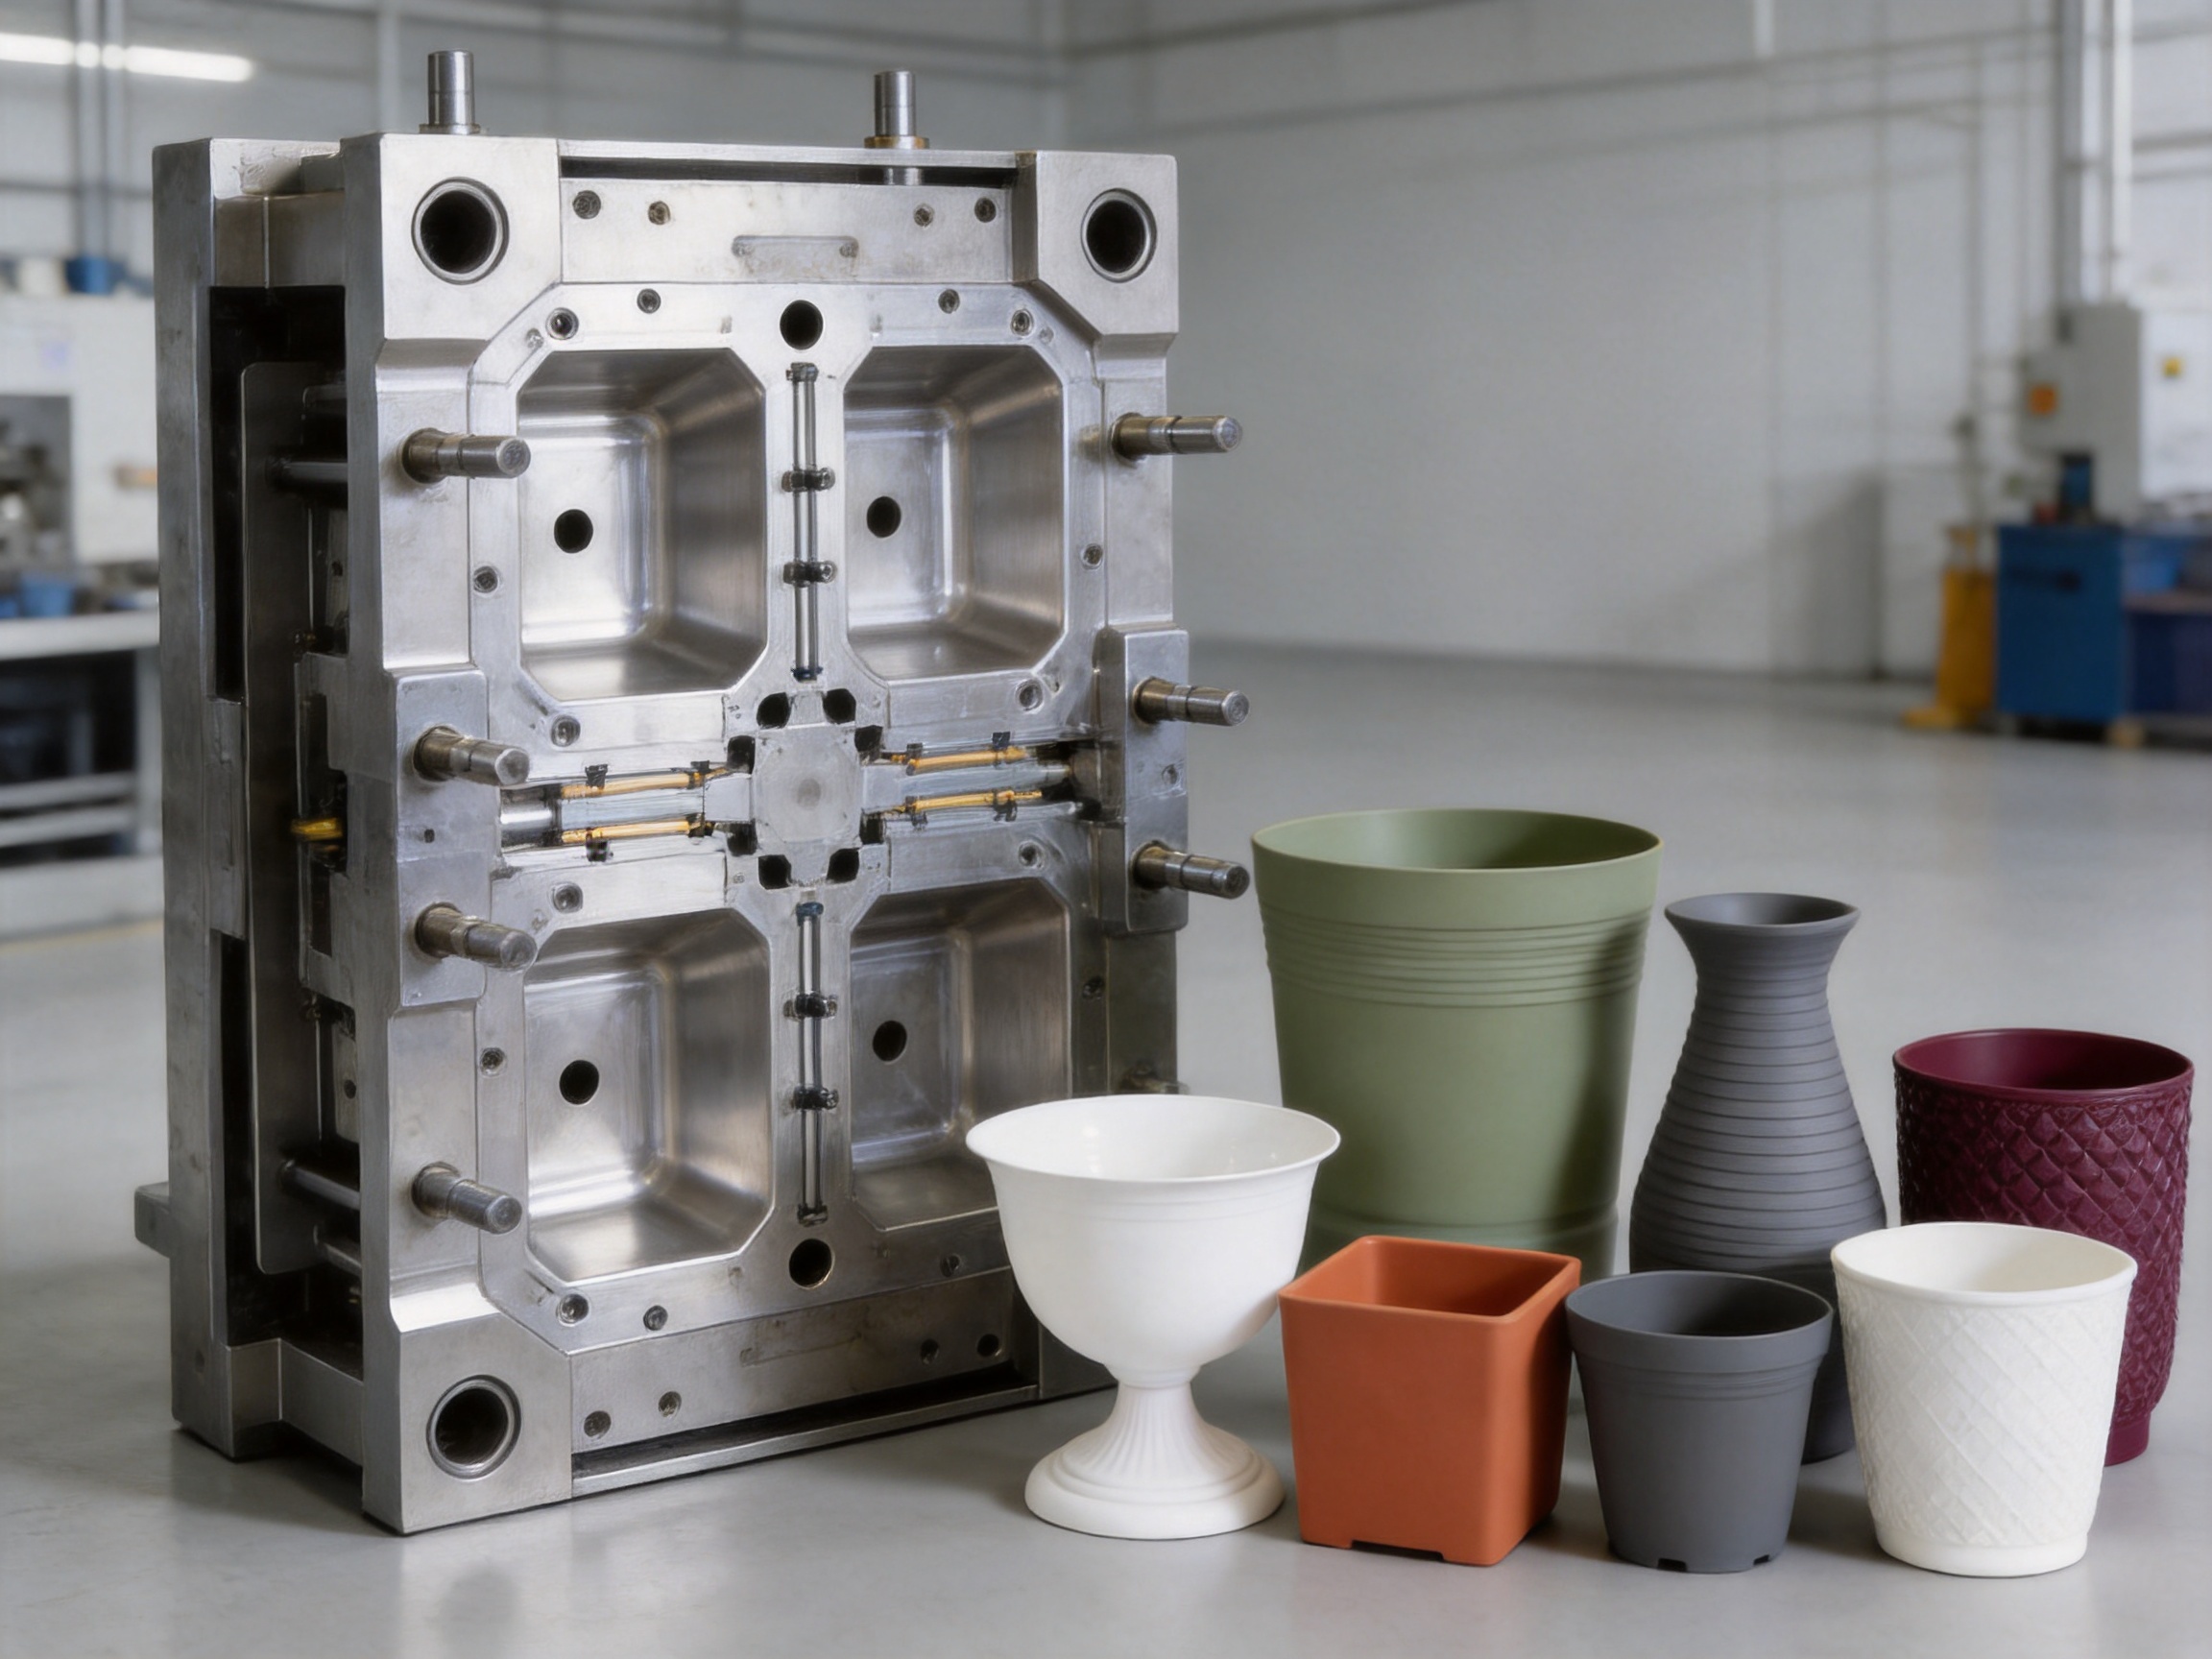
This injection mould is suitable for producing round flower pots, square plant containers, decorative planters, nursery pots, balcony containers, and other customized plastic planting products. Its design is centered on dimensional accuracy, efficient cooling, practical demoulding, and long-term mould durability. By combining suitable mould steel, optimized cavity layouts, flexible runner systems, polished surfaces, and integrated drainage-hole forming, the mould helps manufacturers produce pots that are attractive, functional, lightweight, and strong.
Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. manufactures precision injection moulds for daily necessities, home appliances, automotive components, and industrial equipment. With a professional design team, structured production management, and experience serving international customers, the company provides integrated support from product development and mould design to manufacturing, testing, delivery, and after-sales service.

Plastic Flower Pot Injection Mould with Various Designs
Overview of the Plastic Flower Pot Injection Mould
The Plastic Flower Pot Injection Mould is a reusable production tool used to transform molten thermoplastic material into finished flower pots and plant containers. During injection moulding, plastic pellets such as polypropylene, polyethylene, or recycled plastic are heated until they become fluid. The material is then injected into the mould cavity under controlled pressure. After filling, the material cools and solidifies before the mould opens and the finished pot is removed.
The mould can be configured for one to eight cavities, allowing manufacturers to select a production arrangement according to product demand, machine capacity, investment objectives, and required cycle time. A single-cavity mould may be suitable for customized products or smaller production runs, while a multi-cavity design can improve output for mass production.
Different flower pot designs require different moulding solutions. A basic round nursery pot may require a straightforward cavity structure, while a decorative planter may include tapered walls, embossed patterns, raised bands, curved edges, or special external textures. The tooling must account for these design elements without creating unnecessary difficulties during filling, cooling, or demoulding.
The mould is designed to support practical daily production. Its structure can include a cold runner or hot runner system, depending on the customer’s production requirements. The cooling layout is engineered to remove heat efficiently from the mould, helping shorten cycle time and improve dimensional stability. Drainage openings can also be formed directly during injection moulding, reducing the need for drilling or other secondary operations.
Product Features and Engineering Advantages
Support for Multiple Flower Pot Shapes
One of the primary advantages of this mould solution is its compatibility with multiple product shapes. Round pots remain popular because they are easy to arrange, simple to clean, and suitable for many plant varieties. Square and rectangular containers make efficient use of shelf, greenhouse, balcony, and transport space. Decorative shapes can be developed for retailers, garden centers, home decoration brands, and promotional product lines.
The mould can be designed around the customer’s required product geometry rather than forcing every application into a standard shape. This flexibility supports a broad range of pot styles, including conventional nursery pots, modern minimalist containers, textured planters, decorative balcony pots, and distinctive shapes created for retail differentiation.
Accurate replication of the product design is particularly important for pots with symmetrical patterns or interlocking arrangements. Small dimensional differences can affect how pots stack, how lids or saucers fit, and how products appear when displayed together. Precision mould construction helps maintain consistency across the production batch.
Consistent Wall Thickness
Flower pots need to balance strength and material efficiency. If the wall is too thin, the pot may deform during handling, transportation, filling, or outdoor use. If the wall is unnecessarily thick, material consumption and cooling time increase, which can reduce productivity and raise production costs.
The mould is engineered to help maintain consistent wall thickness throughout the product. Balanced cavity design, suitable gate positioning, controlled filling, and carefully considered cooling channels all contribute to reliable part formation. Consistent wall thickness also improves the appearance of the pot by reducing visible sink marks, uneven shrinkage, and distortion.
For nursery and commercial horticulture products, dimensional consistency is valuable because large quantities of pots are often stacked, transported, and filled using semi-automatic or automatic equipment. Uniform products reduce stacking problems and help maintain a stable production process.
Integrated Drainage Hole Forming
Effective drainage is essential for healthy plant growth. Flower pots commonly require one or more drainage openings at the bottom or around the lower sidewall. These openings allow excess water to escape and help reduce the risk of water accumulation around plant roots.
Drainage holes can be incorporated directly into the injection mould. This approach eliminates or reduces secondary drilling, punching, or cutting operations. Direct forming improves production efficiency and helps keep hole positions consistent from one pot to the next.
The drainage-hole system can be adapted to the product design. The customer may specify the number, shape, size, and location of the openings according to the intended plant type and use environment. For decorative products, the drainage pattern can also be designed to support the visual appearance of the pot.
Polished Internal Surfaces
The inside of a flower pot should be smooth enough to support easy demoulding and convenient plant removal. A high-quality polished surface can reduce friction between the mould and the finished product. This is especially important for tapered pots, deep containers, and products with relatively narrow openings.
Polished mould surfaces also improve the visual quality of the finished pot. A smooth interior is easier to clean and less likely to retain excessive soil or moisture. Depending on the product concept, the external surface may be polished, textured, or finished with a decorative pattern while the inner surface remains smooth for functional reasons.
Surface treatment is selected according to the customer’s requirements. A polished finish can create a clean, refined appearance. A textured finish can reduce the visibility of minor marks and provide a more natural or premium visual effect. Embossed or patterned surfaces can be used to create product differentiation without adding separate components.
Efficient Cooling Design
Cooling is one of the most important factors in injection moulding productivity. After the plastic fills the cavity, it must cool sufficiently before the mould opens and the product is ejected. Poor cooling may cause long cycles, warpage, uneven shrinkage, or dimensional instability.
The mould’s cooling channels are arranged to promote effective heat removal from critical areas of the pot. A balanced cooling system helps maintain more uniform mould temperatures, which supports stable product dimensions and a more predictable production cycle.
Efficient cooling can also improve overall equipment utilization. When cycle time is reduced without compromising product quality, the same injection moulding machine can produce more pieces during a working shift. For high-volume flower pot manufacturing, this productivity advantage can have a direct effect on production economics.
Material Compatibility
The Plastic Flower Pot Injection Mould supports commonly used materials including polypropylene, polyethylene, and recycled plastic. The final selection depends on the intended application, product performance requirements, appearance, environmental conditions, and customer sustainability objectives.
Polypropylene
Polypropylene is widely used for flower pots because it offers a useful combination of low weight, chemical resistance, flexibility, and processability. It can be molded into thin yet functional containers and is suitable for both simple nursery pots and more decorative designs.
PP can also support a broad color range and is compatible with many surface treatments. Its performance makes it appropriate for indoor plant containers, outdoor garden pots, seedling containers, and retail planters.
Polyethylene
Polyethylene is another suitable material for selected flower pot applications. It provides toughness and good impact resistance, which can be valuable when products are handled frequently or exposed to transportation stress. Depending on the grade, PE can be used for flexible or semi-rigid pot designs.
The moulding process must be adjusted to the selected polyethylene grade. Melt flow behavior, shrinkage, cooling requirements, and demoulding performance should be considered during mould design and trial production.
Recycled Plastic
Recycled plastic can help manufacturers reduce reliance on virgin raw materials and develop products with a stronger sustainability profile. The use of recycled material requires attention to material consistency, contamination control, color variation, and processing stability.
A properly engineered mould can support recycled plastic production when the material is prepared and processed appropriately. Mould design should provide reliable filling and adequate venting, while the production team should confirm that the selected recycled resin meets the required mechanical and visual standards.
| Item | Specification | Manufacturing Value |
| Mould Type | Plastic injection mould | Suitable for repeatable mass production |
| Mould Steel | P20, 718, or H13 | Selected according to service life and production requirements |
| Product Material | PP, PE, or recycled plastic | Supports common flower pot material options |
| Runner System | Cold runner or hot runner | Flexible production configuration |
| Cavity Quantity | 1–8 cavities | Adaptable to output requirements |
| Expected Mould Life | 500,000+ shots | Suitable for long-term production planning |
| Surface Finish | Polished, textured, or patterned | Supports different product appearances |
Mould Steel Selection and Service Life
Mould steel has a direct influence on durability, maintenance requirements, surface quality, and production stability. The Plastic Flower Pot Injection Mould can use P20, 718, or H13 steel according to the production application and customer expectations.
P20 Steel
P20 is frequently used for general-purpose injection moulds. It offers a practical balance between machinability, strength, surface performance, and cost. For standard flower pots and moderate production volumes, P20 can provide a cost-effective tooling solution.
With appropriate machining, polishing, assembly, and maintenance, P20 mould components can support stable production for a wide range of daily necessity products.
718 Steel
718 steel is suitable when improved mechanical performance and surface quality are required. It is often selected for products with more demanding appearance requirements, larger dimensions, or longer expected service intervals.
For decorative pots with polished or textured surfaces, the steel grade should be chosen together with the required finish. A suitable steel substrate supports better polishing performance and helps maintain the cavity surface during repeated production.
H13 Steel
H13 is a hot-work tool steel known for its strength and resistance to thermal fatigue. It can be considered for demanding moulding conditions, high production volumes, or applications requiring enhanced durability in certain mould components.
The appropriate steel choice depends on more than the product shape. Material selection should consider the number of production shots, resin characteristics, moulding temperature, cavity quantity, maintenance plan, and expected product life.
With a stated mould life of 500,000 or more shots, the tooling is intended to support long-term production planning. Actual service life depends on material selection, machine settings, operating conditions, cleaning procedures, preventive maintenance, and the handling of the mould during storage and installation.
Runner System Options
The mould can be designed with either a cold runner or a hot runner system. Each option has different benefits, and the best choice depends on product geometry, cavity quantity, material usage, production volume, and the customer’s equipment preferences.
Cold Runner System
A cold runner system is a practical option for many standard flower pot applications. It generally has a straightforward structure and can offer lower initial tooling complexity. The runner material may be recycled into the production process when the selected resin and product requirements allow it.
Cold runner moulds can be suitable for smaller production runs, standard product designs, and applications where the cost of hot runner components is not justified. The runner layout must still be carefully balanced to promote uniform cavity filling and consistent product quality.
Hot Runner System
A hot runner system can reduce or eliminate solidified runner waste and may improve production efficiency for high-volume or multi-cavity applications. It can also support more direct control of material flow and potentially reduce post-moulding trimming.
Hot runner tooling generally requires more detailed temperature control and maintenance. The design must account for heater systems, nozzle selection, thermal balance, material sensitivity, and service access. When properly configured, it can be a valuable solution for manufacturers seeking higher automation and reduced material waste.
Manufacturing Process at Haiquan Mould
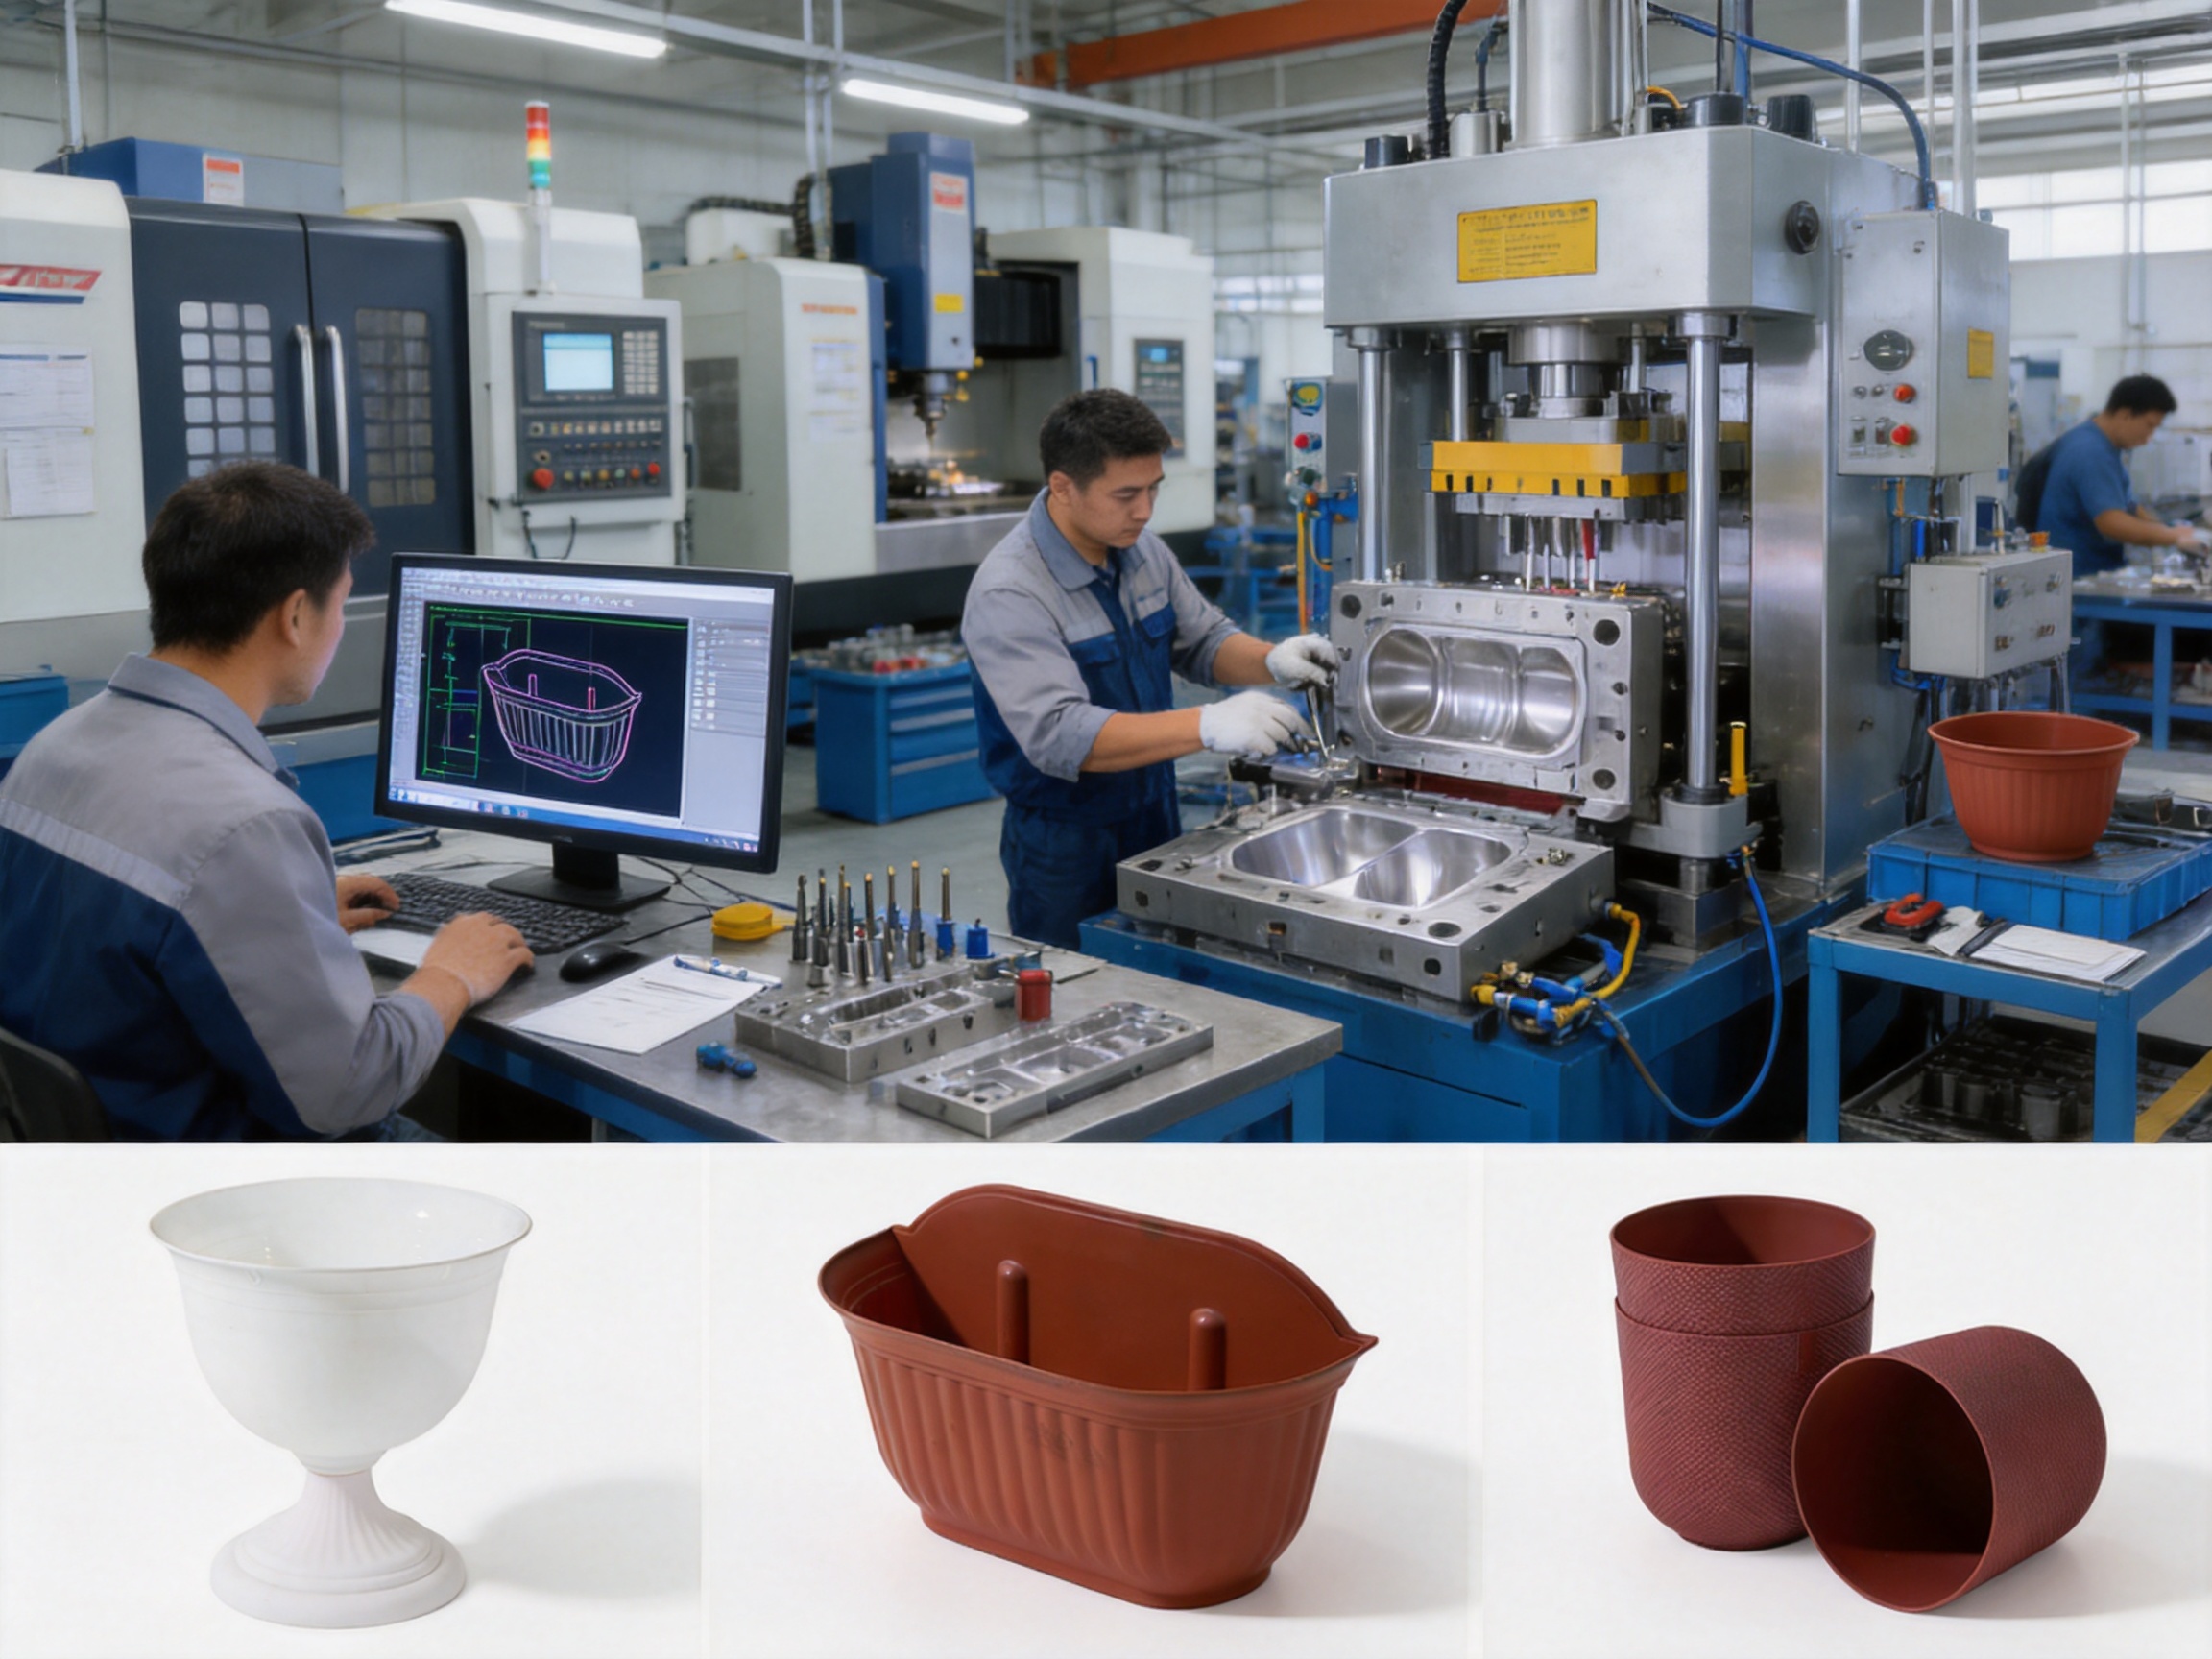
Advanced mould manufacturing is not limited to machining a cavity. It requires a coordinated process that begins with product analysis and continues through design, material selection, precision machining, assembly, testing, inspection, and after-sales support. Haiquan Mould applies a structured workflow to help convert customer requirements into functional injection tooling.
Product Requirement Review
The process begins with a review of the intended flower pot. Important information includes the product dimensions, shape, wall thickness, drainage-hole arrangement, surface finish, material, expected production quantity, machine specifications, and required delivery schedule.
This stage helps identify potential manufacturing risks before detailed design begins. For example, a decorative pattern may require a specific draft angle to support demoulding. A thin wall may require a carefully selected gate position. A deep pot may require special attention to cooling and ejection. Early analysis reduces the likelihood of costly modifications later.
3D Product and Mould Design
After the product requirements are confirmed, the mould design team develops the cavity, core, parting line, runner system, cooling layout, ejection system, and related components. Three-dimensional design allows the team to review the relationship between these elements before machining.
The parting line is positioned to support reliable mould opening and minimize visible marks on important product surfaces. Draft angles are incorporated to help the pot release from the core. The gate location is chosen to support balanced filling and reduce the risk of weld lines or incomplete filling.
For multi-cavity moulds, cavity arrangement and runner balance are particularly important. The cavities should fill as evenly as possible so that product weight, dimensions, and appearance remain consistent across the entire shot.
Steel Preparation and CNC Machining
After the design is approved, mould steel is prepared according to the selected grade and component requirements. CNC machining is used to create the cavity, core, inserts, mould plates, and other precision parts.
Complex decorative details may require multiple machining processes. Rough machining removes the majority of excess material, while semi-finishing and finishing operations improve dimensional accuracy and surface quality. The machining strategy is planned to reduce deformation and maintain the required geometry.
Precision EDM and Fine Detail Processing
Electrical discharge machining can be used for areas that are difficult to produce through conventional cutting. EDM is particularly useful for narrow slots, deep features, sharp internal details, and certain decorative patterns.
For products with textured or patterned surfaces, the mould cavity must reproduce the intended design accurately. Fine detail processing is coordinated with polishing and surface treatment so that the final pot achieves the required visual result.
Polishing and Surface Treatment
Polishing is performed according to the required product finish. Inner surfaces may be polished to assist demoulding, while outer surfaces can receive a polished, matte, textured, or patterned finish.
Surface treatment must be consistent across all cavities. Uneven polishing can lead to differences in gloss or texture between products. Careful finishing helps ensure that pots manufactured from different cavities have a uniform appearance.
Mould Assembly
During assembly, individual components are fitted together and checked for alignment, movement, clearance, and correct operation. The ejection system must move smoothly, and the core and cavity must close accurately without damaging the mould surfaces.
Cooling channels, runner components, guide systems, inserts, ejector pins, and other parts are inspected during assembly. Proper assembly is essential for maintaining stable production and reducing the risk of premature wear.
Trial Moulding and Optimization
Before delivery, the mould is tested through trial injection moulding. The trial process evaluates filling behavior, cooling performance, product appearance, dimensional accuracy, drainage-hole formation, ejection, and cycle operation.
Trial results may lead to adjustments in injection speed, holding pressure, cooling time, mould temperature, gate configuration, or ejection timing. If necessary, minor mould modifications are made to improve the final product.
Testing is especially valuable for decorative flower pots because surface patterns, thin sections, and complex contours can influence filling and shrinkage. A systematic trial process helps confirm that the mould is ready for the customer’s production environment.
Advantages Over Less Specialized Competitor Tooling
Many mould suppliers can manufacture a basic cavity, but a production-ready flower pot mould must address more than the general shape of the product. The advantages of this mould solution come from the combination of functional design, customization, production efficiency, and integrated manufacturing support.
Designed for Both Appearance and Function
Some low-cost moulds focus primarily on producing a basic container and may not provide sufficient attention to surface quality, drainage, demoulding, or wall-thickness consistency. The Plastic Flower Pot Injection Mould is designed to balance decorative appearance with practical horticultural performance.
Customers can select polished surfaces, textures, or patterns while maintaining a smooth and functional inner surface. This makes the mould suitable for products positioned as everyday nursery items as well as decorative consumer goods.
Greater Design Flexibility
Standardized tooling may limit a manufacturer to one fixed size or shape. This mould solution supports customization in pot dimensions, cavity quantity, surface pattern, and drainage-hole configuration. Such flexibility allows customers to develop product lines for different markets rather than relying only on generic products.
Customization also supports private-label and OEM production. A customer may request a specific diameter, height, rim design, taper, texture, or visual identity. The tooling can be developed around these requirements while considering the practical limitations of injection moulding.
Reduced Secondary Processing
When drainage holes are formed directly during moulding, separate drilling or punching may be reduced. This can lower labor requirements, reduce handling, and improve positional consistency. Fewer secondary operations also reduce the possibility of damaging finished pots after they leave the moulding machine.
Direct forming is particularly helpful for mass production, where even a small amount of manual processing can create significant labor and time costs over a large order quantity.
Improved Cycle Efficiency
An efficient cooling system and suitable runner configuration can help reduce cycle time. Although the final cycle depends on the machine, resin, product thickness, and processing settings, mould design has a major role in determining how quickly the pot can be cooled and ejected.
Higher output from each moulding machine can improve production efficiency and reduce the tooling cost allocated to each finished piece. This is an important advantage for manufacturers serving garden centers, nurseries, home improvement retailers, and large distribution networks.
Suitable for Different Production Scales
With one to eight cavities, the mould can be configured for different production requirements. A single-cavity arrangement may be appropriate for product development, seasonal demand, or premium customized pots. Multi-cavity arrangements are better suited to stable, high-volume production.
This range gives customers more control over their investment. Instead of selecting an oversized mould immediately, a manufacturer can choose a cavity quantity aligned with current demand and future expansion plans.
International Manufacturing Experience
Haiquan Mould serves customers in Europe, the Middle East, Southeast Asia, and South America. International experience requires attention to communication, technical documentation, quality expectations, packaging, delivery coordination, and after-sales support.
Customers working with an experienced export-oriented mould manufacturer can benefit from a more organized process when developing tooling across different time zones and production environments. Clear confirmation of drawings, materials, mould specifications, trial samples, and acceptance criteria helps reduce misunderstandings.
Applications of the Finished Flower Pots
Indoor Plant Pots
Indoor flower pots are used in homes, offices, hotels, restaurants, and commercial interiors. These products often emphasize appearance, surface quality, color consistency, and compatibility with decorative interiors.
Polished or patterned surfaces can help create a more attractive product, while integrated drainage systems support healthy plant care. Different sizes allow the same product family to accommodate small desk plants, medium decorative plants, and larger indoor greenery.
Outdoor Garden Containers
Outdoor pots must tolerate regular handling and exposure to changing environmental conditions. Strength, impact resistance, drainage, and stable dimensions are important considerations.
Plastic containers offer the advantage of lower weight compared with many ceramic or concrete alternatives. This makes them easier to move, arrange, and transport. The mould can support practical shapes that combine light weight with sufficient structural performance.
Nursery Planting Pots
Nurseries require large quantities of reliable, economical containers. Pots must stack efficiently, withstand filling and transportation, and provide suitable drainage for plant cultivation.
Multi-cavity tooling can support high output, while consistent wall thickness helps reduce product variation. For nurseries, the ability to produce pots in different sizes is also valuable because plants are often transferred into larger containers as they grow.
Decorative Balcony Planters
Balcony planters often need a balance between decorative appearance and practical installation. They may feature special shapes, textured surfaces, compact dimensions, or drainage arrangements designed for limited outdoor spaces.
The mould can be adapted for customized designs, allowing manufacturers to develop products that match contemporary home decoration trends. Surface patterns and molded details can add visual value without requiring separate decorative components.
Retail and Private-Label Products
Retailers and garden product brands may require flower pots with distinctive sizes, colors, textures, or package-oriented designs. A customized injection mould helps these customers create a product that is less interchangeable with generic market offerings.
OEM production can include adjustments to dimensions, cavity numbers, drainage patterns, and surface treatment. The result is a tooling solution aligned with the customer’s brand portfolio and sales strategy.
Customization Options
Customization is an important part of modern plastic product development. The basic mould structure can be adapted according to the customer’s product drawings, technical specifications, and market objectives.
Pot Size and Geometry
Pot diameter, height, taper, rim thickness, base shape, and overall capacity can be adjusted during the design stage. These dimensions should be evaluated together because changing one feature may affect mould opening, material flow, cooling, and ejection.
The customer may provide a finished product drawing, a three-dimensional model, a physical sample, or a general concept. The design team can then assess feasibility and prepare a mould proposal.
Cavity Quantity
Cavity quantity affects output, mould size, runner balance, machine requirements, and investment. One to eight cavities are available as a general configuration range. The final selection should reflect the expected order volume and the injection machine’s available shot capacity.
Surface Texture and Pattern
Surface texture can be used to create a matte appearance, natural material effect, anti-slip feel, or decorative pattern. Patterns can be developed on the outer surface while the inner surface remains smooth for easier product release.
The texture depth, draft angle, and feature arrangement must be carefully reviewed. Complex textures may increase tooling requirements and require additional attention during polishing, EDM, or surface treatment.
Drainage Design
Drainage holes can be customized according to pot size and intended use. Options may include a central hole, multiple small openings, radial patterns, side drainage, or a combination of these arrangements.
The design should provide sufficient water discharge while preserving base strength. The drainage system can also be integrated with the product’s appearance so that functional openings do not detract from the decorative design.
Runner Selection
Customers can discuss whether a cold runner or hot runner system is more suitable. The decision may depend on material cost, production quantity, automation level, acceptable runner waste, and maintenance preferences.
Quality Control and Inspection
Quality control is applied throughout the mould manufacturing process rather than only at the final stage. Material certificates, machining accuracy, component dimensions, assembly quality, surface finish, and trial samples all contribute to the final result.
Dimensional inspection verifies critical mould components and confirms that the cavity and core match the approved design. Alignment checks help ensure that the mould closes evenly. Cooling and runner systems are reviewed for correct connection and operation.
During trial moulding, finished samples are evaluated for weight, dimensions, wall thickness, drainage-hole position, surface appearance, flash, short shots, warpage, sink marks, and ejection marks. If the customer has special acceptance standards, these can be included in the inspection process.
Consistent quality is particularly important for multi-cavity moulds. Each cavity should produce parts with comparable dimensions and appearance. Cavity identification and sample tracking can help the production team analyze any differences during testing.
Production and Maintenance Recommendations
Proper operation and maintenance help preserve mould performance over its service life. Before production, the operator should confirm that the mould is correctly installed, the cooling circuit is functioning, and the injection machine settings are appropriate for the selected material.
After production, the mould should be cleaned to remove residual plastic, moisture, and contaminants. Drainage-hole cores, ejector components, parting surfaces, and vent areas deserve particular attention because contamination in these areas may affect product quality or mould movement.
Lubrication should be applied to suitable moving components according to the maintenance schedule. Excess lubricant should not be allowed to contaminate the cavity surface. The mould should be stored in a dry environment with appropriate corrosion protection when it is not in use.
Operators should avoid using hard tools that could scratch polished surfaces or damage textured features. Any unusual noise, difficult ejection, leakage, flash, or sudden dimensional change should be investigated promptly rather than ignored.
Preventive maintenance can include inspection of guide pins, bushings, ejector pins, cooling connectors, seals, hot runner components, cavity inserts, and fastening elements. Timely replacement of wear parts can reduce the risk of unexpected production stoppages.
Why Choose an Integrated Mould Manufacturing Partner?
Working with an integrated mould manufacturer can simplify communication and reduce coordination between separate design, machining, assembly, and testing suppliers. Haiquan Mould provides support across the complete tooling process, including product analysis, mould design, manufacturing, trial production, delivery, and after-sales service.
This integrated approach is valuable when the product includes several interacting requirements. A drainage system, decorative texture, multi-cavity layout, and short cycle time must be considered together. If each feature is designed independently, conflicts may arise during production. A unified technical team can evaluate the entire system more efficiently.
The company’s focus on daily necessity moulds gives it experience with products that require dependable cycle performance, practical material use, good appearance, and cost-conscious construction. Flower pots are part of a broader category of household and gardening products in which usability and volume production are equally important.
Its broader capabilities in home appliance, automotive, and industrial equipment moulds also support an engineering culture based on accuracy, process control, and structured production management. Although flower pots are daily-use products, their moulds still benefit from professional tooling standards.
Commercial Value for Flower Pot Manufacturers
The value of an injection mould should be assessed not only by its purchase price but also by its influence on production efficiency, material consumption, product consistency, labor requirements, and service life.
A mould that supports reliable cycle times can increase daily output. A mould that forms drainage holes directly can reduce secondary labor. A mould that maintains consistent wall thickness can lower rejection rates. A mould with durable steel and replaceable components can extend production continuity.
Design flexibility also creates commercial value. Manufacturers can develop several products from related design concepts, target different customer groups, and update surface patterns or dimensions as market demand changes. Customized pots can provide stronger differentiation than basic, widely available containers.
For international buyers, reliable delivery and technical support are also important. A mould is a long-term production asset, and the customer may need assistance with installation, trial adjustment, spare parts, or maintenance questions after delivery. An experienced supplier can contribute to a smoother transition from tooling development to regular manufacturing.
Frequently Asked Questions
What products can be manufactured with this mould?
The mould can manufacture plastic flower pots, indoor plant containers, outdoor garden pots, nursery pots, decorative planters, balcony containers, and related planting products. The final product range depends on the approved mould design.
Which materials are suitable for the flower pot mould?
Commonly supported materials include polypropylene, polyethylene, and recycled plastic. The material grade should be confirmed during the design and trial stage because melt flow, shrinkage, cooling, and demoulding behavior can vary.
Can the mould produce pots with drainage holes?
Yes. Drainage-hole forming systems can be integrated into the mould. The number, size, shape, and position of the holes can be discussed according to the intended product application.
How many cavities can the mould have?
The general cavity range is one to eight cavities. The suitable quantity depends on production volume, product size, injection machine capacity, cycle requirements, and investment objectives.
What mould steel options are available?
The available steel options include P20, 718, and H13. The best choice depends on the expected production quantity, surface finish, material, moulding conditions, and desired service life.
Can the flower pot have a customized surface texture?
Yes. The outer surface can be polished, textured, or patterned. Surface features should be designed together with suitable draft angles and demoulding considerations.
Can the mould support both round and square flower pots?
A mould is normally designed for a specific product or closely related product family. Round, square, and decorative shapes can all be developed, but each shape generally requires its own cavity and core configuration unless a specialized interchangeable insert system is planned.
What is the expected mould life?
The stated expected service life is 500,000 or more shots under suitable operating and maintenance conditions. Actual life may vary according to steel selection, material, machine settings, production frequency, cleaning, and preventive maintenance.
Should a cold runner or hot runner be selected?
A cold runner can be a practical and economical option for many standard applications. A hot runner may be advantageous for high-volume production, reduced runner waste, or more advanced automation. The choice should be made after reviewing the product and production plan.
How does the mould help reduce production costs?
Consistent wall thickness can help control material usage, integrated drainage holes can reduce secondary processing, and efficient cooling can shorten cycles. Multi-cavity configurations can also increase output per machine cycle.
Can the mould be used for OEM or private-label products?
Yes. The mould can be customized for OEM requirements, including dimensions, cavity quantity, drainage design, surface pattern, and other product features. Customers should provide technical drawings or product specifications for evaluation.
What information should be provided when requesting a quotation?
Useful information includes the product drawing or sample, material, product dimensions, estimated production quantity, desired cavity number, surface finish, drainage-hole requirements, injection machine information, runner preference, and target delivery schedule.
How is the mould tested before shipment?
The mould is assembled and tested through trial injection moulding. The trial evaluates filling, cooling, ejection, product dimensions, surface appearance, drainage-hole formation, and overall mould operation. Adjustments can be made when necessary.
Where is the manufacturer located?
Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. is located at No. 17 Houshi Road, Beicheng Industrial Zone, Huangyan District, Taizhou City, Zhejiang Province, China.
How can potential customers request technical information?
Customers can contact the company’s sales team by telephone at +86-18657672567 or by email at sales@tzhqmould.com. Technical details should be confirmed before the mould project begins.
Conclusion
The Plastic Flower Pot Injection Mould with Various Designs is a flexible tooling solution for manufacturers producing indoor pots, outdoor garden containers, nursery products, balcony planters, and customized decorative flower pots. Its main advantages include support for different shapes, consistent wall thickness, integrated drainage-hole forming, polished internal surfaces, efficient cooling, flexible cavity quantities, and compatibility with PP, PE, and recycled plastic.
The mould can be manufactured with P20, 718, or H13 steel and configured with either a cold runner or hot runner system. With one to eight cavities and an expected service life of 500,000 or more shots, it can be adapted to different levels of production demand.
Compared with basic tooling that focuses only on producing a container shape, this solution places greater emphasis on complete production performance. The design considers appearance, drainage, demoulding, cooling, material efficiency, product consistency, and long-term operation. Customization options allow manufacturers to develop products with distinctive dimensions, patterns, textures, and market positioning.
Supported by professional mould design, precision machining, structured assembly, trial production, quality inspection, and international service experience, Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. provides an integrated approach to flower pot mould manufacturing. For gardening product manufacturers, nursery suppliers, household brands, and OEM customers, the mould offers a practical foundation for stable, efficient, and commercially competitive plastic pot production.
References
1. Injection Molding Handbook, general principles of thermoplastic injection mould design and production.
2. Plastics Materials and Processing, reference information on polypropylene, polyethylene, recycled polymers, shrinkage, and processing behavior.
3. Tool and Manufacturing Engineers Handbook, guidance on mould materials, precision machining, cooling, ejection, and maintenance.
4. General technical principles for plastic injection mould cavity design, runner balancing, drainage-hole forming, and surface finishing.
5. Product and company information supplied for the Plastic Flower Pot Injection Mould with Various Designs.
Product: Plastic Flower Pot Injection Mould with Various Designs

For exclusive deals and latest offers, sign up by entering your email address below.












 +86-18657672567
 sales@tzhqmould.com
celin@tzhqmould.com
 No. 17 Houshi Road, Beicheng Industrial Zone, Huangyan District, Taizhou City, Zhejiang Province, China
Copyright © Taizhou Huangyan Haiquan Plastic Mold Co., Ltd. All Rights Reserved
Injection Plastic Mould Maker

